Automatic powder feeding and conveying equipment, as a core component in modern industrial production lines, plays a crucial role in the efficient and stable transportation of bulk powders. This equipment integrates advanced control technology and mechanical design, enabling automated feeding, conveying, and distribution of powders. The following content will delve into the principle of operation and the key characteristics of working scenarios for such equipment, with a focus on the products provided by Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field.
About Shandong HeadPowder Engineering Co., Ltd.
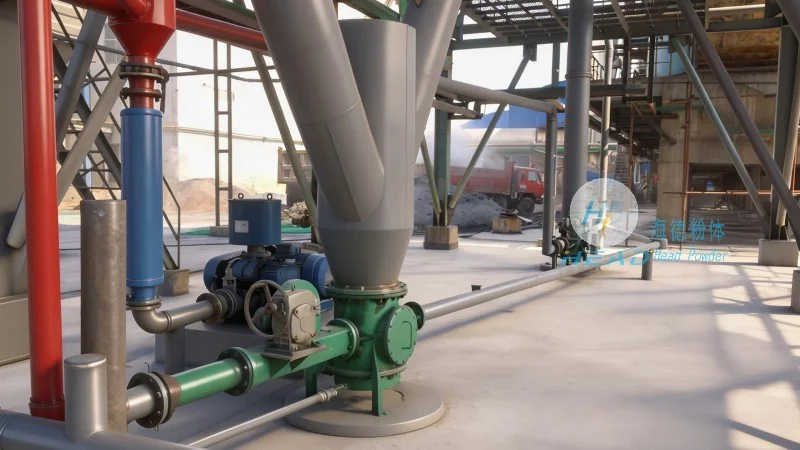
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer and supplier of powder processing equipment. The company is headquartered in Shandong, China, and has been committed to the research, development, and production of high-quality powder handling solutions for many years. HeadPowder's products are widely used in various industries, including chemical, pharmaceutical, food, and more, and are recognized for their reliability, efficiency, and advanced technology.
Principle of Automatic Powder Feeding Conveying Equipment
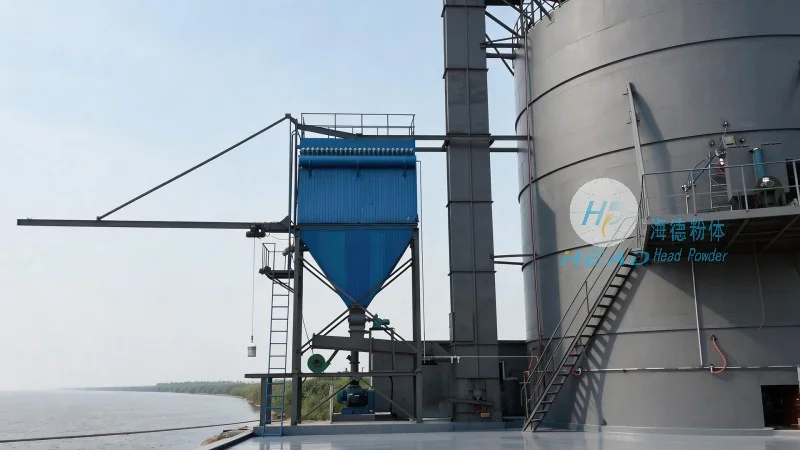
The automatic powder feeding and conveying system typically consists of several key components, including a feeding hopper, a conveyor mechanism (such as a screw conveyor, pneumatic conveyor, or belt conveyor), a control system, and sensors. The feeding hopper is used to store the powder material, and the conveyor mechanism is responsible for transporting the powder from the hopper to the target location. The control system, often equipped with PLC (Programmable Logic Controller) technology, monitors and adjusts the feeding and conveying process in real-time. Sensors, such as level sensors and flow sensors, provide feedback on the material level and flow rate, ensuring the system operates within the set parameters. The entire process is automated, reducing the need for manual intervention and improving production efficiency.
Working Scene Characteristics
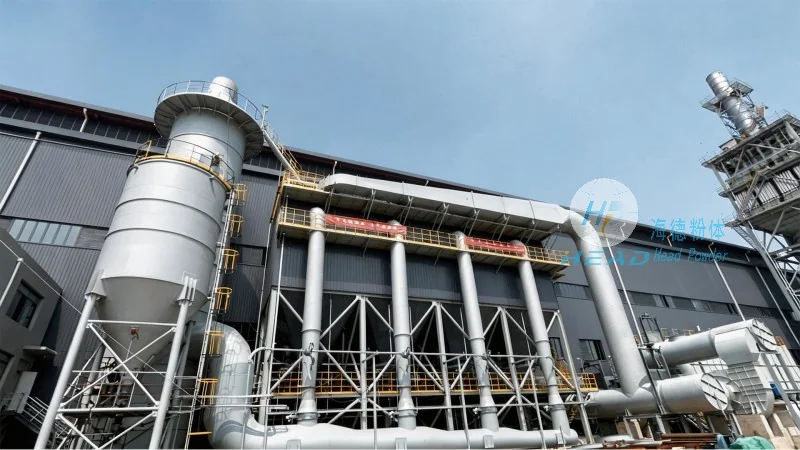
The working scene characteristics of automatic powder feeding conveyors are diverse and closely related to the specific application environments. In chemical production lines, for example, these equipment are used to transport raw materials like powders and additives, ensuring the smooth progress of the chemical synthesis process. In pharmaceutical manufacturing, the equipment must meet strict hygiene and safety standards, with features such as dust-proof design and easy cleaning. In the food industry, the equipment is designed to handle food-grade powders, with materials that comply with food safety regulations and no contamination risk. The working scene also includes different production scales, from small-scale laboratory use to large-scale industrial production, and the equipment can be customized according to the specific needs of the production line.
Advantages in Different Industries
Automatic powder feeding conveyors bring significant advantages to various industries. In the chemical industry, they improve the safety of handling hazardous powders by reducing human exposure and minimizing the risk of dust explosions. In the pharmaceutical industry, they enhance the accuracy of dosage and ensure the purity of the final product. In the food industry, they maintain the quality and freshness of food powders, meeting the high standards of food safety. Additionally, the automation of the feeding and conveying process reduces labor costs and increases production capacity, making it an essential part of modern industrial production.




