Lightweight aggregate powder conveying equipment is a specialized system designed to transport lightweight aggregate powders efficiently and reliably. This equipment is crucial in various industrial applications where the handling of lightweight aggregates, such as expanded clay, vermiculite, or other lightweight construction materials, is required. The core principle behind these systems involves the use of advanced mechanisms to move bulk powders through pipelines or other conduits, ensuring minimal dust generation and optimal material flow control.
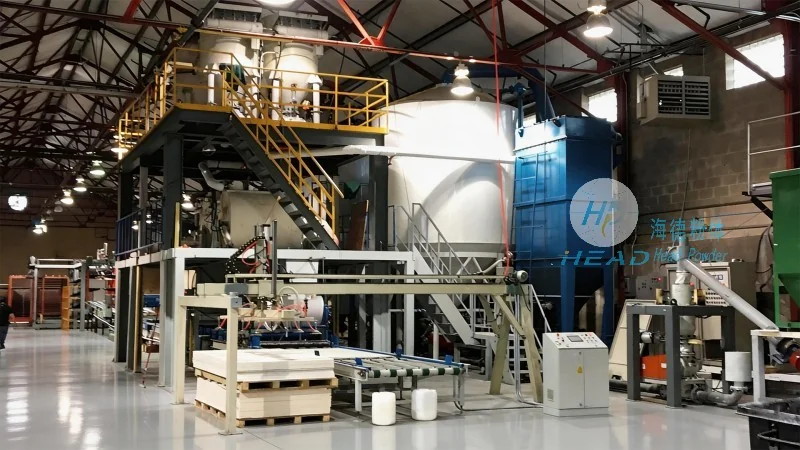
Working Principle of Lightweight Aggregate Powder Conveying Equipment
The operation of lightweight aggregate powder conveying equipment is based on several key principles that ensure effective material transport. One common method is the use of positive displacement pumps or screw conveyors, which create a pressure differential to move the powder. Another approach involves pneumatic conveying systems, where compressed air or other gases are used to push the powder through a network of pipes. These systems often incorporate features like airlocks, rotary valves, and dust collection units to maintain a clean and efficient operation. The equipment is engineered to handle the unique properties of lightweight aggregates, which can be light, dusty, and prone to segregation, ensuring that the conveying process is smooth and consistent.
Key Components and Their Functions
Lightweight aggregate powder conveying equipment typically consists of several essential components that work in tandem to achieve efficient material transport. The main components include the hopper or feed hopper, which stores and feeds the lightweight aggregate powder into the system. The conveyor itself, whether it's a screw conveyor, pneumatic line, or other type of transport mechanism, is responsible for moving the powder through the system. Airlocks and rotary valves are critical for controlling the flow and preventing backflow, ensuring that the material moves in a single direction. Dust collection systems, such as cyclones or bag filters, are often integrated to capture and remove dust particles, maintaining a clean working environment. Additionally, control panels and sensors are used to monitor the system's performance, allowing for real-time adjustments and maintenance.
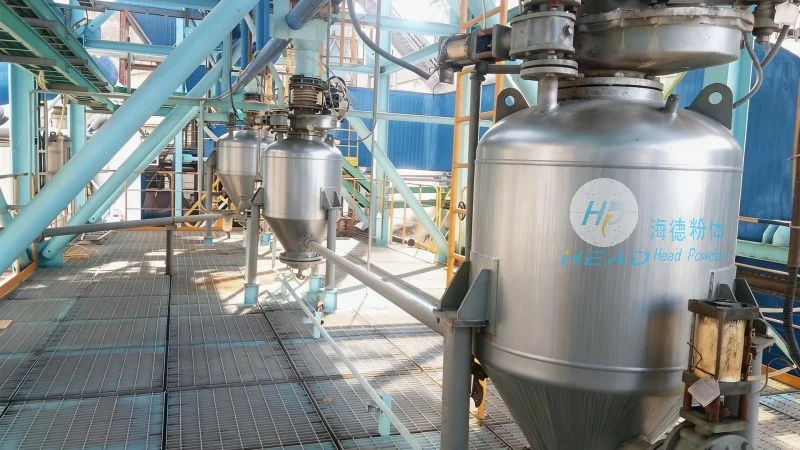
Working Scene Characteristics and Applications
The working scene characteristics of lightweight aggregate powder conveying equipment are tailored to meet the demands of specific industrial environments. These systems are commonly used in construction material manufacturing, where lightweight aggregates are processed and packaged for use in building materials. They are also utilized in agricultural applications, such as the handling of lightweight soil amendments or fertilizers. In the chemical industry, these conveyors may be used to transport lightweight powders for various processing steps. The equipment is designed to operate in environments where dust control is essential, and it can be integrated into existing production lines to enhance efficiency and reduce labor costs. The working characteristics include high capacity, low maintenance requirements, and the ability to handle a wide range of particle sizes and moisture contents, making it suitable for diverse industrial needs.
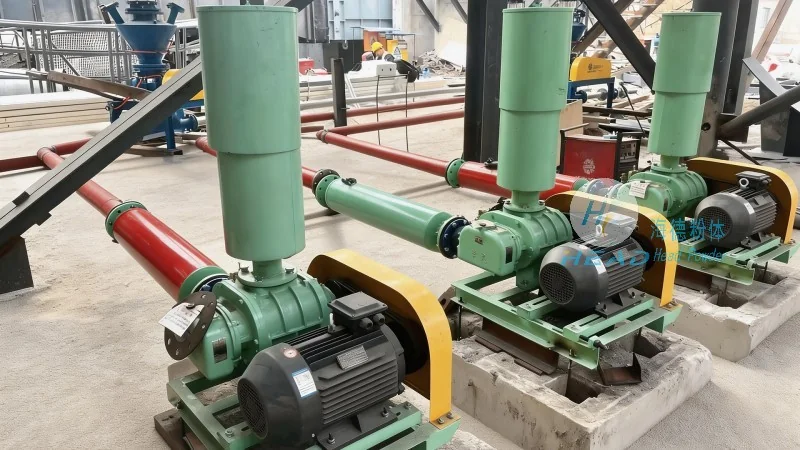
Advantages and Benefits of Using Lightweight Aggregate Powder Conveying Equipment
Implementing lightweight aggregate powder conveying equipment offers several advantages for industrial operations. One of the primary benefits is the reduction in labor costs, as automated systems can handle large volumes of material with minimal human intervention. The equipment also minimizes material loss and contamination, as it is designed to prevent dust and segregation during transport. Additionally, these systems improve safety by reducing the need for manual handling of powders, which can be hazardous. The efficiency of the conveying process leads to increased production rates and better overall productivity. Furthermore, the equipment can be customized to meet specific operational requirements, allowing for flexibility in different industrial settings. The use of advanced materials and engineering in the construction of these conveyors ensures durability and long-term performance, reducing the need for frequent repairs and replacements.
Conclusion and Company Overview
Lightweight aggregate powder conveying equipment is a vital component in industries that rely on the efficient handling of lightweight construction materials. The principles and working characteristics of these systems are designed to address the unique challenges of transporting such powders, ensuring optimal performance and minimal environmental impact. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality conveying solutions tailored to the needs of various industrial applications. With a focus on innovation and customer satisfaction, the company offers reliable equipment that enhances operational efficiency and safety. Based in Shandong, China, HeadPowder has established itself as a trusted partner for businesses seeking advanced powder handling solutions. The company's commitment to quality and customer service ensures that clients receive equipment that meets their specific requirements and contributes to their overall success in the market.




