HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for rice husk powder handling. This article explores the fundamental principles behind these systems and highlights the key working scene characteristics that make them indispensable in modern processing industries.
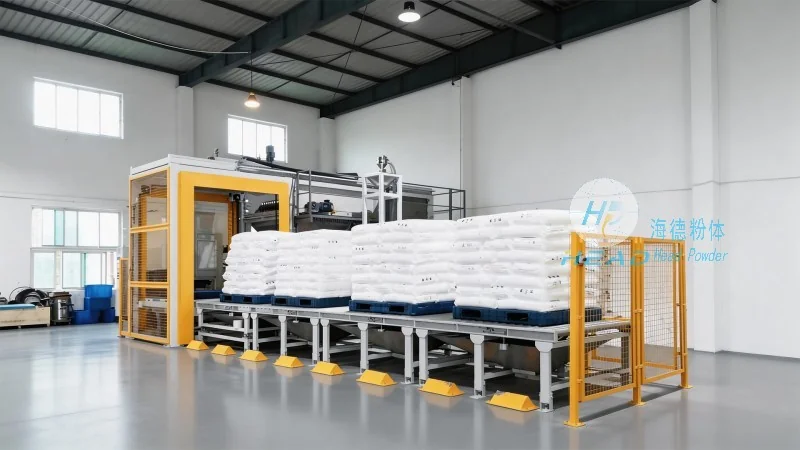
Understanding the Pneumatic Conveying Principle
The core of a rice husk powder pneumatic conveying system lies in the use of air as the primary medium to transport bulk materials. Unlike traditional mechanical conveyors, which rely on belts or screws, pneumatic systems utilize compressed air to create a flow that carries the powder from the source to the destination. This method offers several advantages, including the ability to transport materials over long distances, navigate complex layouts, and maintain a high degree of cleanliness and containment. The system typically consists of a hopper for material storage, a blower or compressor to generate the air flow, a pipeline network to guide the material, and a receiver or discharge point where the material is deposited. The operation involves feeding the rice husk powder into the hopper, activating the air system, and allowing the air pressure to lift and transport the powder through the pipeline. The speed and efficiency of this process are influenced by factors such as the air pressure, material properties (like particle size and moisture content), and the design of the pipeline and equipment.
Key Working Scene Characteristics
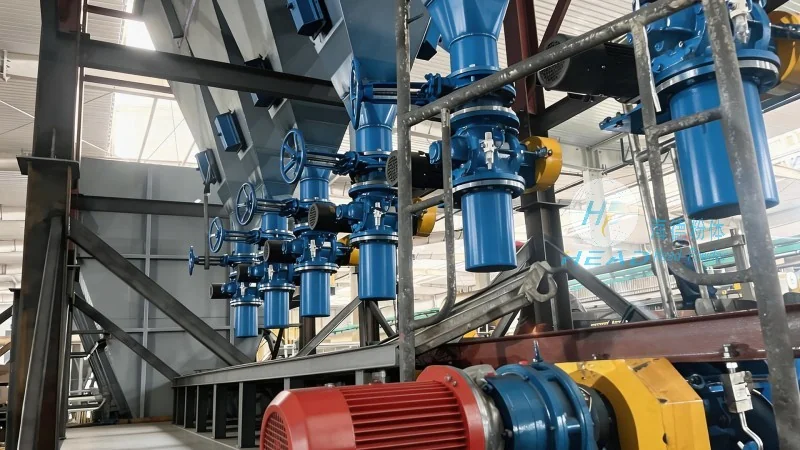
The working scene characteristics of rice husk powder pneumatic conveying equipment are tailored to meet the specific demands of various industrial applications. These characteristics include high efficiency in material transfer, minimal product contamination due to enclosed systems, and the ability to handle materials with varying particle sizes and moisture levels. In addition, the systems are designed for easy integration into existing production lines, allowing for seamless operation without disrupting workflow. The flexibility of pneumatic conveying also enables the equipment to adapt to different operational needs, such as varying production volumes or changes in material characteristics. Another notable characteristic is the reduced need for manual handling, which enhances safety and operational efficiency in the workplace. The systems are also built to withstand the abrasive nature of rice husk powder, ensuring long-term durability and reliability. These features make the equipment suitable for a wide range of applications, from processing facilities to storage and distribution centers.
Applications and Industry Impact
Rice husk powder pneumatic conveying systems are widely used in industries where the efficient and clean transfer of bulk materials is critical. These applications include biomass power generation, where rice husk is used as a fuel source, and the production of biofuels and other renewable energy products. In the agricultural sector, the systems are employed in processing facilities to transport rice husk from storage to processing equipment. The equipment is also utilized in the manufacturing of composite materials, where rice husk powder is mixed with other components to create lightweight and durable products. The consistent and reliable performance of these systems ensures that production processes run smoothly, minimizing downtime and maximizing output. The use of pneumatic conveying in these applications not only improves operational efficiency but also contributes to a more sustainable and environmentally friendly approach to material handling.
Advantages Over Traditional Conveying Methods
Compared to traditional mechanical conveyors, rice husk powder pneumatic conveying systems offer several distinct advantages. The most significant benefit is the ability to handle materials with high moisture content or fine particle sizes without clogging or degradation. Mechanical systems often struggle with such materials, leading to reduced efficiency and increased maintenance costs. Pneumatic systems, on the other hand, maintain consistent performance even with challenging material properties. Another advantage is the reduced risk of product contamination, as the enclosed pipeline system prevents exposure to external elements. This is particularly important for food and pharmaceutical industries where product purity is paramount. The systems also provide better control over the material flow rate, allowing for precise dosing and processing. Additionally, pneumatic conveying can be more cost-effective in the long run, as it reduces the need for frequent maintenance and replacement of parts. The initial investment may be higher, but the operational savings and increased efficiency make it a viable option for many businesses.
Customization and Scalability
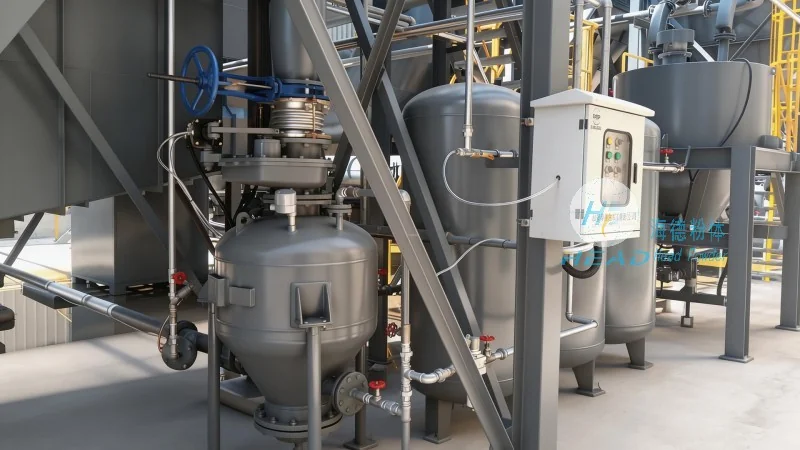
HeadPowder understands that each industrial application has unique requirements, which is why they offer customized pneumatic conveying solutions tailored to specific needs. The company’s engineers work closely with clients to design systems that meet their exact specifications, whether it's for small-scale operations or large-scale production facilities. The systems can be scaled to accommodate varying production volumes, from low to high throughput, ensuring that the equipment remains efficient and effective. Customization options include different pipeline materials, such as stainless steel or plastic, to suit the material's chemical properties and handling requirements. The blower or compressor can also be adjusted to provide the appropriate air pressure and flow rate. This flexibility allows businesses to optimize their material handling processes and achieve their operational goals. The company's commitment to customization ensures that clients receive a solution that is not only efficient but also durable and reliable, supporting long-term business success.
Maintenance and Reliability
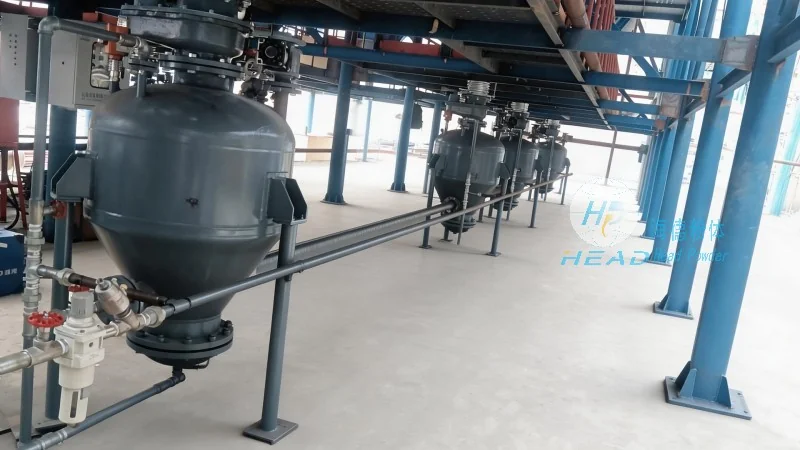
Ensuring the long-term performance and reliability of rice husk powder pneumatic conveying equipment is a top priority for HeadPowder. The company provides comprehensive maintenance services and support to help clients keep their systems running smoothly. Regular maintenance, such as cleaning the pipeline and checking the blower components, is essential to prevent clogs and ensure consistent performance. The use of high-quality materials and components in the construction of the equipment also contributes to its durability and longevity. HeadPowder's systems are designed with easy access points for maintenance, making routine checks and repairs more efficient. The company also offers training programs for clients to help them understand how to operate and maintain their equipment properly. This proactive approach to maintenance helps minimize downtime and extends the lifespan of the equipment. By investing in proper maintenance, businesses can maximize the return on their investment and ensure that their material handling processes remain efficient and reliable.
Conclusion
In conclusion, rice husk powder pneumatic conveying equipment from HeadPowder is a sophisticated and efficient solution for handling bulk materials in various industrial applications. The fundamental principles of using air to transport materials, combined with the key working scene characteristics of high efficiency, minimal contamination, and adaptability, make these systems indispensable in modern processing industries. With customization options and comprehensive maintenance support, HeadPowder provides tailored solutions that meet the specific needs of their clients. The advantages over traditional conveying methods, combined with the company's commitment to quality and reliability, make their pneumatic conveying systems a preferred choice for businesses looking to optimize their material handling processes. As industries continue to evolve, the demand for efficient and sustainable material handling solutions will only increase, and HeadPowder is well-positioned to meet these needs with their advanced pneumatic conveying equipment.




