

What is a Tonne Bag Unpacking and Material Conveying System? And What Are Its Design Principles?
When it comes to efficient material handling in industrial settings, the tonne bag unpacking and material conveying system emerges as a critical solution for managing bulk materials. This system is designed to streamline the process of unpacking large, heavy bags and transporting the contents to processing or storage areas. Understanding its components and design principles is essential for optimizing material flow and operational efficiency.
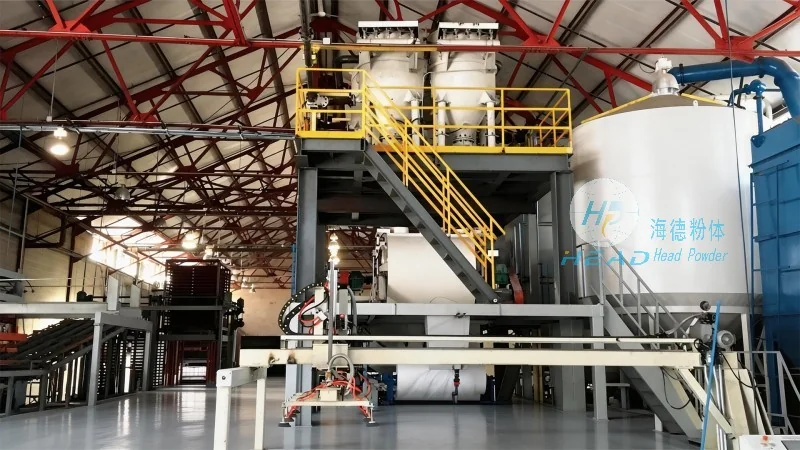
Overview of the Tonne Bag Unpacking and Material Conveying System
The tonne bag unpacking and material conveying system is a specialized piece of equipment used in various industries, including food processing, chemical manufacturing, and mining. It is engineered to handle the challenges associated with moving large quantities of bulk materials from the point of arrival to the point of use. The system typically integrates several key components, such as a bag opening mechanism, a hopper for collecting the material, and a conveyor system for transporting the material to the next stage of processing.
Key Components and Their Functions
At the heart of the tonne bag unpacking and material conveying system are several critical components that work in tandem to ensure smooth operation. The bag opening mechanism is designed to safely and efficiently open the tonne bag, allowing the material to flow into the hopper. This component may include a cutting blade or a hydraulic system that can be adjusted to accommodate different bag types and sizes. The hopper serves as a temporary storage container, collecting the material as it is released from the bag. It is typically made of durable materials, such as stainless steel, to withstand the handling of various bulk materials and to maintain hygiene standards. The conveyor system, which may include belt conveyors, screw conveyors, or pneumatic conveyors, is responsible for transporting the material from the hopper to the processing equipment or storage area. The choice of conveyor type depends on the material's characteristics, such as its density, moisture content, and flowability.
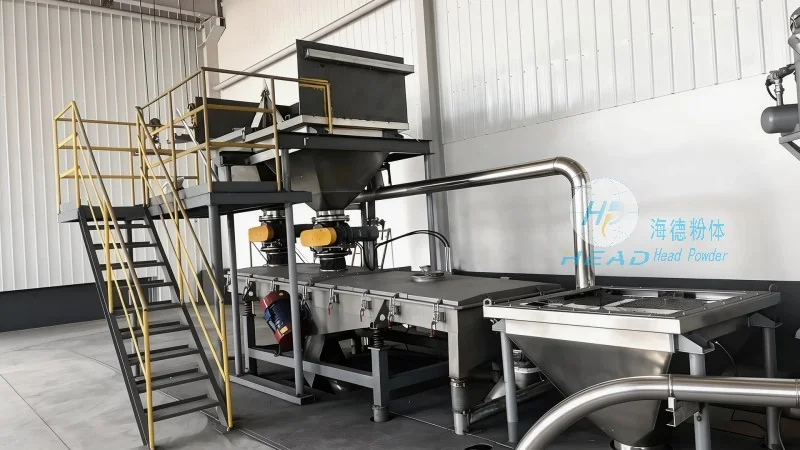
Design Principles and Engineering Considerations
The design of a tonne bag unpacking and material conveying system is guided by several key principles to ensure reliability, efficiency, and safety. One of the primary design principles is the integration of mechanical and control systems to achieve seamless operation. The system must be able to handle the weight and volume of tonne bags, which can weigh up to 1 tonne (or more in some cases), without compromising stability or safety. This requires robust structural design, including reinforced frames and heavy-duty components. Another important principle is the consideration of material compatibility. The system's components must be resistant to the chemical and physical properties of the materials being handled, such as abrasiveness, corrosiveness, or moisture content. For example, in food processing applications, the system may need to be made of food-grade materials to meet hygiene regulations. Control systems are also a critical part of the design, as they allow for automated operation, monitoring, and adjustment of the system's parameters. This includes sensors for detecting bag presence, level indicators for the hopper, and control panels for adjusting conveyor speed and other settings. The design also considers energy efficiency, with options for variable speed drives and energy-saving features to reduce operational costs.
Operational Workflow and Efficiency
The operational workflow of the tonne bag unpacking and material conveying system typically involves several steps. First, the tonne bag is placed on the opening mechanism, which may be a platform or a lifting device. The bag is then opened, and the material flows into the hopper. The hopper level is monitored, and when it reaches a certain level, the conveyor system is activated to transport the material to the next stage. The system may also include features such as bag emptying indicators and conveyor stop mechanisms to prevent overfilling or blockages. The efficiency of the system is influenced by several factors, including the speed of the conveyor, the capacity of the hopper, and the frequency of bag loading. By optimizing these parameters, the system can achieve high throughput rates, reducing downtime and increasing overall productivity. Additionally, the system's design allows for easy maintenance and cleaning, which is crucial for maintaining operational efficiency and meeting regulatory requirements.
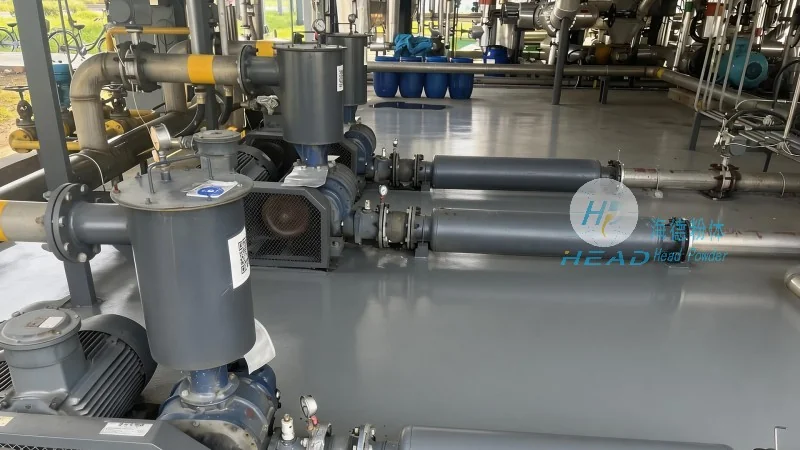
Applications and Industry Impact
The tonne bag unpacking and material conveying system is widely used in various industries due to its ability to handle large volumes of bulk materials efficiently. In the food industry, it is used for processing raw materials such as grains, flour, and sugar, where hygiene and material purity are paramount. In the chemical industry, it is used for handling chemicals and raw materials, where safety and material compatibility are critical. In the mining industry, it is used for transporting ore and other minerals from the mine to processing facilities. The system's versatility and adaptability make it a valuable asset in these industries, helping to improve operational efficiency and reduce labor costs.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of material handling equipment, specializing in the design and production of tonne bag unpacking and material conveying systems. With a focus on innovation and quality, the company has established itself as a trusted partner in the industry. HeadPowder's systems are engineered to meet the specific needs of its clients, with options for customization to accommodate different material types and operational requirements. The company's commitment to customer satisfaction and operational excellence has earned it a reputation for reliability and performance. HeadPowder's facilities are located in Shandong, China, where the company leverages its expertise and resources to develop cutting-edge solutions for material handling challenges. By partnering with HeadPowder, businesses can enhance their material flow processes and achieve greater operational efficiency.