Efficient material handling is a critical aspect of modern agricultural and industrial operations, especially when dealing with bulk materials like ammonium fertilizer. The challenge lies in transporting these fine and granular substances from storage to processing or application sites without loss, contamination, or operational inefficiencies. This is where airborne transport, or pneumatic conveying, emerges as a highly effective solution. By utilizing air flow to move materials, this method offers a reliable and efficient way to handle ammonium fertilizer and other similar powders.
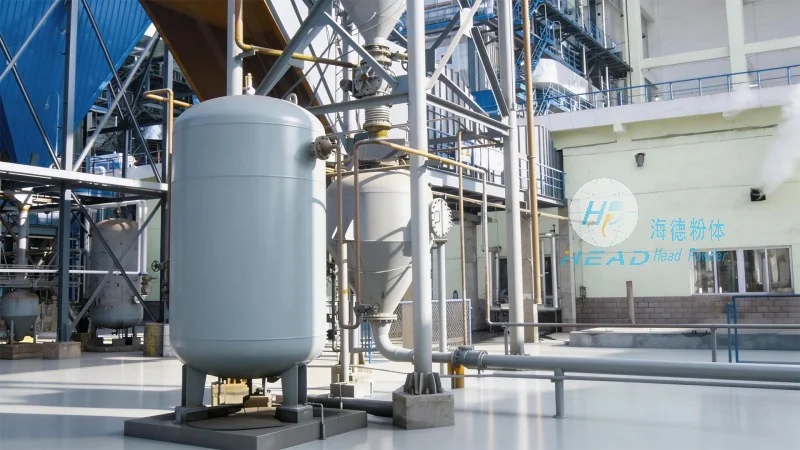
Pneumatic Conveying Systems: The Core Technology for Ammonium Fertilizer Transport
Pneumatic conveying systems operate by creating a pressure differential or using vacuum to move materials through a pipeline using air. There are two primary types: pressure and vacuum systems. Pressure systems use compressed air to push material forward, while vacuum systems create a negative pressure to draw material into the pipeline. For ammonium fertilizer, which is often sensitive to moisture and temperature, selecting the right system is crucial. Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in designing and manufacturing customized pneumatic conveying solutions tailored to the specific needs of fertilizer handling.
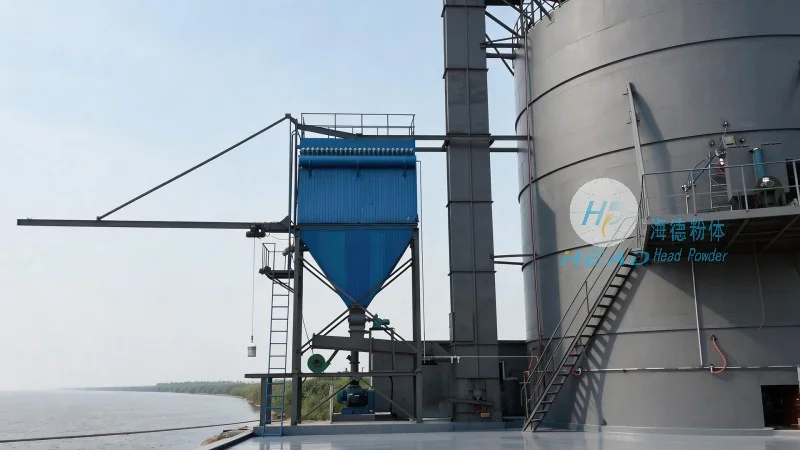
Key Advantages of Airborne Transport for Ammonium Fertilizer
Implementing airborne transport for ammonium fertilizer offers several significant advantages. First, it minimizes material degradation by reducing contact with external elements and preventing segregation. The enclosed pipeline system protects the fertilizer from moisture, dust, and contamination, ensuring product quality. Second, it enhances operational efficiency by allowing continuous, automated material movement, which reduces labor costs and increases throughput. Third, the system is highly flexible, capable of transporting materials over long distances and varying elevations without the need for complex mechanical components like conveyors or elevators. Additionally, it provides better safety by containing dust and preventing exposure to workers, aligning with modern industrial safety standards.
Customized Solutions by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. understands that each fertilizer handling operation has unique requirements. The company offers comprehensive services, from system design and engineering to installation and maintenance, ensuring that clients receive a solution that meets their specific needs. Their expertise lies in selecting the appropriate conveying method—whether pressure or vacuum—and designing the pipeline layout, including components like feeders, cyclones, and filters. The company’s team of engineers works closely with clients to assess the characteristics of the ammonium fertilizer, such as particle size, moisture content, and flowability, to optimize the system for maximum efficiency and reliability. By leveraging advanced technology and years of industry experience, HeadPowder provides solutions that not only improve material transport but also contribute to overall operational cost reduction and sustainability.
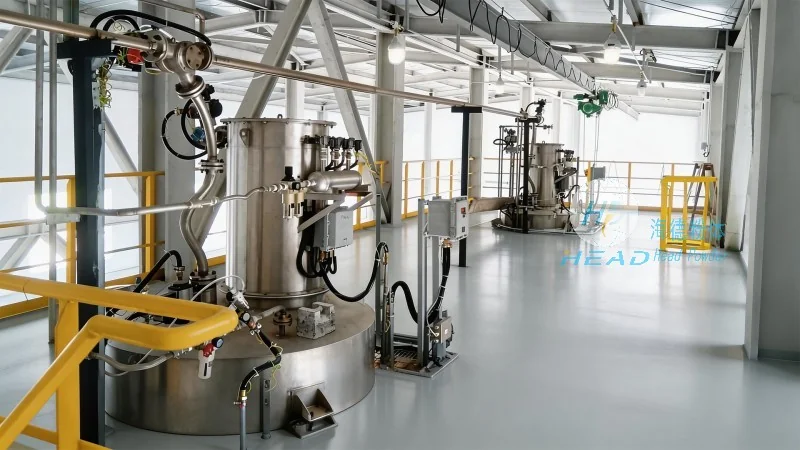
Ensuring Reliability and Durability in Ammonium Fertilizer Conveying
When transporting ammonium fertilizer, reliability and durability are paramount. The materials used in the conveying system must withstand the corrosive and abrasive nature of the fertilizer. Shandong HeadPowder Engineering Co., Ltd. utilizes high-quality materials, such as stainless steel and specialized plastics, to construct the pipelines and components. This ensures that the system can handle the demands of continuous operation without degradation or failure. Regular maintenance and monitoring are also part of the company’s service offerings, helping to prevent downtime and extend the lifespan of the equipment. By focusing on quality and durability, HeadPowder ensures that clients can rely on their airborne transport systems for long-term, efficient fertilizer handling.




