HeadPowder, a leading provider of industrial conveying solutions, specializes in the design, manufacturing, and installation of fertilizer granule pneumatic conveying systems. Based in Shandong, China, the company has established itself as a trusted partner for agricultural and chemical industries seeking efficient and reliable material handling solutions.
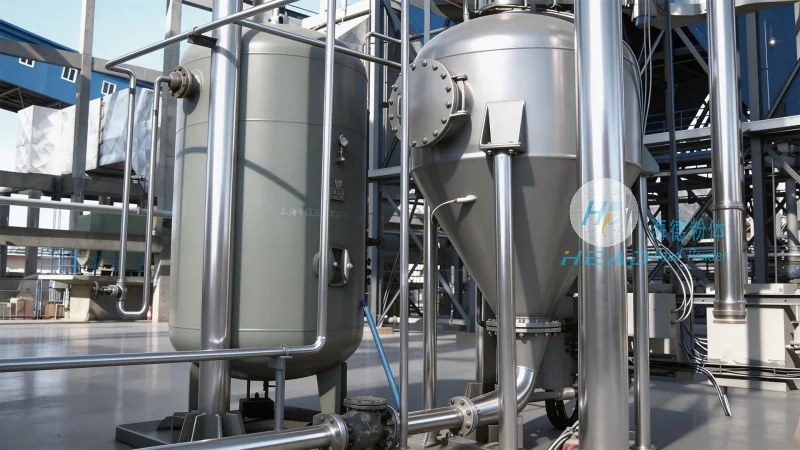
Overview of Fertilizer Granule Pneumatic Conveying Systems
Fertilizer granule pneumatic conveying systems are advanced industrial equipment used to transport bulk granular materials, such as nitrogen, phosphorus, and potassium fertilizers, from storage silos or production lines to processing or packaging units. These systems utilize air or gas as the conveying medium, enabling the movement of materials through pipelines without the need for mechanical components like belts or buckets. The technology offers significant advantages in terms of speed, flexibility, and reduced maintenance compared to traditional methods.
Key Components of the Pneumatic Conveying System
The fertilizer granule pneumatic conveying system consists of several critical components that work in tandem to ensure efficient material transport. The primary components include a material feed hopper, a rotary airlock valve, a conveying pipeline network, a dust collector, and a receiver or discharge hopper. The feed hopper stores the fertilizer granules and feeds them into the system at a controlled rate. The rotary airlock valve acts as a gate, preventing backflow and ensuring a steady flow of material into the pipeline. The conveying pipeline, typically made of stainless steel or other corrosion-resistant materials, transports the material using compressed air or gas. The dust collector removes airborne particles, improving air quality and preventing contamination. The receiver or discharge hopper collects the material at the destination point, ready for further processing or packaging.
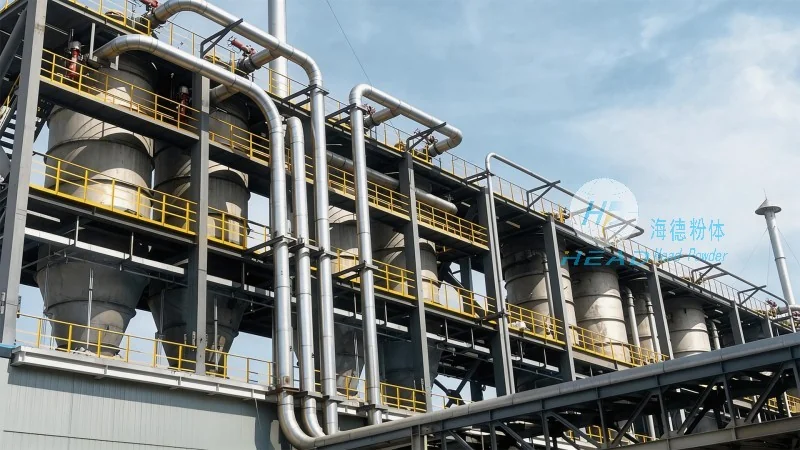
Working Principle of the System
The operation of the fertilizer granule pneumatic conveying system is based on the principle of pneumatic transport, where material is suspended in a stream of air and carried through the pipeline. The process begins with the material being fed from the hopper into the rotary airlock valve. As the valve rotates, it releases the material into the pipeline, where it is entrained by the high-velocity air stream. The air and material mixture travels through the pipeline to the receiver, where the material is separated from the air using a cyclone or other separation device. The separated material is collected in the receiver, while the air is filtered and discharged back into the environment or recirculated for energy efficiency. The system can operate in both positive and negative pressure modes, depending on the application requirements. Positive pressure systems use compressed air to push the material through the pipeline, while negative pressure systems use vacuum to pull the material from the source.
Advantages of Pneumatic Conveying for Fertilizer Granules
Compared to traditional mechanical conveying methods, fertilizer granule pneumatic conveying systems offer several key advantages. First, they provide high-speed and continuous material transport, reducing downtime and increasing production efficiency. Second, the system is highly flexible, allowing for changes in material flow direction or destination without major modifications. Third, the equipment is compact and requires less floor space, making it suitable for installations with limited area. Fourth, the system offers excellent dust control, as the material is contained within the pipeline and the dust collector captures airborne particles. Fifth, the maintenance requirements are lower, as there are fewer moving parts compared to mechanical systems. These advantages make pneumatic conveying an ideal solution for modern fertilizer processing and handling operations.
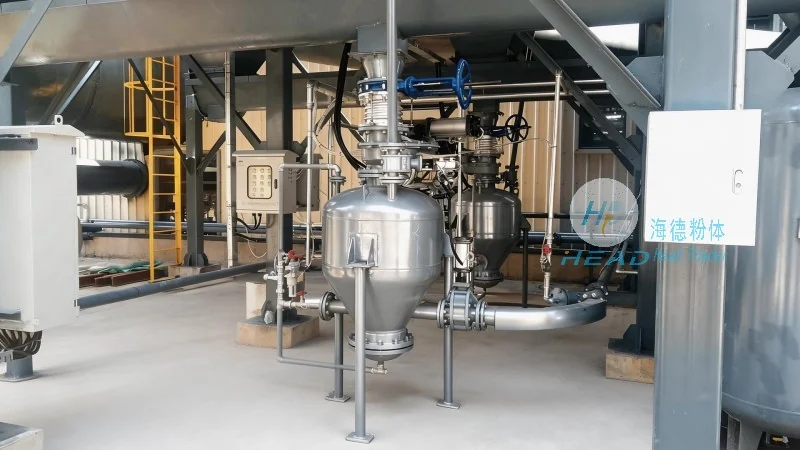
Applications and Industries Served
Fertilizer granule pneumatic conveying systems are widely used in various industries, including agriculture, chemical manufacturing, and food processing. In the agricultural sector, these systems are used to transport bulk fertilizers from storage facilities to farms or processing plants. In chemical manufacturing, they are employed to move raw materials or intermediates between production stages. The systems are also used in food processing for handling granular ingredients like sugar or salt. HeadPowder's systems are designed to meet the specific needs of these industries, ensuring reliable and efficient material handling.
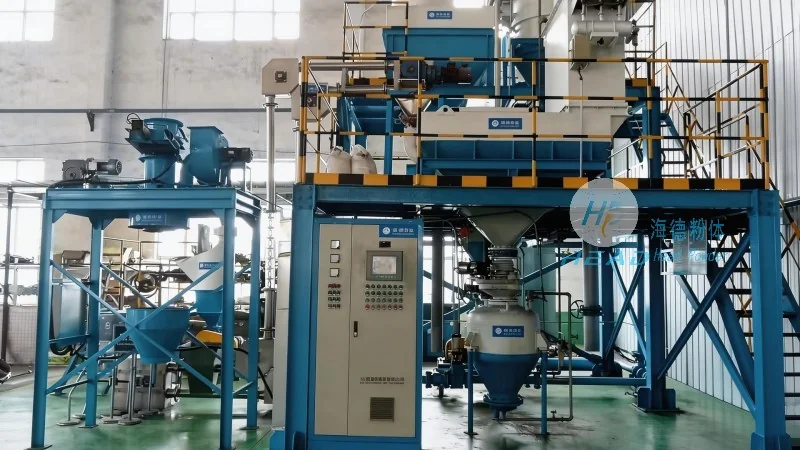
Customization and Installation Services
HeadPowder understands that each fertilizer processing facility has unique requirements. Therefore, the company offers customized pneumatic conveying solutions tailored to specific application needs. The design process involves a thorough analysis of the material characteristics, flow rates, and system layout to ensure optimal performance. HeadPowder's team of engineers works closely with clients to develop a system that meets their operational and budgetary constraints. The company also provides comprehensive installation and commissioning services, ensuring that the system is installed correctly and operates efficiently from the start. Additionally, HeadPowder offers maintenance and support services to ensure the long-term reliability of the equipment.
Conclusion
Fertilizer granule pneumatic conveying systems represent a significant advancement in material handling technology, offering efficient, reliable, and flexible solutions for the agricultural and chemical industries. HeadPowder, with its expertise and commitment to quality, provides top-tier pneumatic conveying systems that meet the highest standards of performance and durability. By leveraging advanced design and manufacturing techniques, HeadPowder ensures that its clients receive systems that enhance productivity, reduce costs, and improve overall operational efficiency.




