Multi-hopper pneumatic conveying systems are advanced industrial equipment designed to transport bulk materials efficiently over long distances. These systems are widely used in various industries, including chemical, food processing, and pharmaceuticals, due to their ability to handle a wide range of materials with minimal product degradation. The core of such systems lies in the multi-hopper design, which allows for the simultaneous or sequential feeding of different materials, enhancing operational flexibility and process control.
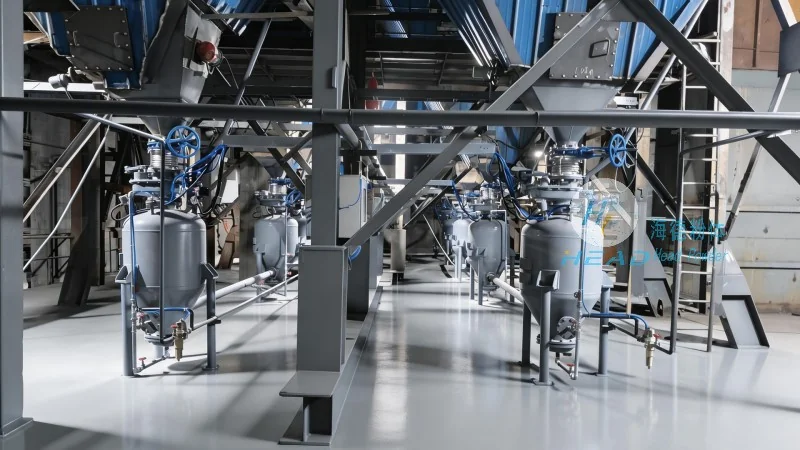
Key Components and Functionality of Multi-Hopper Pneumatic Conveying Systems
A typical multi-hopper pneumatic conveying system consists of several key components that work in tandem to achieve effective material transport. The primary components include the hoppers, which serve as storage vessels for different materials; the pneumatic conveying pipes, which use air pressure to move the material; and the control valves and pumps that regulate the flow and pressure. The multi-hopper design enables the system to handle multiple materials at once, reducing the need for separate equipment for each material type. This integration not only saves space but also improves overall operational efficiency.
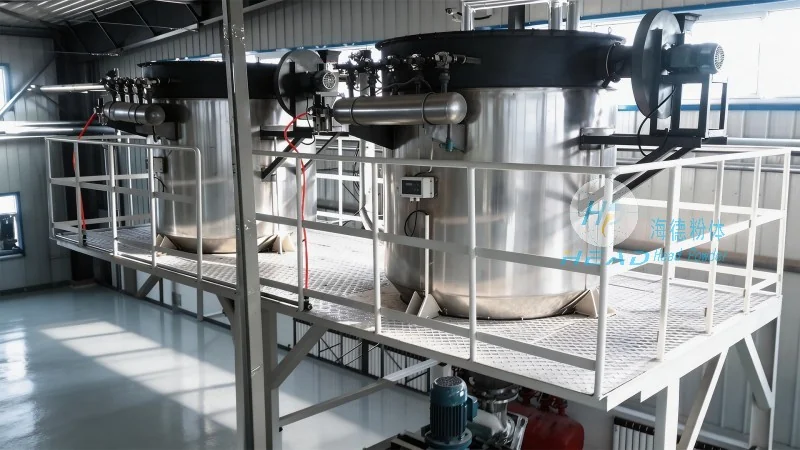
Design Principles Behind Multi-Hopper Pneumatic Conveying Systems
The design of a multi-hopper pneumatic conveying system is based on several fundamental principles that ensure optimal performance and reliability. One of the key principles is the use of differential pressure to move materials through the system. The system operates by creating a pressure difference between the inlet and outlet of the conveying line. This pressure difference is generated by a blower or compressor, which forces air through the pipes, carrying the material particles along with it. The design also considers the material characteristics, such as particle size, density, and flowability, to determine the appropriate air velocity and pressure required for effective transport. Additionally, the system is designed to minimize material degradation by controlling the air velocity and the length of the conveying line. This is crucial for materials that are sensitive to friction or high speeds.
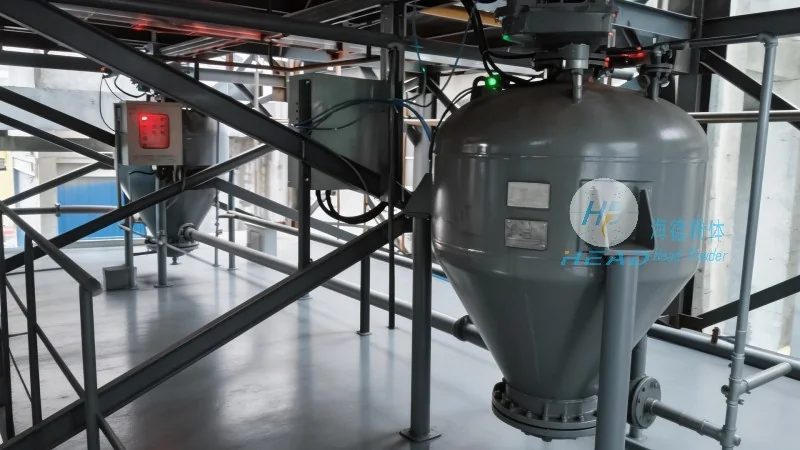
How Shandong HeadPowder Engineering Co., Ltd. Enhances Multi-Hopper Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in developing and manufacturing high-quality multi-hopper pneumatic conveying systems. With years of experience and a commitment to innovation, the company has developed systems that meet the diverse needs of various industries. The company's engineers focus on understanding the specific requirements of each client, from material properties to operational constraints, to design customized solutions that maximize efficiency and reliability. The multi-hopper systems produced by HeadPowder are known for their durability, ease of maintenance, and energy efficiency. The company's commitment to quality is reflected in its adherence to international standards and rigorous testing procedures, ensuring that each system meets the highest performance criteria.
Benefits of Using Multi-Hopper Pneumatic Conveying Systems
Implementing a multi-hopper pneumatic conveying system offers numerous benefits to industrial operations. One of the most significant advantages is the ability to handle multiple materials simultaneously, which reduces downtime and increases productivity. The system also minimizes the risk of cross-contamination, as each material is contained within its own hopper and conveyed through separate lines. This is particularly important in industries where product purity is critical, such as food and pharmaceuticals. Additionally, the system reduces labor costs by automating the material handling process, and it occupies less space compared to traditional methods like conveyor belts or trucks. The energy efficiency of the system also contributes to lower operational costs and a smaller environmental footprint.
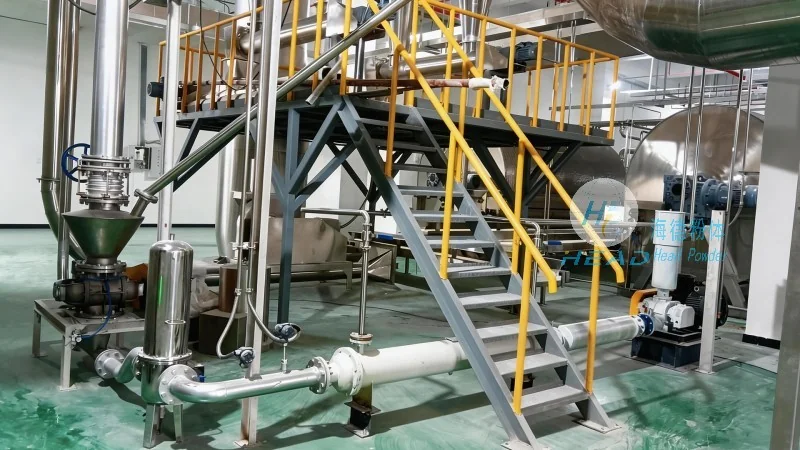
Applications and Industries Served by Multi-Hopper Pneumatic Conveying Systems
Multi-hopper pneumatic conveying systems are versatile and can be applied in a wide range of industries. In the chemical industry, they are used to transport powders and granules, such as chemicals and pigments. In the food processing industry, they are used to handle ingredients like flour, sugar, and spices, ensuring that the products remain fresh and uncontaminated. The pharmaceutical industry also benefits from these systems, as they can transport active pharmaceutical ingredients (APIs) and other sensitive materials with precision. Other industries that utilize multi-hopper pneumatic conveying systems include mining, agriculture, and plastics manufacturing. The adaptability of these systems makes them a preferred choice for companies looking to streamline their material handling processes.




