HeadPowder, a leading provider in the field of powder handling technology, specializes in the design and manufacturing of advanced conveying systems for various industrial applications. This document provides an overview of the Bentonite Powder Conveying System, highlighting its structural design and operational principles.
Company Profile
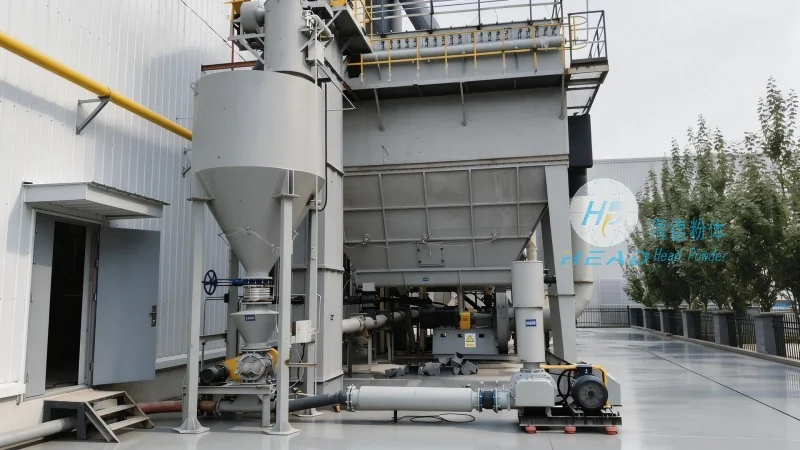
HeadPowder is represented by Shandong HeadPowder Engineering Co., Ltd., a company based in Shandong, China. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner for industries requiring efficient and reliable powder transport solutions. The company's expertise lies in developing customized systems tailored to meet the specific needs of clients across different sectors.
Overview of the Bentonite Powder Conveying System
The Bentonite Powder Conveying System is engineered to handle the unique characteristics of bentonite powder, a fine, cohesive material commonly used in drilling fluids, foundry applications, and other industrial processes. The system is designed to ensure efficient, low-dust, and safe transportation of the powder from storage to processing or application points. Key features include robust construction, precise control mechanisms, and compatibility with various operational environments.
Structural Components and Design
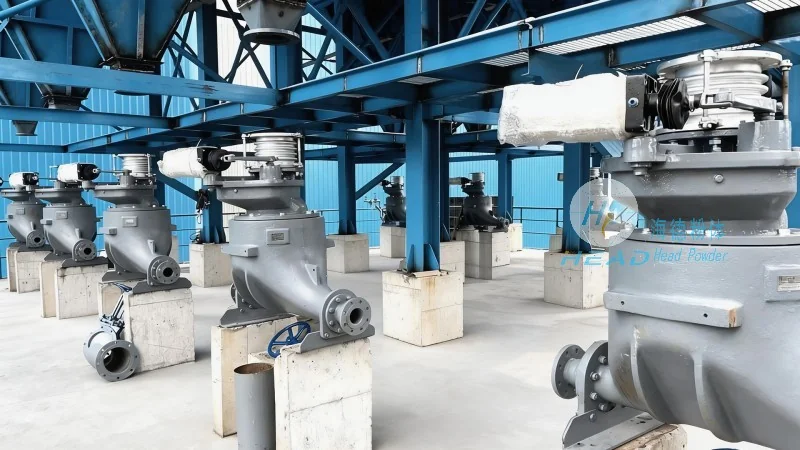
The system's structure comprises several critical components that work in tandem to facilitate smooth powder handling. The main elements include a hopper for material storage, a conveyor mechanism (such as a screw or pneumatic conveyor) for transport, and a control unit for regulating the flow rate. The hopper is typically equipped with a feeding device to ensure consistent material supply, while the conveyor system is designed to handle the cohesive nature of bentonite without causing blockages or degradation of the powder quality. Additionally, the system incorporates dust suppression features to maintain a clean and safe working environment.
Working Principle and Operational Mechanics
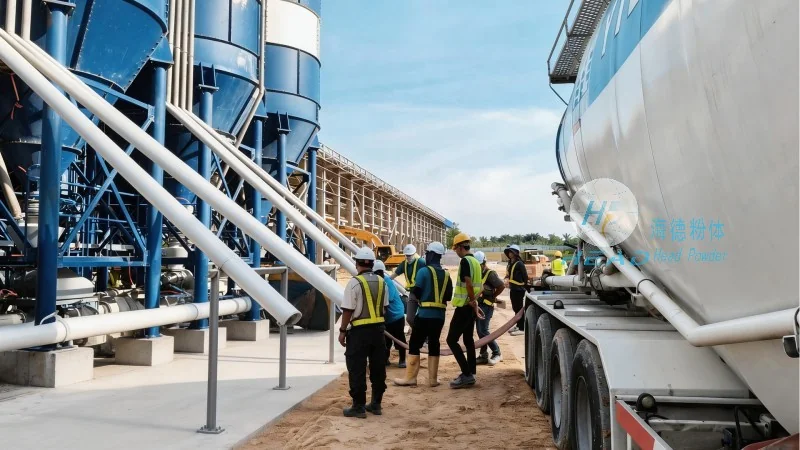
The operational principle of the Bentonite Powder Conveying System is based on the controlled movement of the powder through the system's components. The process begins with the material being fed into the hopper from a storage silo or bulk container. The feeding device then regulates the flow of powder into the conveyor. Depending on the chosen conveyor type, the powder may be transported via mechanical force (e.g., screw conveyors) or pneumatic pressure (e.g., air slides). The control unit monitors and adjusts the flow rate to maintain optimal performance, preventing overloading or underloading of the system. This ensures consistent delivery of the bentonite powder to the intended destination, whether it is for mixing, blending, or direct application.
Advantages and Applications
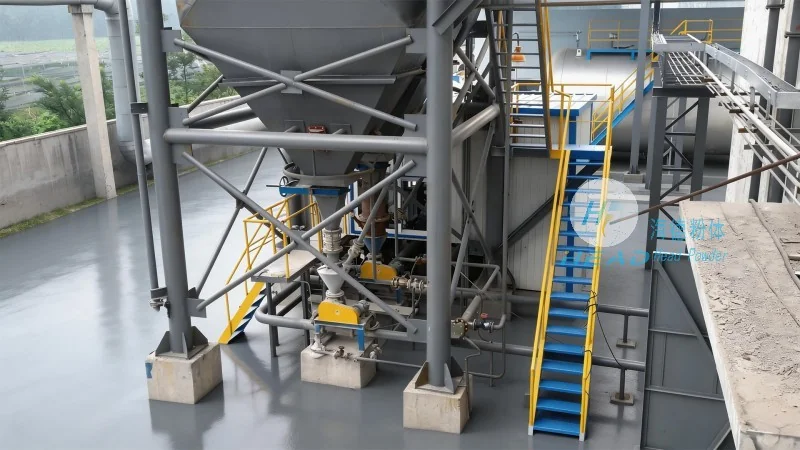
The Bentonite Powder Conveying System offers several advantages that make it suitable for a wide range of industrial applications. Its ability to handle fine, cohesive powders efficiently reduces material waste and improves process reliability. The system's low-dust operation enhances workplace safety and compliance with environmental regulations. Additionally, the modular design allows for easy integration into existing production lines and customization to accommodate varying production volumes. Typical applications include the supply of bentonite to drilling fluid mixing stations, foundry sand preparation lines, and other processes where precise powder control is critical.
Conclusion
HeadPowder's Bentonite Powder Conveying System represents a sophisticated solution for the efficient and reliable transport of bentonite powder. By combining robust structural design with advanced operational controls, the system ensures consistent performance and meets the stringent requirements of modern industrial applications. With its origins in Shandong, China, HeadPowder continues to deliver high-quality powder handling solutions that enhance productivity and safety in various industries.




