For industries handling bulk powder materials, efficient and reliable material transport is crucial. Pneumatic conveying equipment, such as those offered by Shandong HeadPowder Engineering Co., Ltd., provides a solution that combines advanced technology with practical application. This article explores the operation process and working principle of these systems, highlighting how they enhance productivity and safety in material handling operations.
Understanding Pneumatic Conveying Technology
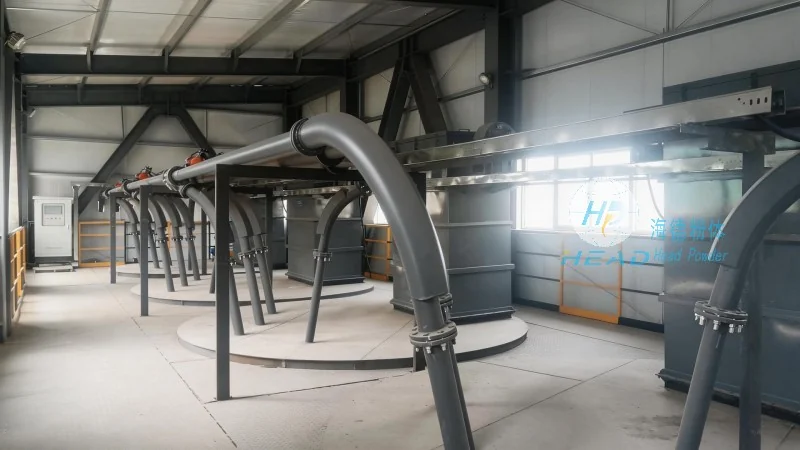
Pneumatic conveying systems utilize air or gas to transport dry bulk materials through a pipeline network. The core components include a material feed hopper, a conveyor line, and a discharge mechanism. The process begins with the material being fed into the system, where it is then entrained by a flow of air. This method is particularly effective for handling fine powders, granules, and other particulate materials that are sensitive to mechanical stress or contamination.
The Operation Process of Pneumatic Conveying Equipment
The operation of a pneumatic conveying system involves several key steps. First, the material is loaded into the feed hopper. A control system then regulates the air flow, ensuring the material is drawn into the conveyor line. As the material travels through the pipeline, it is carried by the air stream, which maintains a consistent velocity to prevent material deposition or blockages. The system typically includes pressure or vacuum control to manage the flow rate and direction of the material. At the discharge point, the material is separated from the air, often through a cyclone separator or filter, and collected in a receiving container. This process is continuous and can be automated to match production demands, ensuring a steady flow of material from the source to the destination.
Working Principle of Pneumatic Conveying Systems
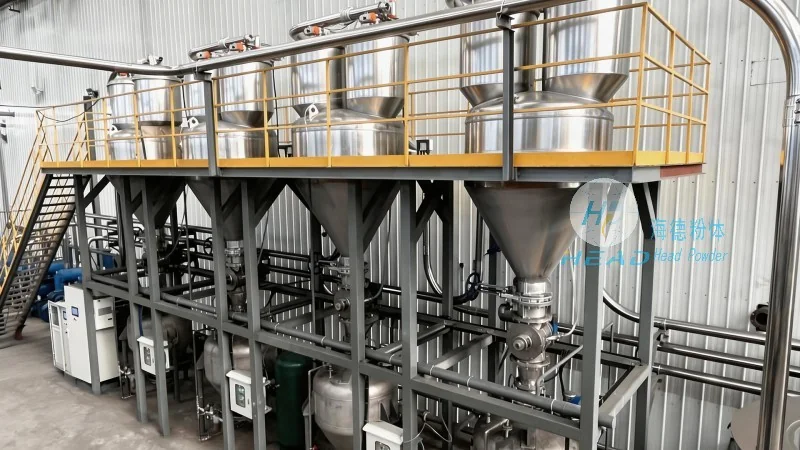
The working principle of pneumatic conveying relies on the interaction between the material particles and the air flow. In a pressure system, compressed air is used to push the material through the pipeline, while a vacuum system uses suction to draw the material from the source. The design of the system, including the diameter of the pipeline, the air velocity, and the material's properties, determines the efficiency and capacity of the conveying process. Advanced systems may incorporate features like pulse-jet cleaning to maintain pipeline integrity and prevent clogging, ensuring long-term operational reliability.
Key Benefits of Pneumatic Conveying Equipment
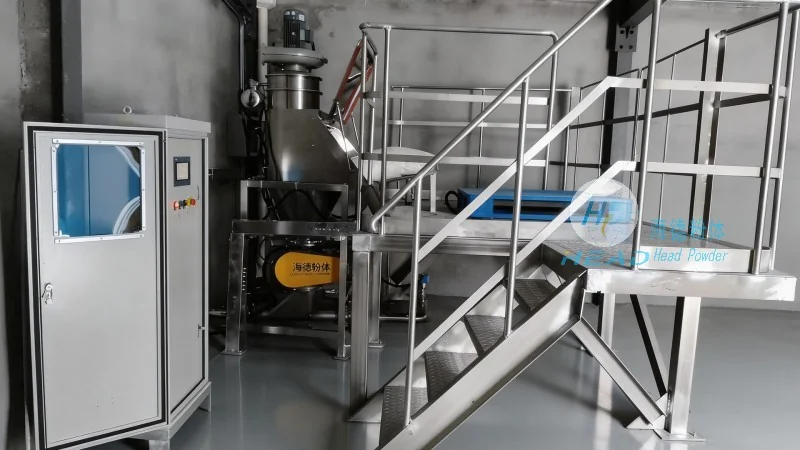
Implementing pneumatic conveying systems offers numerous advantages for industrial applications. These include reduced material handling time, minimized product contamination, and improved safety compared to traditional methods like bucket elevators or belt conveyors. The systems are also flexible, allowing for changes in material flow direction or destination without major modifications. Additionally, they can be integrated with other processing equipment, such as mixers or classifiers, to create a seamless material handling workflow. For companies in sectors like pharmaceuticals, food processing, and chemical manufacturing, these benefits translate into enhanced product quality and operational efficiency.
Application Examples and Industry Use Cases
Pneumatic conveying equipment is widely used across various industries. In the pharmaceutical industry, it is essential for transporting active ingredients and excipients with strict purity requirements. The systems ensure that the materials remain free from contamination and are handled gently to preserve their integrity. In the food industry, similar considerations apply, as the equipment can be designed to meet sanitary standards and handle food-grade powders. The chemical industry also benefits from these systems, particularly when handling hazardous or reactive materials, as the enclosed pipeline design minimizes exposure risks. Additionally, in the agricultural sector, pneumatic conveyors are used to transport grain and other agricultural products, improving storage and processing efficiency.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of pneumatic conveying equipment. With operations based in Shandong, China, the company specializes in designing and manufacturing customized solutions tailored to the specific needs of its clients. The company's products are engineered to meet international standards for quality and safety, ensuring reliable performance in demanding industrial environments. By combining expertise in material handling technology with a customer-centric approach, headpowder provides comprehensive solutions that enhance operational efficiency and reduce costs for its clients. The company's commitment to innovation and service has established it as a trusted partner in the industry, delivering high-performance pneumatic conveying systems that meet the evolving needs of modern manufacturing.




