HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. Among their portfolio is the tonne bag powder pneumatic conveying line, a robust and efficient system engineered to handle bulk powder materials with precision and reliability. This article delves into the operational process and underlying working principles of such a system, highlighting its key components, operational steps, and the technical mechanisms that ensure smooth material transport.
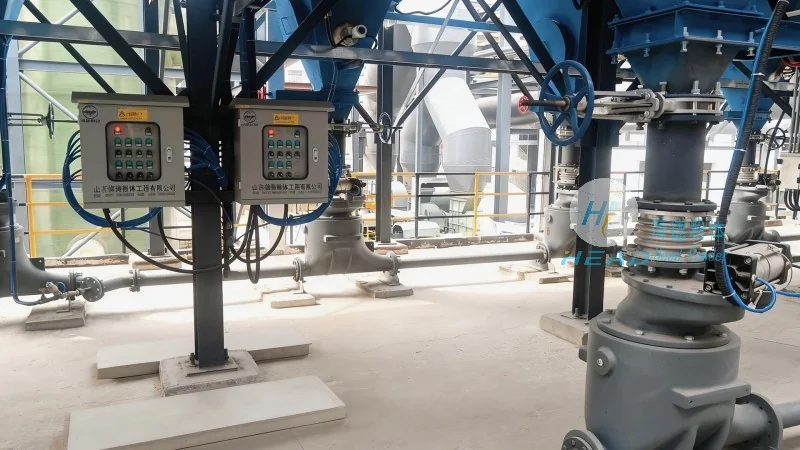
Overview of Tonne Bag Powder Pneumatic Conveying Systems
A tonne bag powder pneumatic conveying line is a closed-loop system designed to transport bulk powders from a storage point to a processing or discharge location. The system is particularly suited for handling materials that are prone to dust, require hygienic handling, or need to be transported over long distances without degradation. HeadPowder’s systems are built with high-quality materials and advanced engineering to meet stringent industry standards, ensuring durability and performance in various industrial applications.
Key Components of the Pneumatic Conveying Line
The tonne bag powder pneumatic conveying line consists of several critical components that work in tandem to facilitate material transport. These include the hopper or receiving tank, the air compressor or blower, the conveying pipeline, the control valves, the dust collection system, and the discharge or metering equipment. Each component plays a vital role in the overall operation, contributing to the system’s efficiency and safety.
Operation Process of the Tonne Bag Powder Pneumatic Conveying Line
The operation of a tonne bag powder pneumatic conveying line typically follows a sequential process that ensures consistent and controlled material flow. The process begins with the loading of the powder into the receiving hopper, which is often equipped with a feeding mechanism such as a rotary valve or a screw feeder to regulate the flow rate. Once the hopper is filled, the air compressor or blower is activated, generating a high-pressure air stream that is introduced into the conveying pipeline.
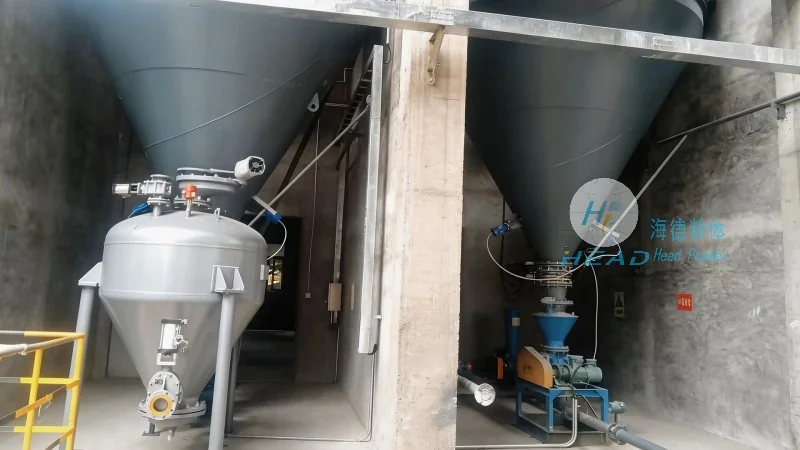
As the air flows through the pipeline, it creates a low-pressure zone that draws the powder particles into the air stream. The mixture of air and powder then travels through the pipeline to the discharge point, where the material is separated from the air using a cyclone separator or a filter system. The separated powder is then collected in a discharge bin or container, while the air is either recycled back into the system or filtered and released to the atmosphere.
Working Principle of the Pneumatic Conveying System
The core working principle of the tonne bag powder pneumatic conveying line is based on the principle of fluidization and pneumatic transport. The system utilizes compressed air to create a fluidized bed of powder particles, allowing them to be suspended and transported through the pipeline. This method, known as dilute phase conveying, is highly effective for transporting powders over moderate to long distances, as it minimizes material degradation and reduces the risk of blockages.
In the dilute phase operation, the air velocity within the pipeline is maintained at a level that keeps the powder particles in suspension without causing excessive pressure drops or energy consumption. The system’s control system continuously monitors parameters such as air pressure, flow rate, and material level, adjusting the operation to maintain optimal performance. This dynamic control ensures that the system operates efficiently, minimizing energy waste and maximizing material throughput.
Advantages of Tonne Bag Powder Pneumatic Conveying Lines
HeadPowder’s tonne bag powder pneumatic conveying lines offer several advantages over traditional material handling methods. These include the ability to handle abrasive or corrosive powders without damage to the system components, the reduction of dust emissions and environmental contamination, and the elimination of manual handling, which enhances workplace safety. Additionally, the closed-loop design of the system ensures that material loss is minimized, and the system can be integrated with other processing equipment for seamless operation.
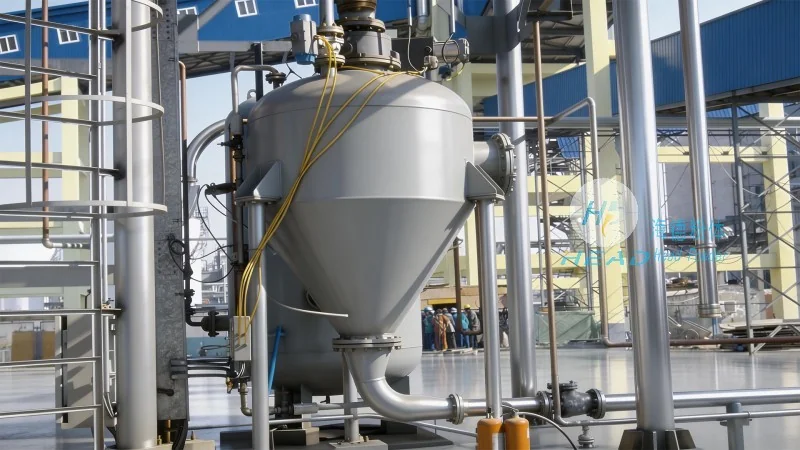
Applications and Industries
The tonne bag powder pneumatic conveying lines are widely used in various industries, including food and beverage, pharmaceuticals, chemicals, and minerals processing. In the food industry, the system is used to transport powders such as flour, sugar, and spices, ensuring hygienic and dust-free handling. In the pharmaceutical sector, the system is employed to handle active pharmaceutical ingredients (APIs) and other sensitive materials, maintaining strict contamination control. The chemical industry utilizes the system for transporting bulk chemicals, while the minerals processing industry uses it for handling raw materials like coal, cement, and limestone.
Maintenance and Safety Considerations
To ensure the long-term reliability and performance of the tonne bag powder pneumatic conveying line, regular maintenance is essential. HeadPowder recommends routine checks of the air compressor, pipeline integrity, and filter systems to prevent system failures. Additionally, the system should be equipped with safety features such as pressure relief valves, emergency shut-off switches, and dust explosion prevention measures to protect personnel and equipment.
HeadPowder, with its headquarters in Shandong, China, is committed to providing high-quality pneumatic conveying solutions that meet the diverse needs of industrial clients. Their expertise in system design and engineering ensures that each tonne bag powder pneumatic conveying line is tailored to the specific requirements of the application, delivering optimal performance and reliability.




