HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design, production, and supply of advanced pneumatic conveying equipment for various industrial applications. The company's core product, the coal ash powder pneumatic conveying system, is engineered to efficiently transport fine powders like coal ash, ensuring high reliability and minimal maintenance. This equipment is widely used in power plants, cement factories, and other industrial facilities where handling bulk powders is essential.
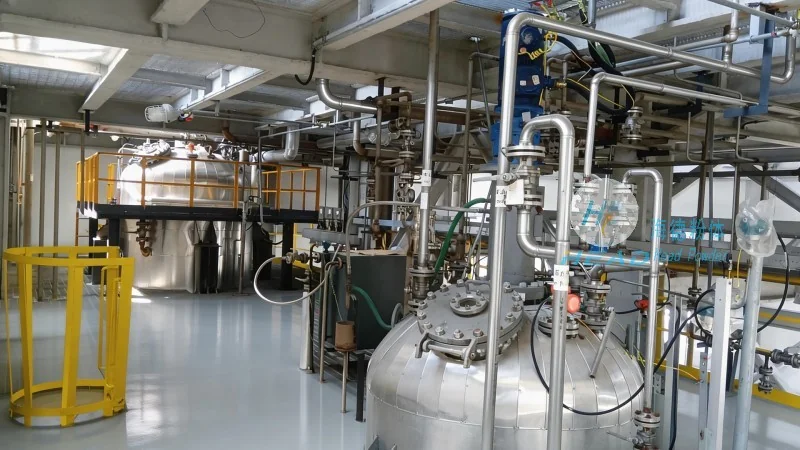
Coal Ash Powder Pneumatic Conveying Equipment Overview
The coal ash powder pneumatic conveying equipment from HeadPowder Engineering Co., Ltd. is a sophisticated system designed to handle the transportation of coal ash, a byproduct of coal combustion. The system integrates advanced pneumatic conveying technology, which uses air pressure to move powders through pipelines, eliminating the need for mechanical components like belts or buckets. This design not only reduces operational costs but also minimizes the risk of material contamination and equipment wear. The equipment is constructed with high-quality materials, ensuring durability and long service life under harsh industrial conditions.
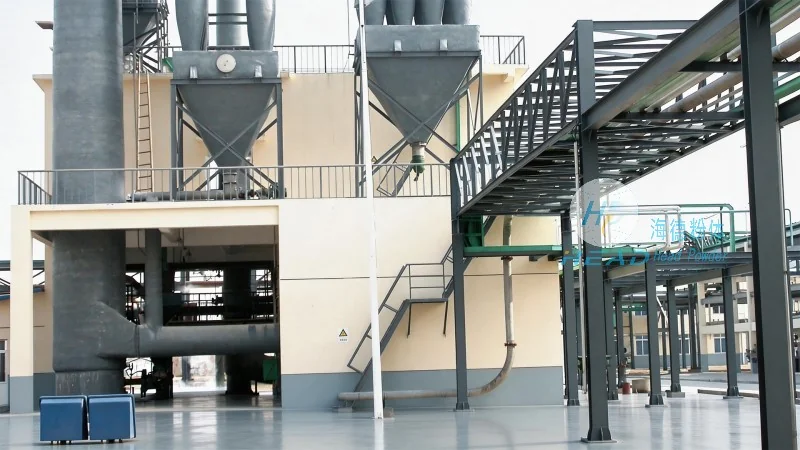
Operation Process of the Equipment
The operation process of the coal ash powder pneumatic conveying equipment involves several key steps. First, the coal ash is fed into the hopper or storage silo. From there, the material is drawn into the conveying line by a vacuum or pressure source, depending on the system configuration. The air and powder mixture travels through the pipeline to the destination point, such as a storage silo or processing unit. At the receiving end, the powder is separated from the air using a cyclone or filter system, and the air is then discharged or recirculated. The entire process is automated, with sensors and control systems monitoring the flow rate, pressure, and other critical parameters to ensure optimal performance. This automated operation enhances efficiency and reduces the need for manual intervention, making it suitable for continuous industrial production.
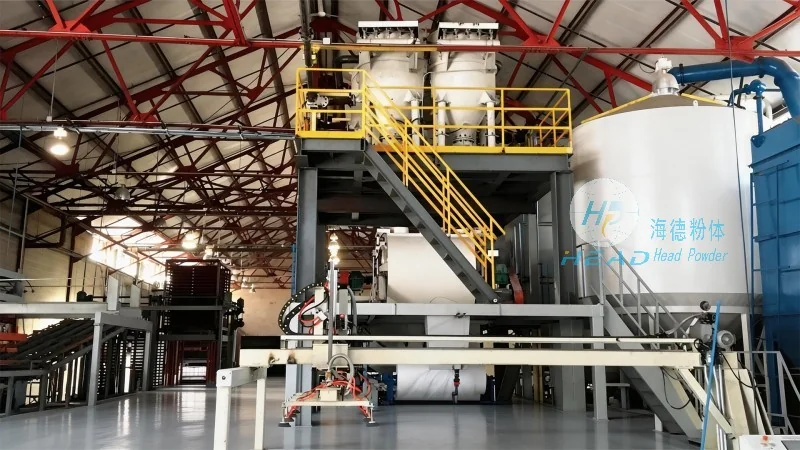
Working Principle of the Equipment
The working principle of the coal ash powder pneumatic conveying equipment is based on the fundamental physics of fluid dynamics. The system operates by creating a pressure differential between the inlet and outlet of the conveying line. In a vacuum system, the inlet is under a negative pressure, which draws the powder and air mixture into the pipeline. In a pressure system, the inlet is under positive pressure, pushing the mixture through the line. The coal ash particles are suspended in the air stream, allowing them to be transported over long distances without clogging the pipeline. The equipment uses a combination of air velocity and particle size to maintain a stable flow. The cyclone separator at the receiving end uses centrifugal force to separate the powder from the air, ensuring that the powder is collected efficiently and the air is either vented or recirculated. This separation process is crucial for maintaining the purity of the powder and preventing dust emissions, which is essential for environmental compliance in industrial settings.




