For industrial applications involving the handling of powder electrolytes, understanding the operation process and working principles of bulk material handling systems is crucial. This article provides a detailed overview of the mechanisms and processes involved in efficiently transporting and managing these materials, with a focus on the technical aspects that ensure reliable performance.
Introduction to Bulk Material Handling Systems for Powder Electrolytes
Bulk material handling systems are essential in industries such as battery manufacturing, where the efficient transport of powder electrolytes is critical for production efficiency and product quality. These systems are designed to handle large volumes of fine powders, ensuring minimal loss, contamination, and energy consumption. The operation process typically involves several key components and steps that work in tandem to achieve optimal performance.
Key Components of Powder Electrolyte Handling Systems
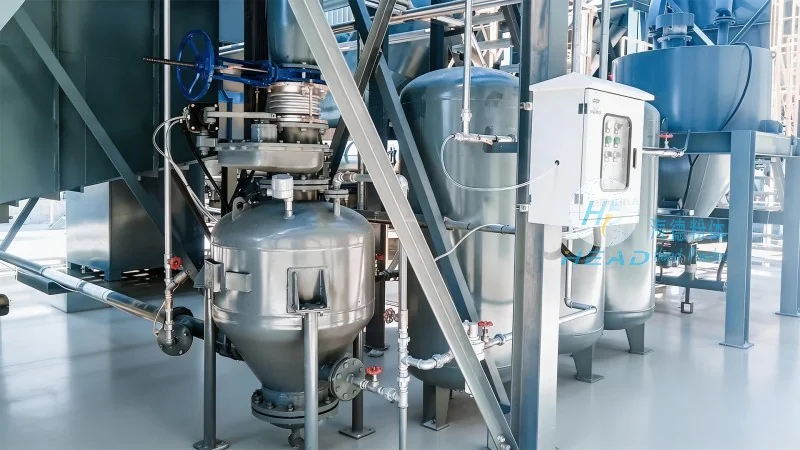
The core components of a typical powder electrolyte handling system include feeders, conveyors, storage silos, and control systems. Each component plays a vital role in the overall operation. Feeders, such as rotary or vibratory types, are used to regulate the flow of powder from storage silos to the conveyor system. Conveyors, often in the form of pneumatic or mechanical systems, transport the powder electrolyte to the processing or packaging areas. Storage silos provide a controlled environment for storing the powder, preventing moisture absorption and maintaining consistent material properties.
Operation Process of Powder Electrolyte Bulk Material Handling
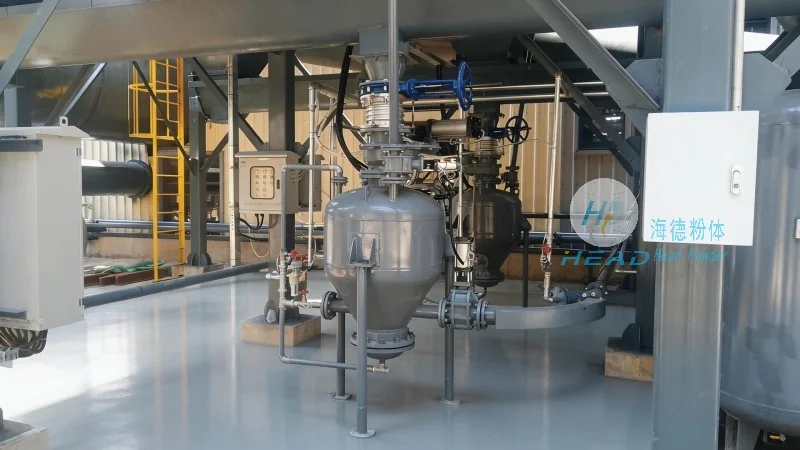
The operation process begins with the loading of powder electrolyte into the storage silo. The silo is equipped with level sensors to monitor the material level, ensuring proper inventory management. When the system is activated, the feeder starts to discharge the powder at a controlled rate. The powder then flows into the conveyor system, which transports it to the next stage of processing. The conveyor system may include features like airlocks or seals to prevent dust emissions and maintain a controlled environment. At the receiving end, the powder is discharged into a hopper or directly into the processing equipment. The entire process is monitored by a control system that adjusts the flow rate based on real-time demand and material levels.
Working Principle of the Handling Mechanisms
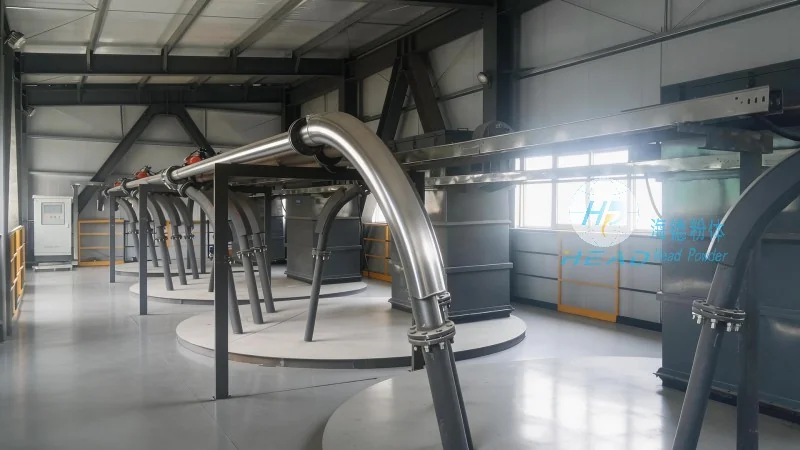
The working principle of powder electrolyte handling systems relies on the principles of fluidization and pneumatic transport. In fluidized bed systems, air is introduced into the powder bed, creating a fluid-like state that allows for uniform flow and reduced friction. This method is particularly effective for fine powders, as it minimizes particle agglomeration and ensures consistent material properties. Pneumatic conveyors use compressed air to move the powder through a pipeline, where the air velocity is carefully controlled to prevent particle separation and blockages. The system's design, including the size of the pipeline, air pressure, and material characteristics, is optimized to achieve efficient and reliable transport.
Role of Shandong HeadPowder Engineering Co., Ltd. in Bulk Material Handling Solutions
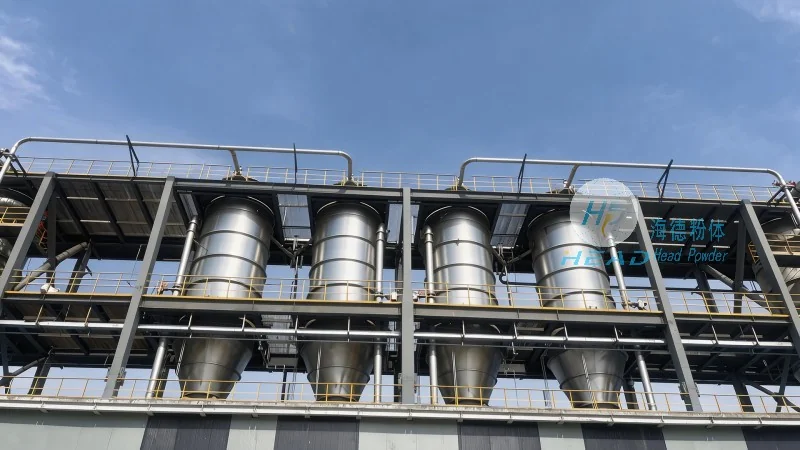
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, specializes in designing and manufacturing systems tailored to the specific needs of powder electrolyte applications. With a focus on innovation and quality, the company offers customized solutions that enhance operational efficiency and product integrity. The company's expertise in material handling technology ensures that clients receive systems that are reliable, durable, and compliant with industry standards. Based in Shandong, China, HeadPowder Engineering leverages local resources and expertise to deliver high-performance equipment for various industrial sectors.
Conclusion and Practical Applications
In conclusion, the operation process and working principles of powder electrolyte bulk material handling systems are complex but essential for modern industrial operations. By understanding the key components, operation steps, and underlying mechanisms, industries can optimize their material handling processes, reduce costs, and improve overall productivity. The expertise of companies like Shandong HeadPowder Engineering Co., Ltd. is instrumental in providing tailored solutions that meet the unique demands of powder electrolyte applications, ensuring efficient and reliable material transport in various industrial settings.




