Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design and manufacturing of advanced material handling systems tailored for the transportation of desulfurization and denitrification agents. These systems are critical components in industrial facilities that employ flue gas treatment technologies to reduce sulfur dioxide (SO₂) and nitrogen oxides (NOₓ) emissions. The efficient operation of such systems ensures consistent and safe delivery of these chemical agents, which are essential for maintaining compliance with environmental regulations and optimizing the performance of pollution control equipment.
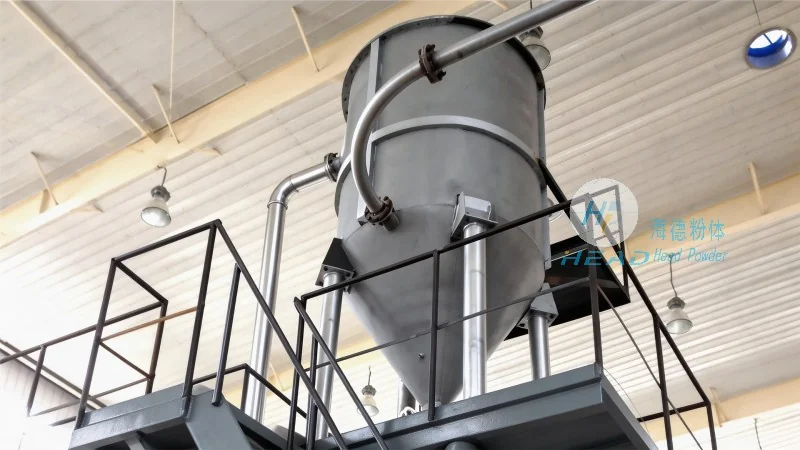
Principle of the Material Handling System
The core principle of the desulfurization and denitrification agent material handling system is to provide a reliable and controlled method for transporting bulk chemicals from storage to processing units. The system typically incorporates several key components, including storage silos, conveyor belts, pneumatic conveying systems, and control panels. Each component is engineered to handle the specific physical and chemical properties of the desulfurization and denitrification agents, such as their density, moisture content, and reactivity. The storage silos are designed with corrosion-resistant materials to prevent degradation of the agents and ensure long-term storage stability. Conveyor belts, often equipped with special coatings or liners, facilitate the smooth movement of the agents without causing degradation or contamination. Pneumatic conveying systems, which use compressed air to transport the agents in a closed pipeline system, offer flexibility in routing and can handle both dry and semi-dry agents. Control panels integrate sensors and automation technologies to monitor and regulate the flow rate, pressure, and temperature, ensuring precise and safe operation.
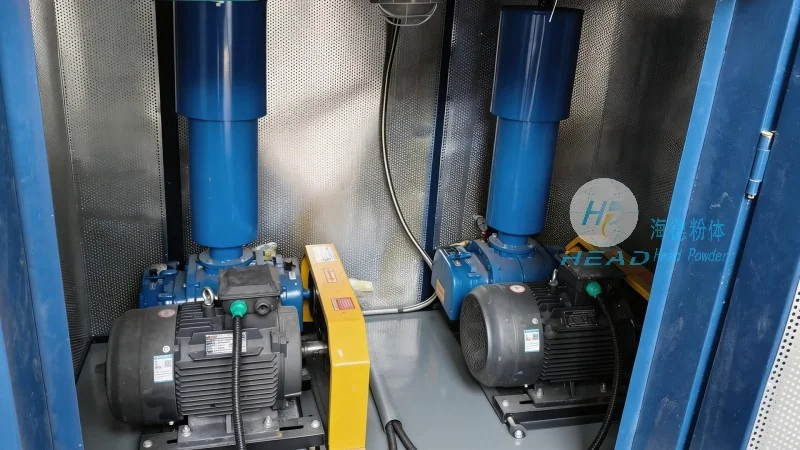
Key Operational Scenarios and System Features
The operational scenarios for these material handling systems vary based on the scale of the industrial facility and the specific requirements of the desulfurization and denitrification processes. For small to medium-sized plants, the system may consist of a single storage silo and a simple conveyor belt setup, capable of handling moderate volumes of agents. In larger industrial complexes, the system may include multiple silos, automated batching systems, and integrated control networks that coordinate the delivery of agents to multiple processing units. A notable feature of these systems is their ability to handle different types of desulfurization and denitrification agents, such as limestone, ammonia, or urea, by adjusting the system parameters and components. The systems are also designed to be compatible with existing infrastructure, allowing for seamless integration into existing industrial setups without significant modifications.
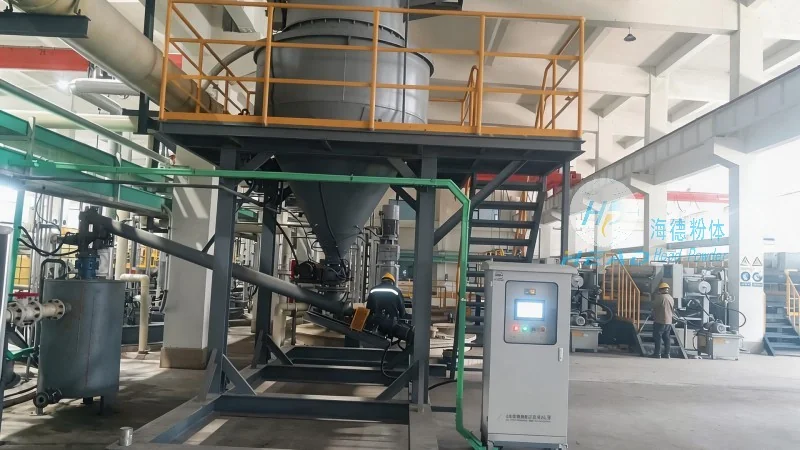
Advantages and Performance Characteristics
Shandong HeadPowder Engineering Co., Ltd.'s material handling systems for desulfurization and denitrification agents offer several advantages that enhance operational efficiency and safety. One of the primary benefits is the consistent and uniform delivery of agents, which is crucial for maintaining the optimal performance of the treatment equipment. The systems are engineered to minimize material degradation, ensuring that the chemical properties of the agents remain stable throughout the transportation process. This stability is critical for achieving consistent emission reduction rates and preventing equipment malfunctions. Additionally, the systems are designed with safety features, such as overpressure relief valves and emergency shut-off mechanisms, to prevent accidents and protect personnel and equipment. The use of corrosion-resistant materials and advanced sealing technologies further enhances the durability and longevity of the system, reducing maintenance costs and downtime.
Application Examples and Case Studies
The effectiveness of these material handling systems is demonstrated in various industrial applications across different sectors. For instance, in power plants, the system efficiently delivers limestone to the flue gas desulfurization (FGD) units, ensuring continuous and reliable operation of the scrubbers. In industrial boilers and manufacturing facilities, the system provides a consistent supply of ammonia or urea to the denitrification units, optimizing the reduction of nitrogen oxides emissions. A case study from a large thermal power plant in Shandong, China, shows that the implementation of a HeadPowder material handling system resulted in a 15% reduction in material handling time and a 10% decrease in maintenance costs compared to traditional manual or semi-automated systems. This improvement was attributed to the system's automated control features and efficient material flow management. Another example is from a chemical manufacturing plant, where the system successfully handled a new type of desulfurization agent, demonstrating its adaptability to different chemical compositions and process requirements.
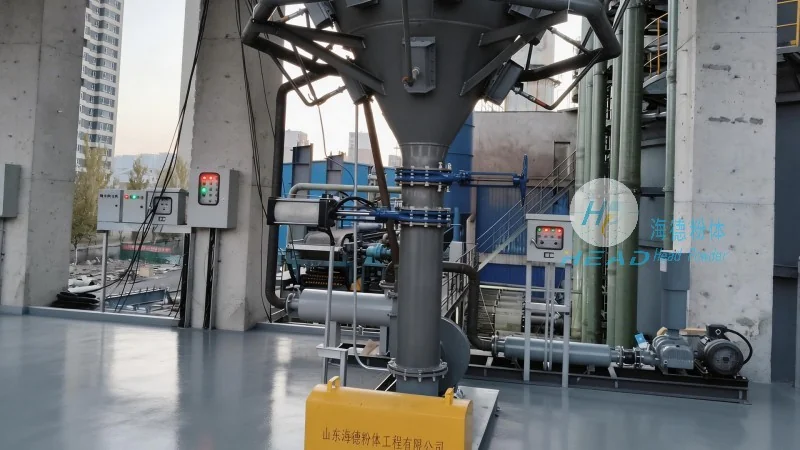
Conclusion and Future Developments
Shandong HeadPowder Engineering Co., Ltd.'s desulfurization and denitrification agent material handling systems represent a sophisticated solution for the efficient and safe transportation of critical industrial chemicals. By integrating advanced engineering, automation, and material science, these systems ensure consistent performance, compliance with environmental standards, and operational reliability. As industrial facilities continue to prioritize sustainability and efficiency, the demand for such advanced material handling systems is expected to grow. Future developments may include the integration of artificial intelligence and machine learning for predictive maintenance, real-time monitoring of agent quality, and further optimization of energy consumption in the transportation process. These advancements will further enhance the capabilities of the systems, making them even more effective in supporting the environmental goals of industrial operations.




