Principle and Working Scene Characteristics of Tonne Bag Dust-Free Feeding Station Pneumatic Conveyi
Release time:2026-09-19 00:01:29
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
For industrial applications requiring efficient and dust-free material handling, the tonne bag dust-free feeding station with pneumatic conveying system represents a sophisticated solution. This equipment is designed to streamline the process of transferring bulk materials from large bags into processing systems while maintaining a clean and controlled environment. The system integrates advanced technology to ensure minimal dust generation and optimal material flow, making it ideal for industries such as pharmaceuticals, food processing, and chemical manufacturing where air quality and product purity are critical. Developed by Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial material handling solutions, this system exemplifies the company's commitment to innovation and quality.
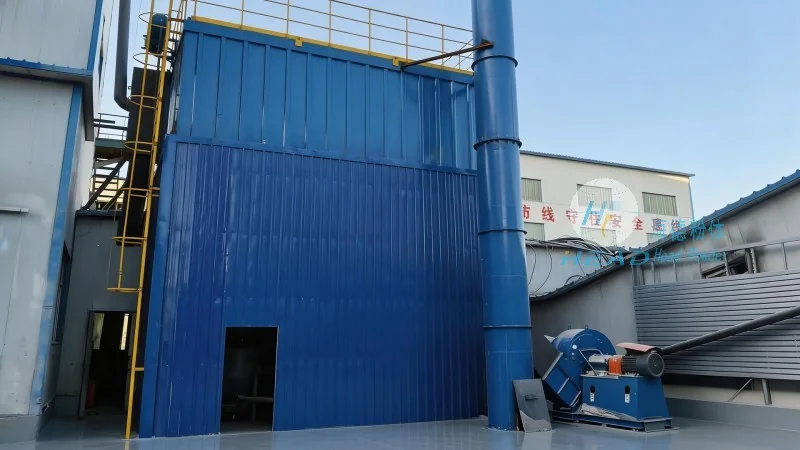
Principle of the Tonne Bag Dust-Free Feeding Station Pneumatic Conveying System
The core principle of this system revolves around the use of air pressure to transport bulk materials from a tonne bag into a processing unit. The process begins with the placement of a large bag containing the material onto a designated feeding platform. The system then uses a combination of vacuum or pressure air to create a flow path that draws the material from the bag and conveys it through a pipeline to the target destination. Key components include a bag opening mechanism, a hopper with a dust filter, and a conveying line equipped with control valves and a dust collection system. The design ensures that the material is transferred without direct human contact, reducing the risk of contamination and improving operational safety. The engineering approach by HeadPowder focuses on creating a seamless material transfer process that aligns with industry standards for cleanliness and efficiency.
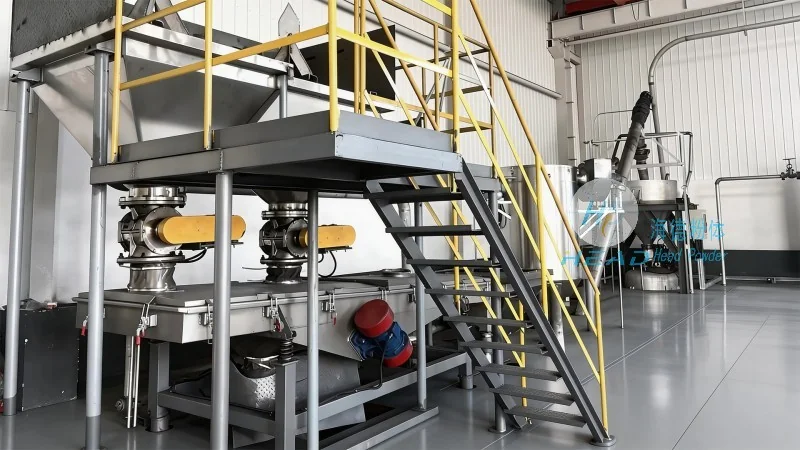
Working Scene Characteristics and Application Advantages
The tonne bag dust-free feeding station is particularly suited for scenarios where large quantities of bulk materials need to be handled in a controlled environment. Its dust-free operation is crucial in industries such as pharmaceuticals and food processing, where maintaining air quality is paramount. The system's ability to handle various materials, including powders and granules, makes it versatile for different production needs. Additionally, the integration of a dust collection system ensures that any airborne particles are captured and filtered, preventing environmental contamination and maintaining compliance with regulatory standards. The compact design of the station allows for easy installation in existing production lines, minimizing downtime and facilitating seamless integration into existing workflows. As a product of Shandong HeadPowder Engineering Co., Ltd., this system reflects the company's expertise in designing solutions that address the specific challenges of modern industrial operations.
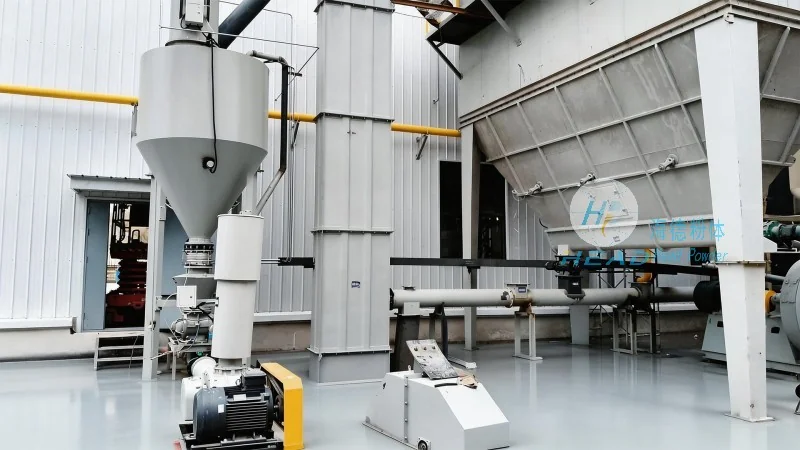
Technical Features and Operational Efficiency
Shandong HeadPowder Engineering Co., Ltd. has developed this system with a focus on enhancing operational efficiency and reliability. The equipment incorporates advanced control systems that allow for precise regulation of air flow and material transfer, ensuring consistent performance. The dust filter and collection system are designed to capture fine particles, maintaining a clean working environment. The feeding station is equipped with safety features, such as automatic shut-off in case of blockages or overpressure, which enhances operational safety. The system's low maintenance requirements and long service life contribute to cost-effective operation over time. By leveraging the expertise of HeadPowder, users can benefit from a solution that combines innovation with practicality, tailored to meet the specific demands of their industrial processes. The company's location in Shandong, China, provides a strategic advantage in terms of manufacturing and supply chain management, ensuring timely delivery and support for clients worldwide.




