HeadPowder, the professional brand under Shandong HeadPowder Engineering Co., Ltd., specializes in the research, development, and manufacturing of advanced pneumatic conveying systems. With a strong engineering foundation and a focus on innovation, the company has established itself as a leading provider of solutions tailored for soil and bulk material handling. Headquartered in Shandong, China, HeadPowder leverages decades of industry experience to deliver reliable and efficient equipment that meets the diverse needs of construction, mining, and environmental sectors.
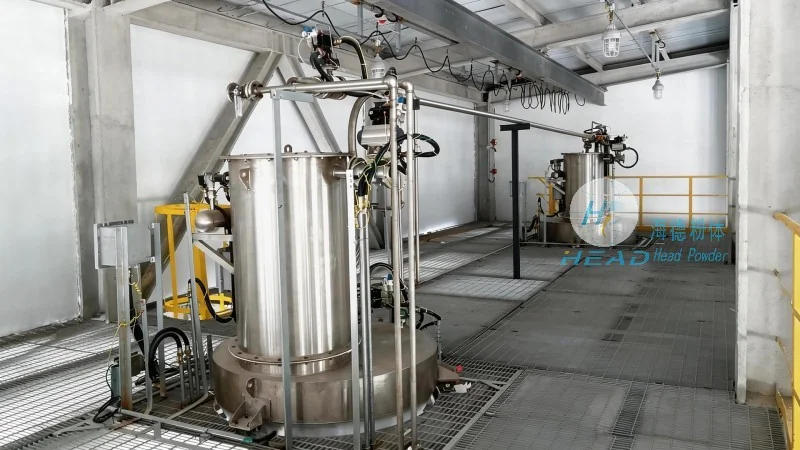
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a reputable enterprise dedicated to the design and production of high-quality pneumatic conveying equipment. The company's commitment to technological advancement and customer satisfaction has positioned it as a trusted partner in the material handling industry. Headquartered in Shandong, China, the company operates with a team of skilled engineers and technicians who bring expertise in both mechanical and pneumatic systems. By combining traditional engineering principles with modern manufacturing techniques, HeadPowder ensures that its products meet international standards while offering competitive pricing and comprehensive after-sales support.
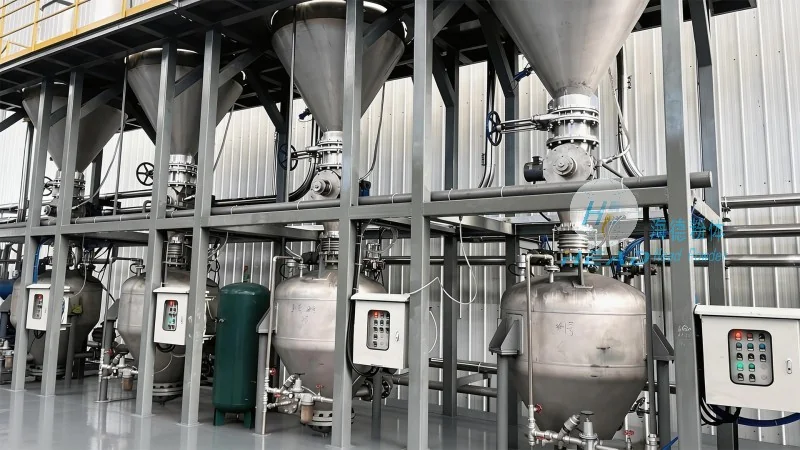
The Principle of Pneumatic Conveying Technology
The core principle of soil pneumatic conveying equipment lies in the use of compressed air to transport granular or powdery materials through a pipeline system. Unlike traditional mechanical conveyors, this technology eliminates the need for moving parts in the conveying path, reducing maintenance requirements and enhancing operational safety. The system typically consists of a material hopper, an air compressor, a pipeline network, and a discharge unit. When the material is introduced into the hopper, the air compressor generates a high-pressure airflow that draws the material into the pipeline. The air and material mixture travels through the pipeline, with the air pressure maintaining the material in suspension. At the discharge point, the air pressure is reduced, causing the material to separate from the air and be deposited in the target location. This process is highly efficient for transporting soil, sand, and other fine or coarse particulate materials over varying distances, from short on-site transfers to long-distance industrial applications. The technology's ability to handle materials with different properties, such as moisture content and particle size, makes it versatile for diverse soil types and operational needs.
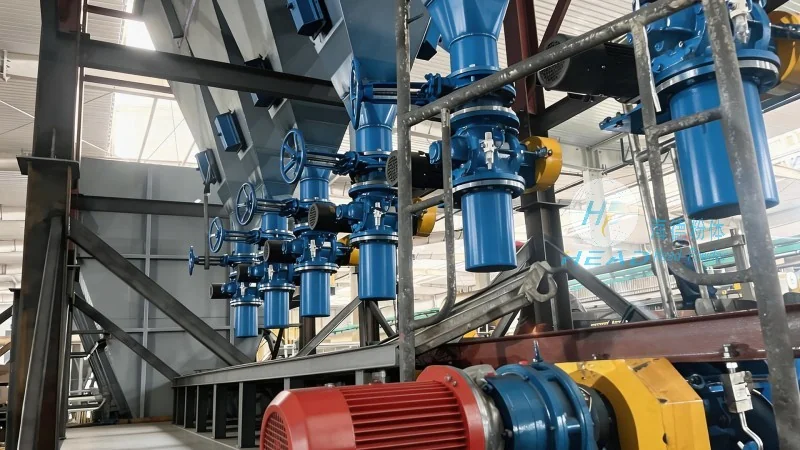
Key Working Scene Characteristics
HeadPowder's soil pneumatic conveying equipment is designed to excel in a range of working scenarios, each with unique challenges and requirements. The equipment's adaptability makes it suitable for both indoor and outdoor applications, from construction sites where soil needs to be moved between different areas to industrial facilities handling raw materials. One key characteristic is its ability to handle materials with varying moisture content and particle sizes, ensuring consistent performance even when dealing with challenging soil types. The system's compact design allows for easy integration into existing workflows, minimizing disruption during installation and operation. Additionally, the pneumatic conveying method reduces dust generation compared to traditional methods, contributing to a cleaner working environment and improved safety for personnel. In mining operations, the equipment can efficiently transport excavated soil from the site to processing facilities, while in environmental remediation projects, it aids in the removal and disposal of contaminated soil. The flexibility of the system also enables it to handle multiple material types simultaneously, making it a versatile solution for complex projects. For example, in a construction project, the equipment can move excavated soil from the excavation site to a storage area or disposal site without the need for manual labor or heavy machinery, streamlining the workflow and reducing project timelines.
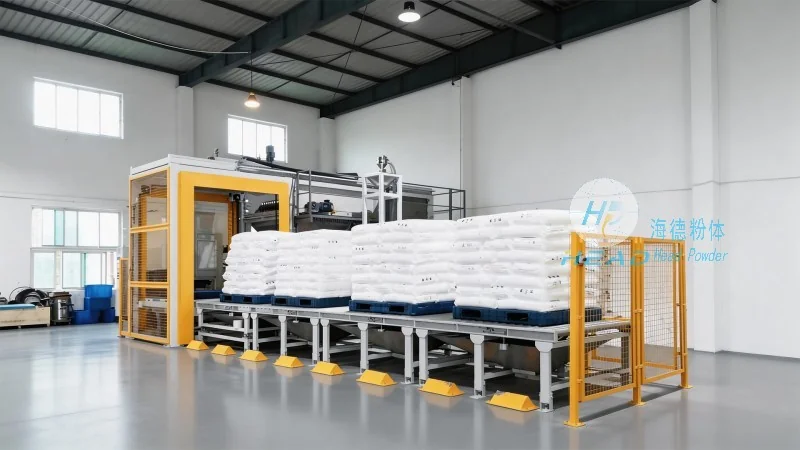
Technical Advantages and Practical Applications
Technical advantages of HeadPowder's soil pneumatic conveying equipment include high efficiency in material transport, with minimal energy consumption compared to mechanical conveyors. The absence of moving parts in the pipeline reduces wear and tear, leading to lower maintenance costs and longer equipment lifespan. The system's ability to operate in harsh environments, such as dusty or wet conditions, makes it ideal for outdoor construction and mining sites. Furthermore, the equipment's modular design allows for easy customization to meet specific project requirements, including varying pipeline lengths, material capacities, and pressure levels. Practical applications span across multiple industries, including construction, where it is used for moving soil from excavation sites to storage areas or disposal sites; mining, where it facilitates the transport of excavated earth to processing plants; and environmental management, where it aids in the remediation of contaminated soil by safely transporting it to treatment facilities. The equipment's reliability and performance have made it a preferred choice for projects requiring consistent and efficient material handling, even in challenging conditions. For instance, in a large-scale mining operation, the pneumatic conveying system can transport thousands of tons of soil per day, ensuring that the mining process remains uninterrupted and that material handling is carried out safely and effectively. In environmental projects, the equipment helps in the controlled removal of contaminated soil, reducing the risk of environmental contamination and ensuring compliance with regulatory standards.




