HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. Among their portfolio is the borax granule pneumatic conveying system, a technology that efficiently transports borax granules through a network of pipes using air pressure. This system is engineered to meet the specific demands of borax processing and handling, ensuring reliability, efficiency, and safety in industrial applications.
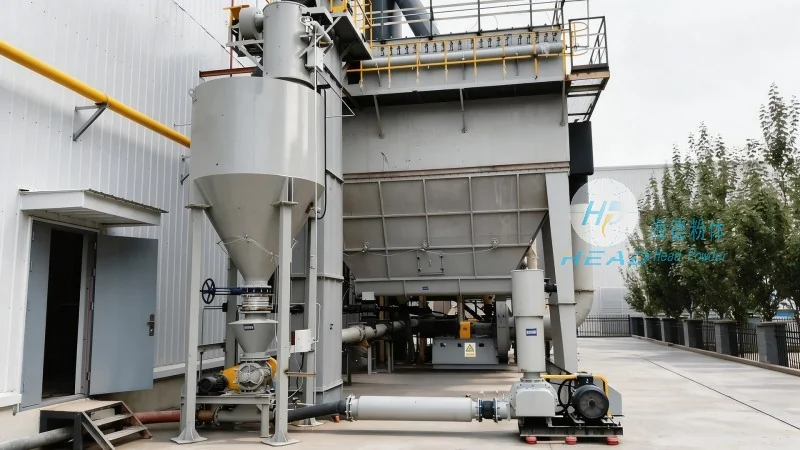
The Principle of Pneumatic Conveying for Borax Granules
The core principle of the borax granule pneumatic conveying system lies in the use of air as the conveying medium. The system operates by creating a pressure differential within a closed pipeline. At the inlet, air is introduced, often through a blower or compressor, which generates sufficient force to lift and move the granular borax particles. The design incorporates components such as feeders, cyclones, and filters to control the flow and separation of the material. The system’s efficiency is determined by factors like the particle size, density, and moisture content of the borax, as well as the air velocity and pressure within the pipeline. HeadPowder’s engineering expertise ensures that these parameters are optimized to achieve consistent and reliable transport of borax granules, minimizing material degradation and system downtime.
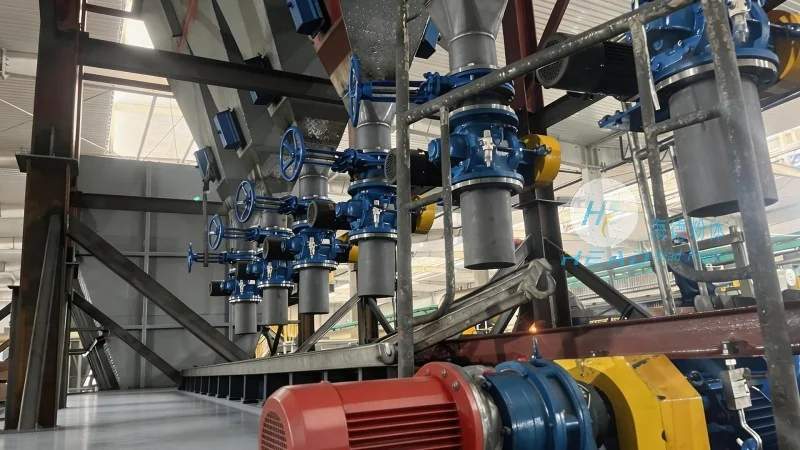
Key Working Scene Characteristics
The working scene characteristics of the borax granule pneumatic conveying system are tailored to the unique requirements of borax processing facilities. These characteristics include high throughput capabilities, which allow for the rapid movement of large volumes of borax granules, essential for meeting production demands in industrial settings. The system is also designed for flexibility, enabling integration with existing processing lines and adaptability to varying production scales. Another critical characteristic is its ability to handle abrasive materials, as borax granules can be hard and potentially damaging to equipment if not transported properly. The system’s design incorporates wear-resistant components and efficient separation mechanisms to mitigate these risks. Additionally, the system is engineered for safety, with features like dust suppression and pressure relief valves to prevent accidents and ensure compliance with industrial safety standards. The working scene also emphasizes energy efficiency, as the system is designed to minimize air consumption while maintaining optimal conveying performance, reducing operational costs for the end-user.
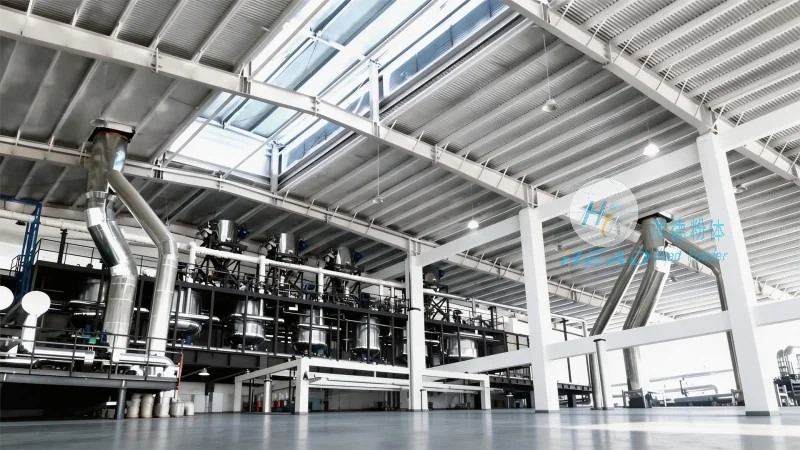
Applications and Benefits in Industrial Settings
The borax granule pneumatic conveying system is widely used in various industrial applications where the efficient handling of borax granules is critical. These applications include chemical manufacturing, where borax is used as a raw material in the production of detergents, glass, and other chemical products. The system’s ability to transport borax granules from storage silos to processing units, or between different stages of production, enhances workflow efficiency and reduces manual handling risks. In mining and mineral processing industries, the system is employed to move borax ore from extraction sites to processing plants, ensuring a continuous supply of raw material. The benefits of this system extend beyond operational efficiency; it also contributes to environmental sustainability by reducing the need for manual handling and minimizing material loss during transport. Furthermore, the system’s compact design and modular components allow for easy installation and maintenance, making it a cost-effective solution for industrial facilities. HeadPowder’s commitment to quality and innovation ensures that their borax granule pneumatic conveying systems deliver superior performance, reliability, and longevity, meeting the stringent demands of modern industrial operations.




