For industries dealing with bulk powder and granular materials, efficient material handling is crucial for operational efficiency and cost management. Pneumatic conveying systems have emerged as a reliable solution for transporting dust and fine particles over short to medium distances. These systems utilize air pressure or vacuum to move materials from one location to another, offering advantages such as reduced contamination, lower maintenance requirements, and the ability to handle sensitive or hazardous materials. Understanding the working principle and key features of these systems is essential for selecting the right equipment for specific applications.
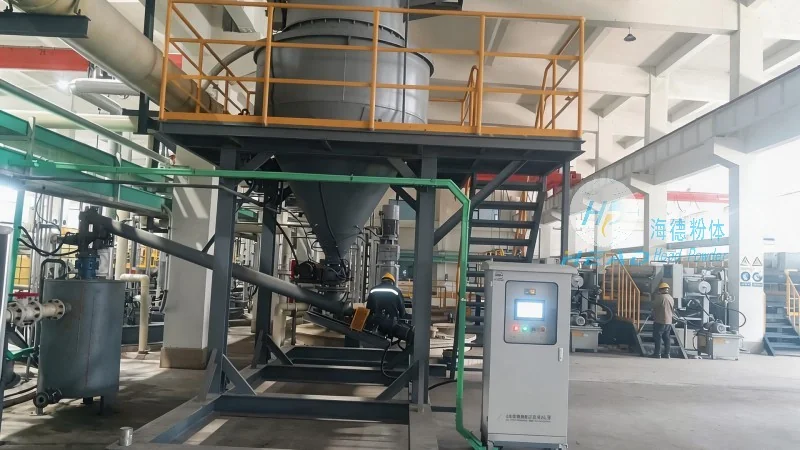
The Working Principle of Pneumatic Conveying Systems
At the core of dust material pneumatic conveying systems is the use of air to transport particles. The process typically involves a few key components: a material feed hopper, a conveying line (often made of metal or flexible tubing), a fan or blower to generate airflow, and a discharge point. The system operates by creating a pressure differential—either by blowing air into the line (positive pressure) or by creating a vacuum (negative pressure). When the material is introduced into the system, it is entrained by the moving air and carried through the pipeline to the destination. The fan or blower provides the necessary force to overcome friction losses and lift the material against gravity if needed. The design of the system, including the type of fan, the diameter of the conveying line, and the layout of the pipeline, significantly impacts the system's performance and efficiency.
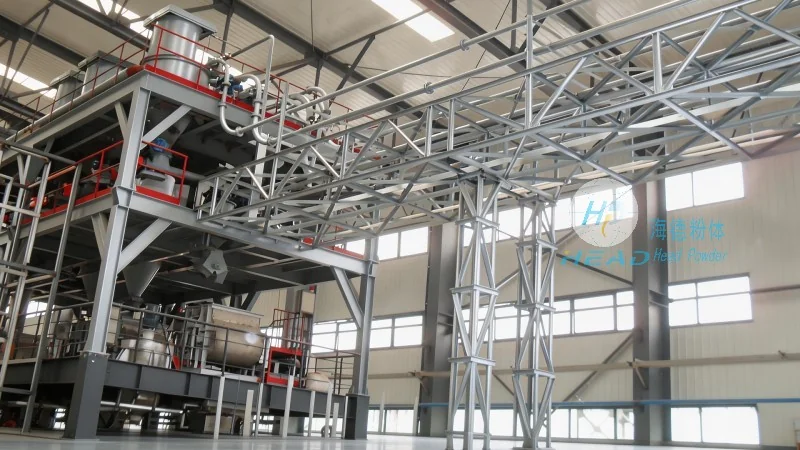
Key Features and Advantages of Dust Material Pneumatic Conveying Systems
Several distinct features make pneumatic conveying systems suitable for handling dust and fine materials. First, they offer a closed system, which minimizes dust emissions and prevents contamination from external sources. This is particularly important in industries like pharmaceuticals, food processing, and chemical manufacturing where product purity is critical. Second, these systems can handle a wide range of materials, from fine powders to coarse granules, with minimal degradation. The gentle handling reduces particle breakage and agglomeration, preserving the material's quality. Third, pneumatic conveying systems are flexible in terms of layout, allowing for vertical, horizontal, or mixed (vertical and horizontal) configurations. This adaptability makes them suitable for complex plant layouts and space constraints. Additionally, they can transport materials over longer distances compared to other bulk handling methods, such as belt conveyors, without the need for multiple transfer points. The systems also provide better control over material flow, enabling precise dosing and regulation of material delivery to downstream processes.
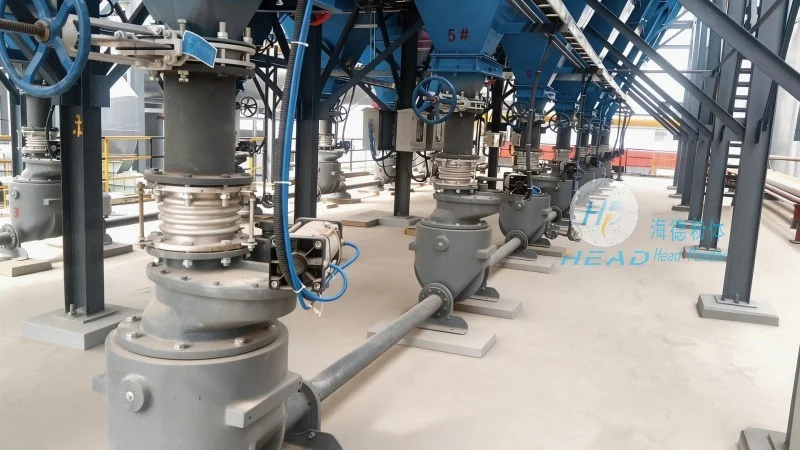
Applications and Industries Utilizing Pneumatic Conveying
Pneumatic conveying systems are widely used across various industries due to their versatility and efficiency. In the chemical industry, they are employed to transport powders like cement, plastics, and pigments. The food and beverage sector uses them for handling ingredients such as flour, sugar, and spices, ensuring hygiene and preventing cross-contamination. The pharmaceutical industry relies on these systems for transporting active pharmaceutical ingredients (APIs) and other fine powders, where contamination control is paramount. In the mining and minerals sector, pneumatic conveyors are used to transport ore and other bulk materials from processing plants to storage or further processing facilities. The ability to handle abrasive and corrosive materials makes these systems suitable for harsh environments in mining operations. Overall, the adaptability and efficiency of pneumatic conveying systems make them a preferred choice for industries requiring reliable and clean material handling solutions.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer of pneumatic conveying systems, specializes in providing customized solutions for dust and material handling needs. With a strong focus on innovation and quality, the company has developed advanced systems that meet the demands of various industries. HeadPowder's products are designed to ensure efficient material transport while maintaining high standards of safety and environmental compliance. The company's expertise in system design, manufacturing, and installation ensures that clients receive tailored solutions that address their specific operational requirements. Based in Shandong, China, HeadPowder leverages local manufacturing capabilities to deliver high-quality equipment at competitive prices, supporting global clients with reliable and durable pneumatic conveying systems.




