Flower bio-material conveying systems are essential in the horticultural and agricultural sectors, designed to efficiently transport organic materials such as flower petals, stems, and other plant byproducts. These systems are engineered to handle delicate biological materials while maintaining optimal conditions for preservation and processing. The technology behind these conveyors combines mechanical precision with environmental considerations, making them a critical component in modern flower processing facilities.
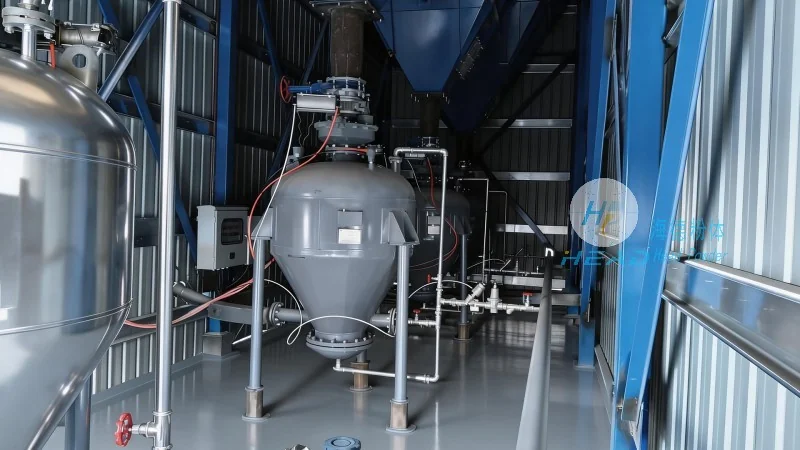
Working Principle of Flower Bio-Material Conveying
The core working principle of flower bio-material conveyors involves a series of specialized components working in tandem to move materials from one location to another. The process typically begins with material loading, where flowers or plant parts are placed into a hopper or feeding mechanism. From there, the material is transported through a conveyor system, often using gentle, low-friction surfaces to prevent damage to the delicate biological components. Many systems employ air-assisted or vacuum technology to create a smooth, continuous flow, minimizing mechanical stress on the flowers. The conveyor may include adjustable speed controls and directional changes, allowing for precise positioning of the material as it moves through the processing line. At the end of the conveyor, the material is discharged into a collection container or further processing unit. This entire process is designed to be gentle yet efficient, ensuring that the bio-materials retain their quality and integrity throughout the conveying operation.
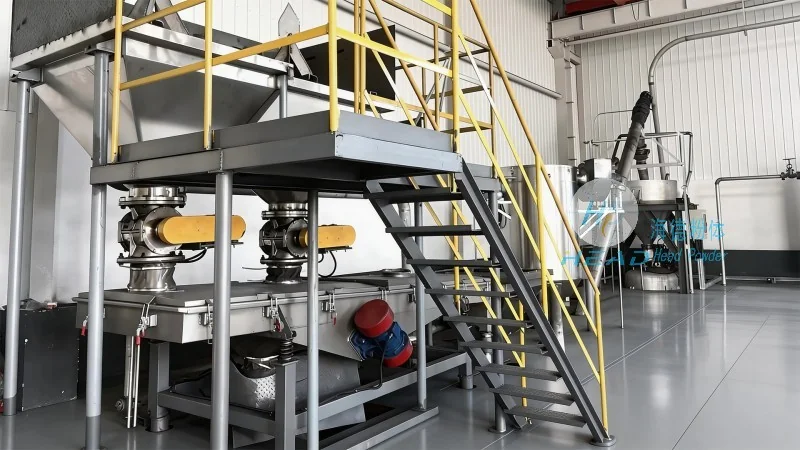
Key Characteristics of Flower Bio-Material Conveying Systems
Flower bio-material conveying systems are characterized by several key features that distinguish them from conventional industrial conveyors. First, the materials used in the construction of the conveyor components are non-toxic and food-grade certified, ensuring that they do not contaminate the organic materials being transported. The conveyor surfaces are often lined with soft, flexible materials like rubber or silicone, which provide a cushioning effect and prevent bruising or crushing of the flowers. Additionally, the systems are equipped with temperature and humidity control features, as many flower species are sensitive to environmental changes. This helps maintain the freshness and quality of the bio-materials during transport. Another important characteristic is the system's ability to handle a wide variety of flower types and sizes, from small blooms to large stems, without requiring frequent adjustments. The design also incorporates easy cleaning and maintenance features, which are crucial for hygiene in food and flower processing environments. Finally, the energy efficiency of these conveyors is a notable characteristic, with many models using variable frequency drives to adjust power consumption based on the load and speed requirements.
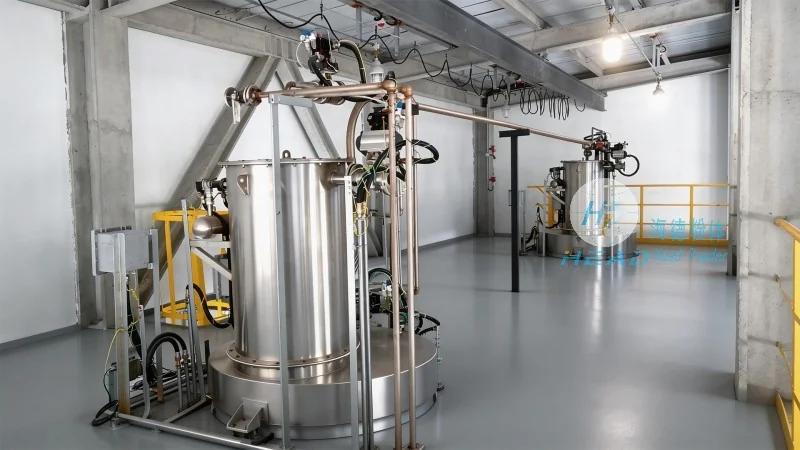
Applications and Benefits in the Flower Industry
Flower bio-material conveying systems are widely used in various stages of flower processing, from harvesting and sorting to packaging and distribution. In the harvesting phase, these systems help collect freshly picked flowers from fields or greenhouses and transport them to processing centers without damage. During sorting, the conveyors can be used to separate different types of flowers or remove damaged parts, improving the overall quality of the final product. In the packaging stage, the systems efficiently move flowers into containers or wrapping materials, ensuring that they are arranged neatly and securely for shipping. The benefits of using these systems extend beyond just efficiency; they also contribute to cost savings by reducing material waste and labor costs associated with manual handling. Furthermore, the gentle handling of the flowers helps maintain their market value, as customers often prefer fresh and undamaged flowers. The systems also support sustainable practices by minimizing the environmental impact of flower transportation, as they reduce the need for excessive water or chemical treatments during the conveying process.
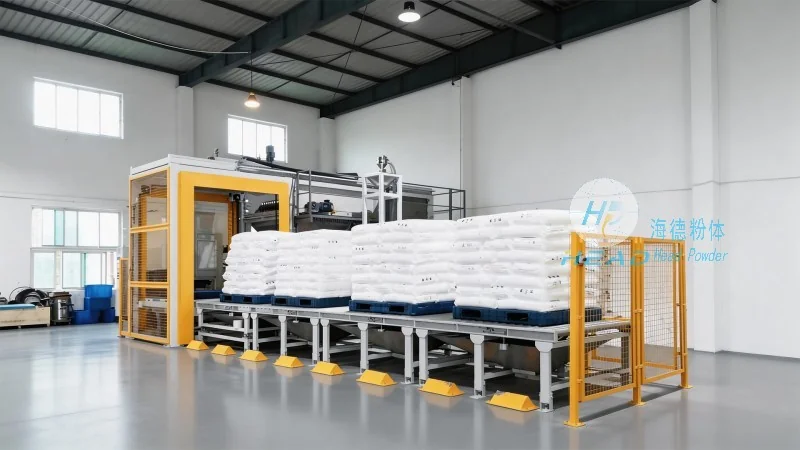
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer of specialized conveying equipment, has been at the forefront of developing advanced flower bio-material conveying systems. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the horticultural industry. HeadPowder's products are designed to meet the specific needs of flower processing facilities, offering customizable solutions that enhance operational efficiency and product quality. The company's headquarters is located in Shandong, China, where it has a dedicated team of engineers and technicians who work closely with clients to understand their unique requirements. HeadPowder's commitment to quality is reflected in its adherence to international standards and rigorous testing protocols, ensuring that each conveyor system meets the highest performance and safety criteria. The company also provides comprehensive after-sales support, including maintenance services and technical assistance, to help clients maximize the lifespan and effectiveness of their equipment. By combining expertise in mechanical engineering with a deep understanding of the flower industry, HeadPowder continues to deliver reliable and efficient solutions that help businesses thrive in a competitive market.




