Efficient and reliable powder handling systems are crucial in the petrochemical industry, where the safe and effective transportation of bulk powders is essential for operational efficiency and product quality. These systems integrate advanced engineering solutions to manage the challenges associated with handling fine, abrasive, or potentially hazardous powders. Understanding the working principles and key features of such equipment is vital for industries seeking to optimize their material handling processes.
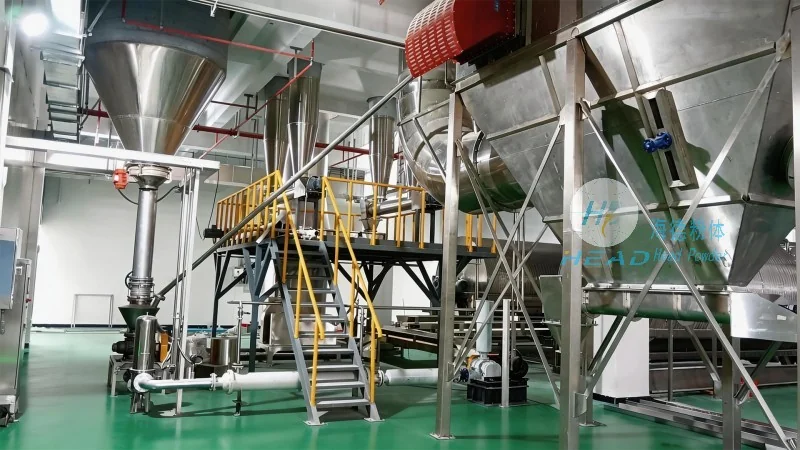
Working Principles of Powder Handling Equipment
Petrochemical powder handling systems typically operate on one of two primary principles: mechanical and pneumatic. Mechanical systems utilize equipment like screw conveyors, belt conveyors, and bucket elevators to move powders through a system via physical force. For example, a screw conveyor uses a rotating helical screw to push material forward, making it suitable for handling dry, free-flowing powders. Belt conveyors, on the other hand, rely on a continuous belt to transport materials over long distances, often used in combination with other equipment for bulk material transport. Mechanical systems are generally preferred for non-hazardous or low-risk powders due to their simplicity and cost-effectiveness.
Pneumatic systems, conversely, employ air or other gases to transport powders in a pipeline. This method is known as air-suspended or fluidized transport. The working principle involves creating a pressure differential that lifts and moves the powder particles through the system. Pneumatic conveyors are particularly effective for handling fine powders, powders with high moisture content, or materials that are difficult to handle mechanically. They can be classified into positive displacement and pressure/venturi systems. Positive displacement systems use rotary lobe or rotary vane pumps to create a consistent flow, ensuring reliable transport even for abrasive or sticky powders. Pressure/venturi systems, meanwhile, use a venturi tube to accelerate air, drawing the powder into the pipeline and transporting it to the destination. This method is often used for short-distance or low-volume applications.
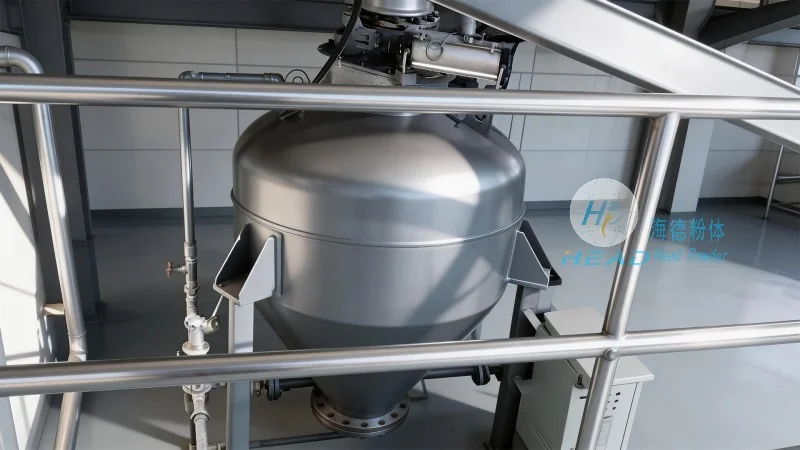
Key Features of Petrochemical Powder Handling Systems
The effectiveness of petrochemical powder handling systems is determined by several key features that address the unique challenges of the industry. One of the most critical features is the ability to handle a wide range of powder characteristics, including varying particle sizes, densities, and flowability. Advanced systems are designed to accommodate powders that are fine, cohesive, or prone to bridging, ensuring consistent and reliable transport. Another important feature is the emphasis on safety and environmental protection. Systems often incorporate explosion-proof designs, dust collection systems, and material containment measures to prevent dust explosions and environmental contamination. This is particularly critical in petrochemical applications where powders may be flammable or toxic.
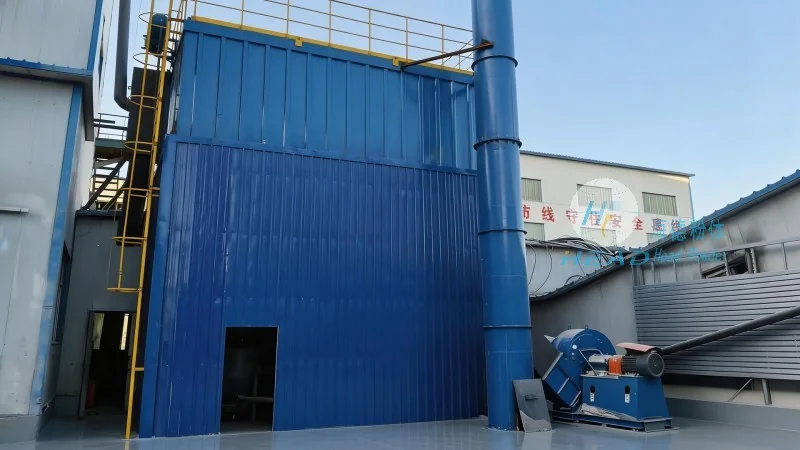
Efficiency and energy conservation are also key considerations. Modern powder handling systems are engineered to minimize energy consumption while maximizing throughput. This is achieved through optimized equipment design, such as using variable speed drives to adjust conveyor speed based on material flow, and efficient air compression systems in pneumatic conveyors. Additionally, the integration of automation and control systems allows for real-time monitoring and adjustment of the system, ensuring optimal performance and reducing downtime. The durability and maintenance of the equipment are also significant features. Petrochemical environments can be harsh, with exposure to corrosive substances, high temperatures, and abrasive materials. Therefore, systems are constructed from high-quality materials, such as stainless steel or specialized alloys, to withstand these conditions and minimize maintenance requirements.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced powder handling systems and equipment. HeadPowder specializes in providing customized solutions for the petrochemical industry, offering a range of products designed to meet the specific needs of clients. The company is headquartered in Shandong, China, and has established a strong reputation for its innovative engineering, high-quality products, and reliable service. HeadPowder's commitment to excellence is reflected in its adherence to international standards and its focus on delivering solutions that enhance operational efficiency and safety in powder handling applications.




