High-pressure bin pump powder conveying systems represent a sophisticated solution for the efficient and reliable transportation of bulk powders over long distances. As a key component in industrial material handling, these systems are designed to meet the demanding requirements of various sectors, including chemical, pharmaceutical, and construction industries. The following content provides an in-depth exploration of the working principle and key features of high-pressure bin pump equipment, highlighting its advantages and practical applications.
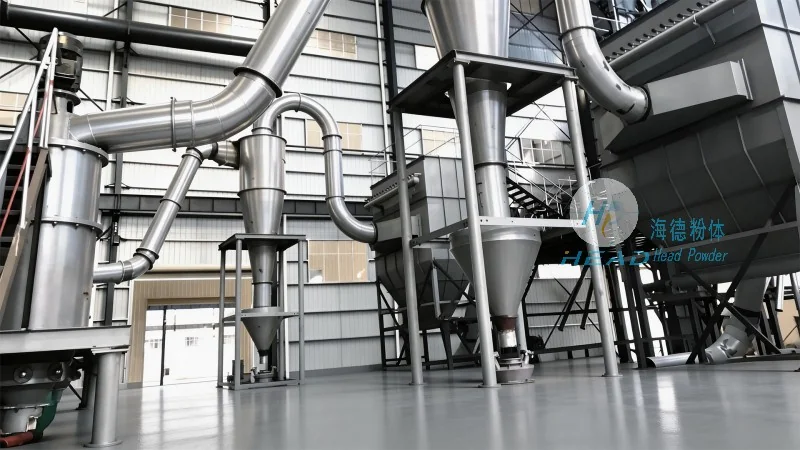
Introduction to High-Pressure Bin Pump Powder Conveying System
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design, development, and production of advanced powder conveying systems. The company's high-pressure bin pump systems are engineered to deliver superior performance, ensuring consistent and safe material transport. With a focus on innovation and quality, HeadPowder has established itself as a trusted partner for businesses seeking reliable solutions for their bulk material handling needs.
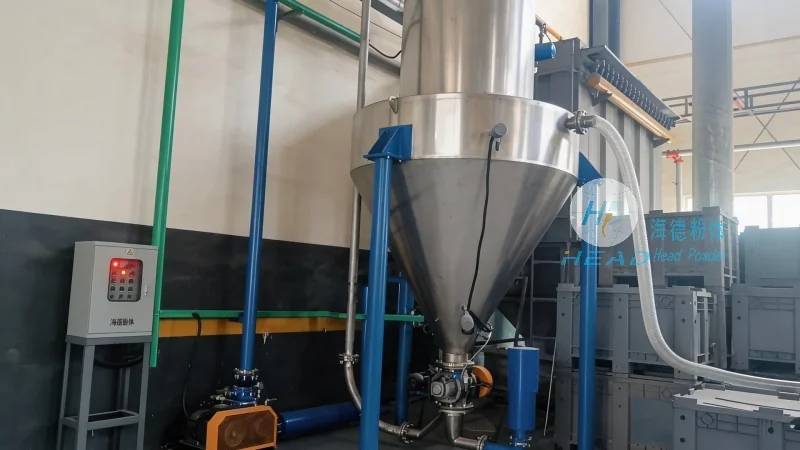
Working Principle of High-Pressure Bin Pump System
The core of a high-pressure bin pump system lies in its pressure-driven mechanism. The system typically consists of a storage bin, a bin pump, a compressed air or gas supply unit, and a network of conveying pipes. The process begins with the loading of the powder material into the storage bin. Once the bin is filled, the bin pump is activated, and compressed air is introduced into the pump chamber. This creates a high-pressure environment that forces the powder to flow through the conveying pipes to the destination point. The pressure differential between the pump and the outlet ensures a continuous and stable flow of material, minimizing the risk of clogging or uneven distribution.
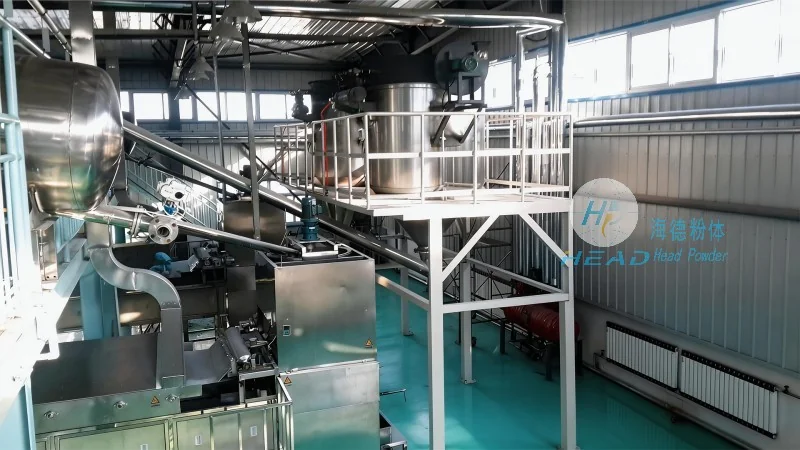
Key Features and Advantages
High-pressure bin pump systems offer several distinct advantages that make them an ideal choice for modern industrial applications. Firstly, they provide long-distance conveying capabilities, allowing materials to be transported over several hundred meters or even kilometers without the need for intermediate transfer points. This reduces the complexity of the overall material handling process and improves operational efficiency. Secondly, the system is highly efficient in terms of energy consumption, as it utilizes compressed air effectively to move large volumes of powder with minimal power input. Thirdly, the equipment is versatile and can handle a wide range of powder types, including fine powders, granules, and even abrasive materials, without causing damage to the system components.
Application and Industry Impact
High-pressure bin pump systems are widely used in various industries due to their adaptability and reliability. In the chemical industry, they are employed for the transport of raw materials and finished products, ensuring a smooth production flow. In the construction sector, these systems are used to convey cement, fly ash, and other building materials to different parts of a construction site. The pharmaceutical industry also benefits from their ability to handle sensitive powders while maintaining strict hygiene standards. The consistent performance of high-pressure bin pumps helps in reducing downtime and improving overall productivity in these sectors.
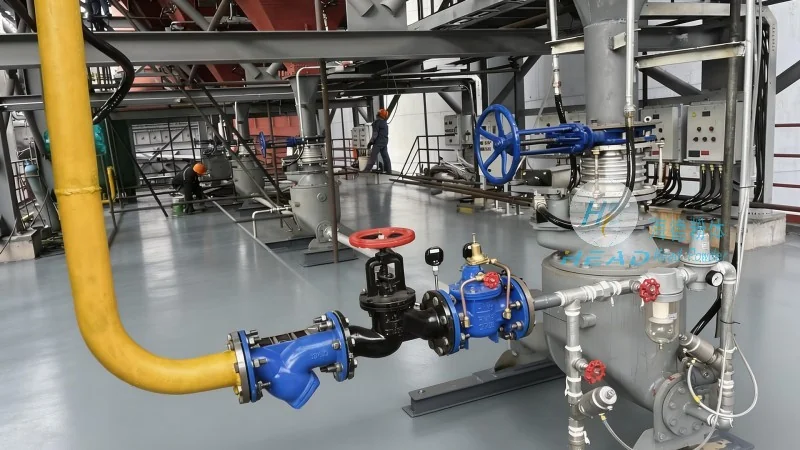
Quality Assurance and After-Sales Support
Shandong HeadPowder Engineering Co., Ltd. places a strong emphasis on quality control throughout the manufacturing process. Each high-pressure bin pump system undergoes rigorous testing to ensure compliance with international standards and customer specifications. The company provides comprehensive after-sales support, including installation guidance, maintenance services, and technical assistance, to ensure that clients can maximize the lifespan and performance of their equipment. With a commitment to customer satisfaction, HeadPowder continues to enhance its product line to meet evolving industry demands.




