

What is a Negative Pressure Dilute Phase Material Conveying Line? And What Are Its Design Principles
Understanding the negative pressure dilute phase material conveying line is crucial for industries that rely on efficient and reliable material handling solutions. This technology represents a sophisticated approach to transporting bulk materials through a pipeline using air as the primary medium. At the core of this system lies the principle of creating a negative pressure environment within the pipeline, which draws material particles into the air stream and transports them to the destination. The design principles behind such systems are intricate, balancing factors like air velocity, pipeline diameter, and material properties to ensure optimal performance.
Introduction to Negative Pressure Dilute Phase Conveying
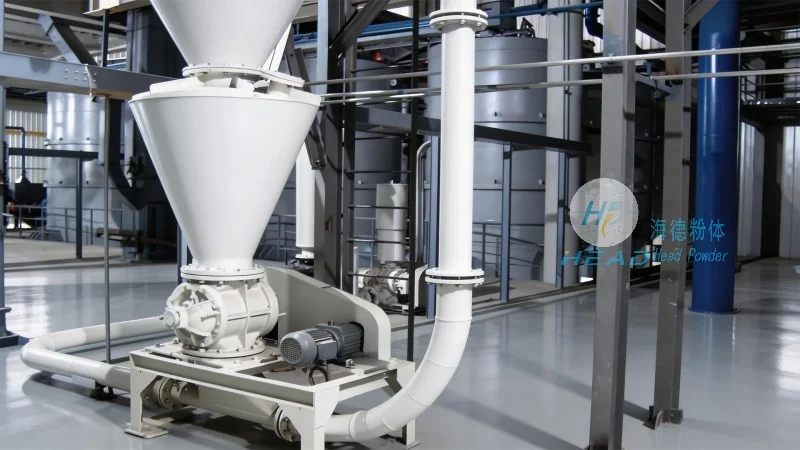
A negative pressure dilute phase material conveying line operates by generating a vacuum or reduced pressure in the conveying pipeline. This vacuum pulls material particles from the source hopper or storage area into the air stream. The material is then carried along with the air as a dilute suspension, moving through the pipeline to the discharge point. This method is particularly effective for transporting fine to medium-sized particles, such as powders, granules, and small pellets. The system is designed to minimize material degradation, maintain product integrity, and ensure consistent flow rates, making it a preferred choice in various industrial applications.
About HeadPowder: A Leading Provider in Material Handling Solutions
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a prominent company based in Shandong, China, specializing in the design, manufacturing, and installation of advanced material handling equipment. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner for businesses seeking efficient and reliable material conveying solutions. The company leverages years of industry experience to develop customized systems that meet the unique needs of each client, ensuring optimal performance and long-term durability. HeadPowder's expertise spans a wide range of material handling technologies, including pneumatic conveying systems, which are central to the negative pressure dilute phase conveying line.
Design Principles of Negative Pressure Dilute Phase Conveying Systems
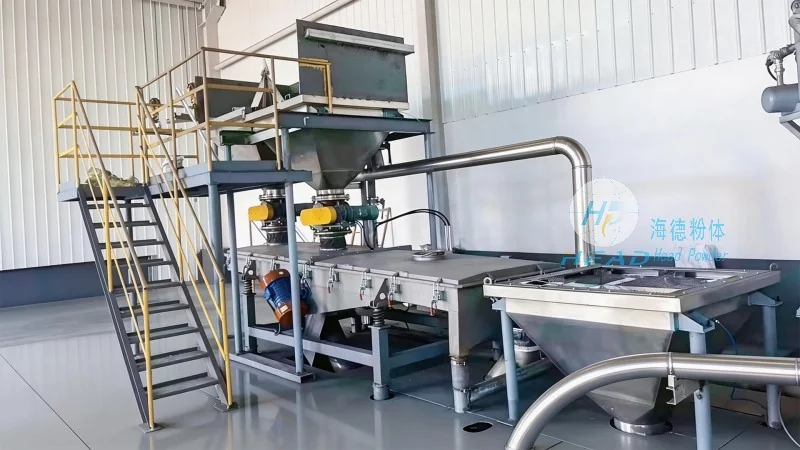
The design of a negative pressure dilute phase material conveying line involves several critical principles that ensure efficient material transport. First, the system must maintain a consistent negative pressure throughout the pipeline to create an effective suction force. This is achieved through carefully engineered components, such as vacuum pumps or fans, which generate the necessary air flow. The air velocity within the pipeline is a key parameter; it must be high enough to keep the material particles suspended but low enough to prevent excessive wear on the pipeline and components. The pipeline diameter is also critical, as it affects the air velocity and the overall capacity of the system. Proper sizing ensures that the material flows smoothly without clogging or causing pressure drops that could lead to system failure.
Another crucial design principle is the selection of appropriate materials for the pipeline and components. The conveying line must be constructed from materials that are resistant to the specific properties of the transported material, such as abrasiveness, moisture, or chemical compatibility. This prevents degradation of the pipeline over time and ensures the longevity of the system. Additionally, the system includes features like filter bags or cyclones at the discharge end to separate the material from the air stream, allowing for clean material recovery and air filtration. These components are essential for maintaining product purity and complying with environmental regulations.
Key Features and Benefits of Negative Pressure Dilute Phase Conveying
Negative pressure dilute phase material conveying lines offer several advantages that make them ideal for industrial applications. One of the primary benefits is the ability to transport materials over long distances with minimal energy consumption compared to other methods like belt conveyors or truck transport. The system is also highly flexible, as it can be easily integrated into existing facilities or adapted to new layouts. The enclosed pipeline design prevents dust emissions, making it a more environmentally friendly option compared to open systems. Furthermore, the system allows for precise control over material flow rates, ensuring consistent production processes and reducing waste. The negative pressure operation also minimizes the risk of material spillage or contamination, which is critical in industries where product purity is paramount, such as pharmaceuticals, food processing, and chemical manufacturing.
Applications and Industries Served by Negative Pressure Dilute Phase Conveying
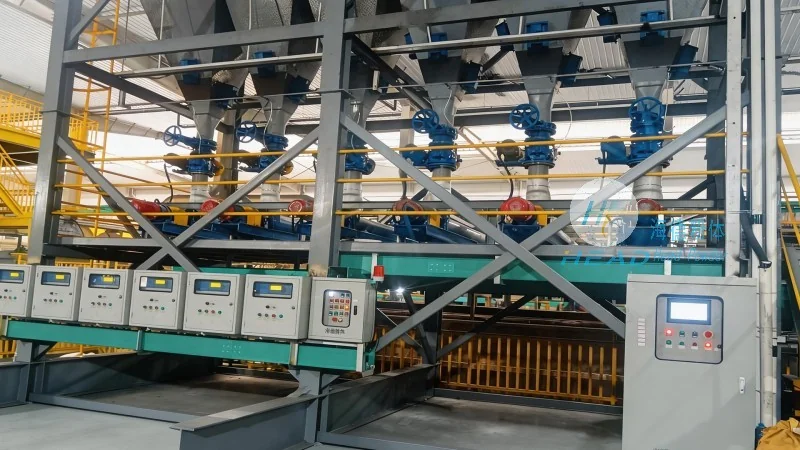
The negative pressure dilute phase material conveying line is widely used across various industries due to its versatility and efficiency. In the chemical industry, it is used to transport powders and granules for processing and storage. The food and beverage industry benefits from its ability to handle ingredients like flour, sugar, and spices while maintaining hygiene standards. The pharmaceutical sector relies on this technology to transport active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring they remain uncontaminated and pure. Additionally, the system is used in the mining and mineral processing industry to transport ore and other bulk materials from processing plants to storage or shipping facilities. The flexibility of the system allows it to adapt to different material types and processing requirements, making it a valuable asset for businesses in these sectors.
Conclusion: The Role of HeadPowder in Advancing Material Handling Technology
In conclusion, the negative pressure dilute phase material conveying line is a sophisticated and efficient solution for bulk material transport, with design principles that prioritize performance, reliability, and environmental responsibility. HeadPowder, with its expertise and commitment to quality, plays a vital role in providing these advanced systems to industries worldwide. By understanding the core design principles and benefits of such systems, businesses can make informed decisions about implementing effective material handling solutions that enhance productivity and operational efficiency. As industries continue to evolve, the demand for reliable and innovative material conveying technologies will remain high, and companies like HeadPowder will continue to lead the way in developing solutions that meet these evolving needs.