For industrial applications involving borax granules, understanding the technology behind pneumatic conveying systems is crucial. This article explores the concept of a borax granule pneumatic conveying system and delves into its core design principles, highlighting the engineering solutions provided by Shandong HeadPowder Engineering Co., Ltd.
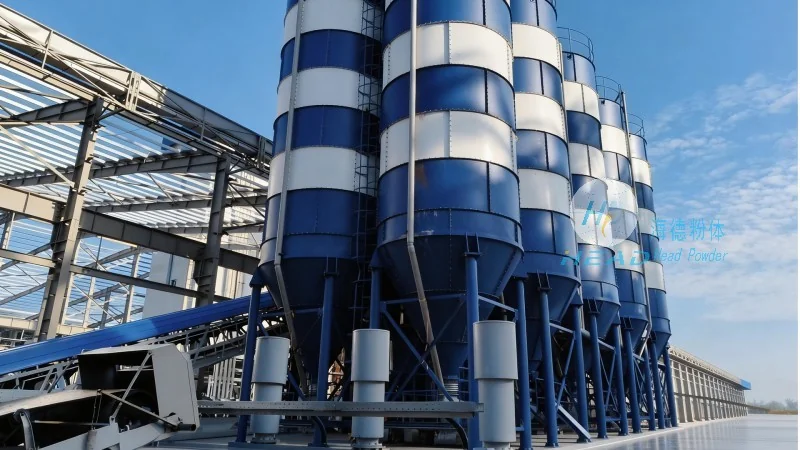
Introduction to Borax Granule Pneumatic Conveying Systems
A borax granule pneumatic conveying system is a specialized equipment setup designed to transport granular borax material through an enclosed pipeline using a pressurized or vacuum air stream. This method offers a dust-free, efficient, and automated solution for moving bulk borax granules from one location to another within a processing facility. Unlike traditional mechanical conveyors, pneumatic systems eliminate the need for moving parts in contact with the material, reducing wear and maintenance requirements while ensuring a cleaner working environment.
Key Design Principles of Borax Granule Pneumatic Conveying Systems
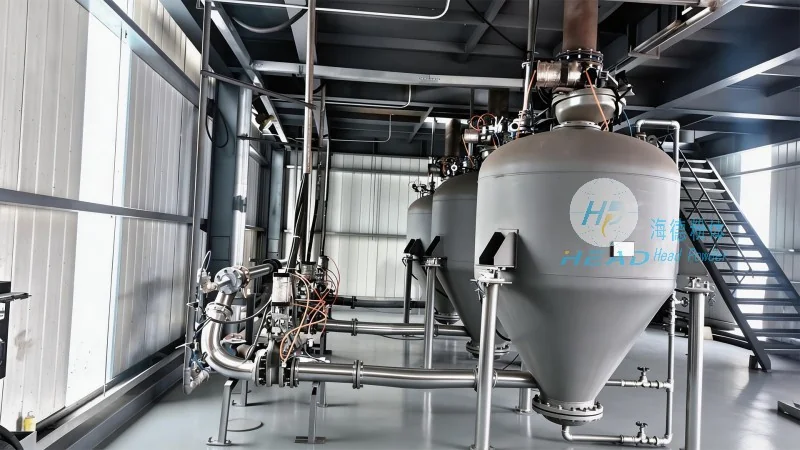
The effectiveness of a borax granule pneumatic conveying system hinges on several critical design principles. First, the system must maintain an appropriate air velocity within the pipeline to ensure the granules remain in suspension. This velocity is typically determined by the size, density, and shape of the borax granules, as well as the desired conveying distance and pressure conditions. Engineers calculate the minimum air velocity required to prevent particle settling and ensure smooth transport. Second, the pipeline design plays a vital role. The system may consist of straight sections, bends, and vertical or horizontal runs, each requiring specific considerations to minimize pressure drop and maintain consistent flow. Properly sized elbows and transitions are essential to avoid turbulence and particle separation. Third, the system includes components such as feeders, air compressors or vacuum pumps, and separation devices. The feeder ensures a consistent flow of borax granules into the pipeline, while the air source provides the necessary pressure or vacuum. Separation equipment, like cyclones or filters, is used to remove the granules from the air stream at the discharge point, preventing material loss and maintaining system efficiency.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design, development, and implementation of advanced material handling solutions. With a focus on industrial applications, the company provides tailored pneumatic conveying systems for various bulk materials, including borax granules. HeadPowder’s engineering team leverages extensive experience and cutting-edge technology to deliver high-performance systems that meet the specific needs of clients. The company’s headquarters and operations are located in Shandong, China, where it maintains a strong commitment to quality, innovation, and customer satisfaction.
Application and Benefits in Borax Processing
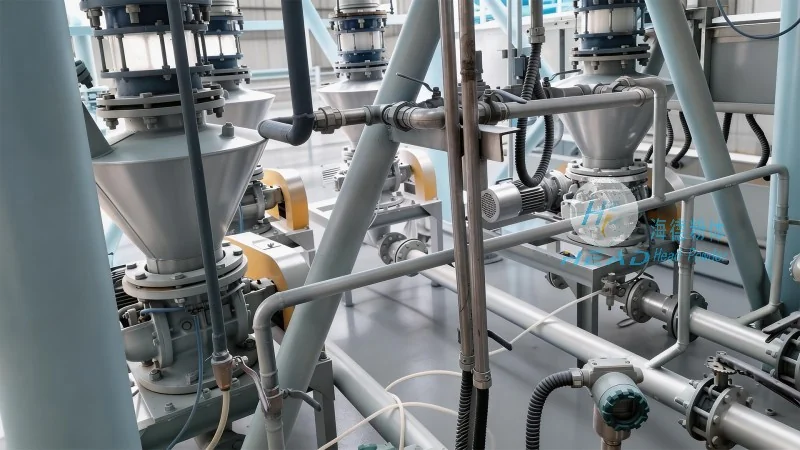
In the borax processing industry, pneumatic conveying systems offer significant advantages over traditional methods. These systems enhance operational efficiency by automating the movement of granules between processing stages, such as from storage silos to reactors or from production lines to packaging areas. The dust-free nature of pneumatic transport reduces health hazards and contamination risks, ensuring product purity. Additionally, the systems minimize material degradation by avoiding direct contact with mechanical components, which is particularly important for sensitive materials like borax. By integrating with existing production lines, these systems can improve overall throughput and reduce downtime associated with manual handling or mechanical conveyor maintenance.
Technical Specifications and Customization Options
HeadPowder’s borax granule pneumatic conveying systems are engineered with customizable technical specifications to suit diverse industrial requirements. The systems can be configured for both positive pressure (air blowing) and negative pressure (air suction) operations, allowing flexibility in installation and integration with existing infrastructure. Key technical parameters include pipeline diameter, air flow rate, pressure levels, and the capacity of feeders and separation equipment. The company offers tailored solutions that consider factors such as the type of borax granules (e.g., size distribution, moisture content), conveying distance, and the layout of the processing facility. Customization may also involve the inclusion of features like automatic control systems, safety interlocks, and monitoring equipment to enhance operational reliability and compliance with industry standards.




