Slurry pneumatic conveying systems represent a critical technology in material handling, particularly for transporting slurries that combine solid particles with liquid. These systems are essential in various industrial sectors, including mining, chemical processing, and food production, where efficient and reliable material transport is paramount. The classification and application of such systems are vital for optimizing operational efficiency and ensuring the integrity of the conveyed materials.
Classification of Slurry Pneumatic Conveying Systems
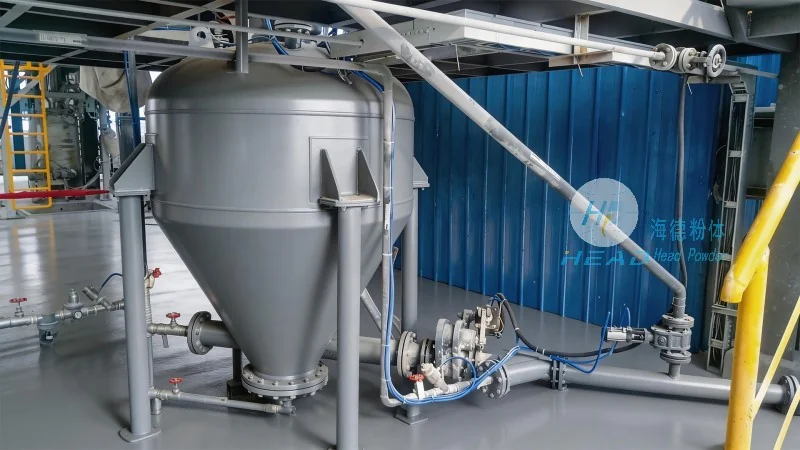
Slurry pneumatic conveying systems can be broadly categorized based on the principles of operation and the characteristics of the materials being transported. The primary classifications include positive pressure systems, negative pressure (vacuum) systems, and hybrid systems. Positive pressure systems use compressed air to push the slurry through the pipeline, making them suitable for long-distance and high-capacity transport. Negative pressure systems, on the other hand, use suction to draw the slurry into the system, which is ideal for applications requiring minimal dust emission and for transporting materials from multiple sources. Hybrid systems combine elements of both positive and negative pressure, offering flexibility in handling diverse material types and operational conditions.
Key Components and Operational Principles
Understanding the core components and operational principles of slurry pneumatic conveying systems is essential for their effective application. The system typically consists of a slurry feed hopper, a pump or compressor for pressurization, a pipeline network, and a receiver or discharge unit. The feed hopper ensures a consistent supply of slurry, while the pump or compressor generates the necessary pressure to move the material through the pipeline. The pipeline design, including diameter, length, and bends, significantly impacts the system's performance and efficiency. Proper selection of these components is crucial to avoid issues such as clogging, pressure loss, and material degradation.
Applications in Industrial Sectors
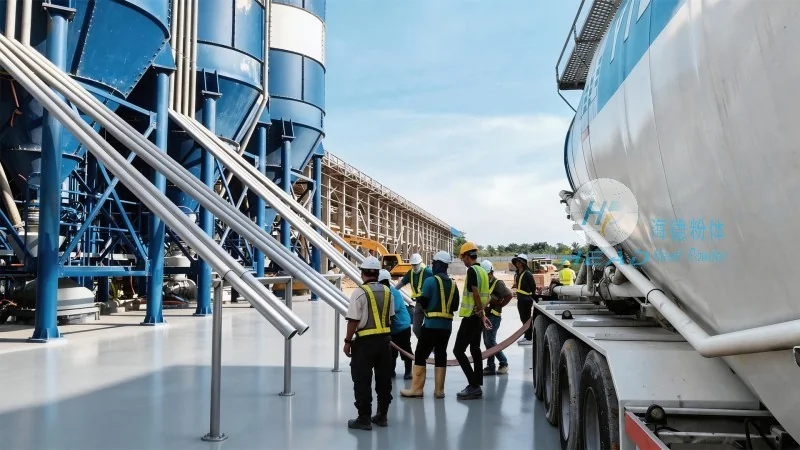
Slurry pneumatic conveying systems find extensive applications across multiple industrial sectors. In the mining industry, they are used for transporting ore slurries from processing plants to storage facilities or for transporting tailings. The chemical industry utilizes these systems for handling slurries containing chemicals, catalysts, or other reactive materials, ensuring safe and efficient transport. In the food and beverage industry, slurry pneumatic conveying is employed for transporting slurries like fruit purees, dairy products, or starches, maintaining product quality and hygiene. Additionally, in the construction industry, these systems are used for transporting concrete mixtures or other construction materials, facilitating efficient on-site material handling.
Advantages and Challenges of Slurry Pneumatic Conveying
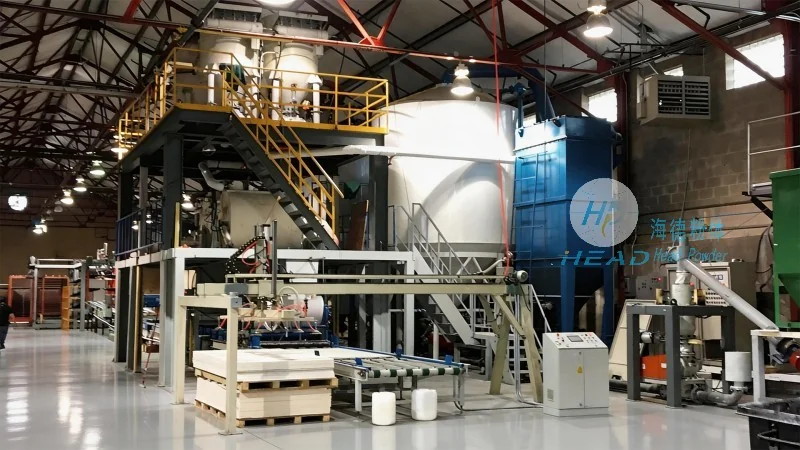
While slurry pneumatic conveying systems offer numerous advantages, such as reduced labor costs, minimized material handling losses, and the ability to transport materials over long distances, they also present specific challenges. One of the main challenges is the potential for pipeline clogging due to the presence of solid particles, which can be mitigated through proper system design and maintenance. Another challenge is the need for regular cleaning and maintenance to prevent material buildup and ensure system longevity. Additionally, the energy consumption of these systems can be significant, particularly for long-distance transport, requiring careful consideration of operational costs.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of slurry pneumatic conveying systems and related engineering solutions. With a strong focus on innovation and customer satisfaction, the company specializes in designing, manufacturing, and installing customized slurry conveying systems tailored to the specific needs of its clients. HeadPowder's expertise lies in understanding the unique challenges of slurry transport and developing solutions that optimize performance, reliability, and cost-effectiveness. The company's commitment to quality and technical excellence has established it as a trusted partner in the industry, serving clients across various sectors with high-quality, efficient slurry conveying systems.




