Bentonite powder, a critical material in numerous industrial sectors, demands efficient and reliable handling solutions to sustain smooth production workflows. The pneumatic conveying equipment engineered by Shandong HeadPowder Engineering Co., Ltd. addresses these requirements by delivering a sophisticated system for transporting bentonite powder between locations. This equipment is designed to preserve the powder's quality while minimizing material loss and operational interruptions.
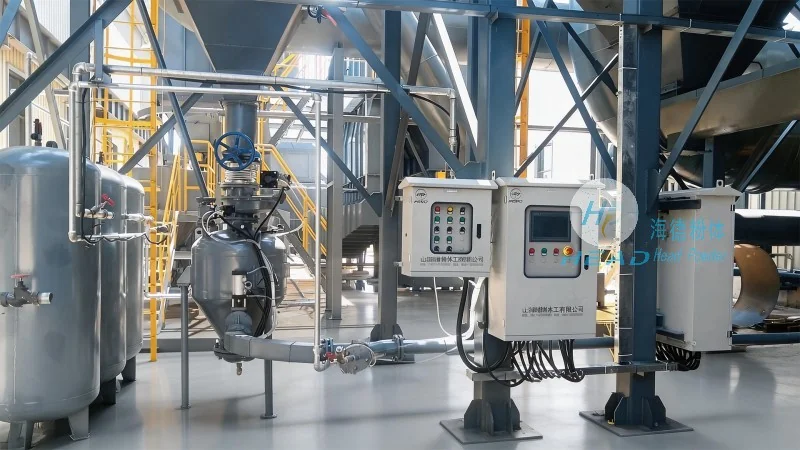
Components of the Pneumatic Conveying System
The pneumatic conveying system for bentonite powder comprises several essential components that operate in unison to achieve effective material transport. These components include the hopper, which stores the bentonite powder; the feeder, responsible for regulating the powder flow rate into the system; the air compressor, which generates the necessary air pressure to move the powder; the conveying pipeline, which transports the powder through the system; and the receiver, where the powder is deposited at the destination. Each component is meticulously engineered to ensure optimal performance and durability under industrial conditions.
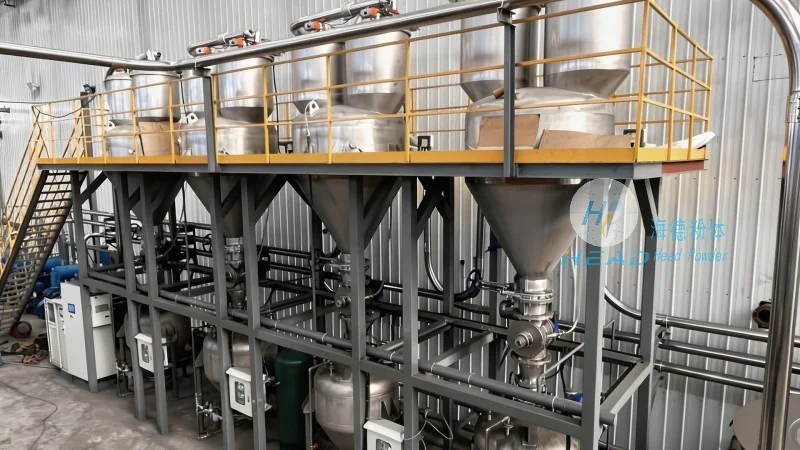
Working Principle of the Pneumatic Conveying Process
The operation of the bentonite powder pneumatic conveying equipment is grounded in the principle of air suspension, where powder particles are suspended in an air stream and transported through the pipeline. The process initiates when the feeder releases a controlled amount of bentonite powder into the hopper. The air compressor then generates a high-pressure air stream that is introduced into the conveying pipeline. As the air flows through the pipeline, it picks up the bentonite powder particles, forming a mixture of air and powder. This mixture travels through the pipeline to the receiver, where the air is separated from the powder, and the powder is collected in the receiver. The air is subsequently discharged back into the system or to the atmosphere, depending on the equipment's design.
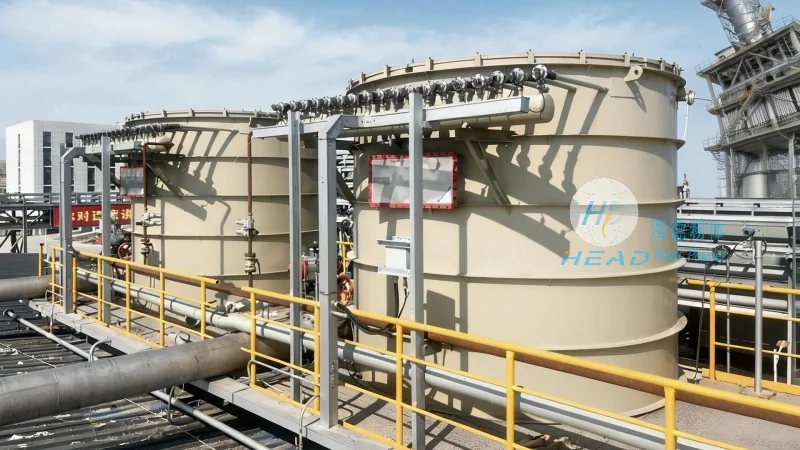
Operation Process of the Equipment
The operation process of the bentonite powder pneumatic conveying equipment involves sequential steps to ensure efficient and continuous material transport. First, the hopper is filled with bentonite powder, and the feeder is adjusted to the desired flow rate. The air compressor is then activated, and the system is pressurized to the required level. Once pressurized, the feeder begins releasing the powder into the system. The powder is conveyed through the pipeline to the receiver. The receiver is engineered to collect the powder and prevent leakage or spillage. The system is continuously monitored to maintain flow rate and pressure at optimal levels. Adjustments to the feeder or air compressor are made as needed to sustain desired performance.
Advantages of Using Pneumatic Conveying for Bentonite Powder
Employing pneumatic conveying equipment for bentonite powder handling offers several benefits. Firstly, the system enables long-distance transport without intermediate storage or handling, reducing contamination and loss risks. Secondly, the equipment is designed to preserve powder quality by minimizing exposure to air and moisture—critical for bentonite's sensitivity to environmental factors. Thirdly, the system is highly efficient, handling large volumes with minimal energy consumption. Finally, the equipment is user-friendly and low-maintenance, reducing specialized personnel needs and downtime.
Conclusion
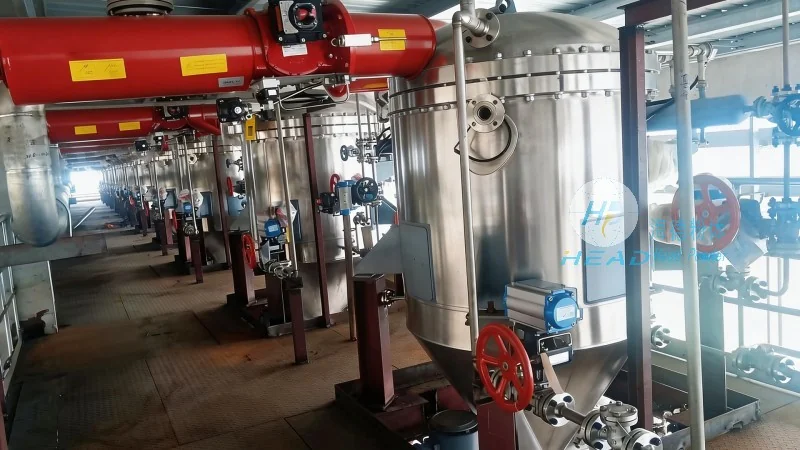
Shandong HeadPowder Engineering Co., Ltd. provides high-quality pneumatic conveying equipment for bentonite powder, tailored to meet diverse industrial application needs. The equipment is based on a proven air suspension principle and consists of carefully engineered components working in tandem for efficient material transport. The operation process is straightforward and adaptable to specific application requirements. Advantages include long-distance transport, minimal material loss, and efficient operation. By utilizing this equipment, industrial facilities can enhance production processes and maintain bentonite powder quality.




