HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of efficient coffee material conveying systems. These systems are engineered to handle the unique demands of coffee processing, ensuring optimal performance and reliability in various operational environments.
Understanding the Core Principles of Coffee Material Conveying Systems
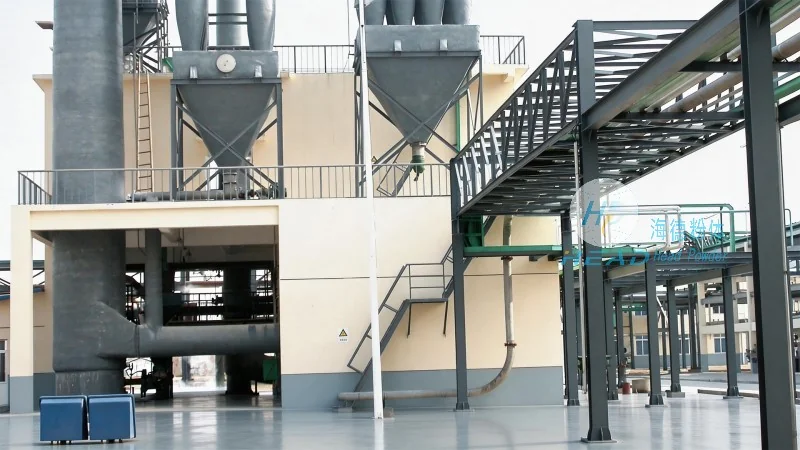
Coffee material conveying systems operate on fundamental principles that ensure the smooth and safe transport of coffee beans, grounds, and other related materials. The primary mechanism involves the use of specialized equipment such as conveyor belts, pneumatic conveyors, and gravity chutes, each tailored to the specific characteristics of coffee products. These systems are designed to maintain the integrity of the coffee materials, preventing damage or degradation during transport. The integration of advanced control systems allows for precise regulation of speed, direction, and flow, enhancing operational efficiency and reducing downtime.
Key Working Scene Characteristics of Coffee Material Conveying Systems
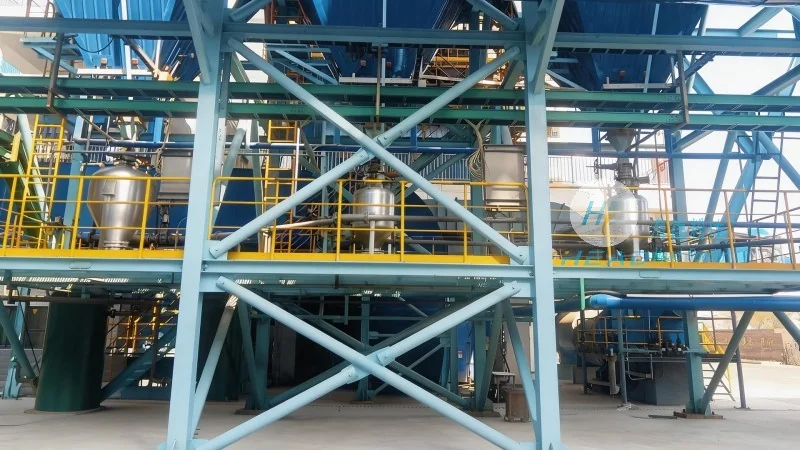
The working scene characteristics of coffee material conveying systems are shaped by the diverse applications within the coffee industry. In coffee roasting facilities, these systems facilitate the movement of raw coffee beans from storage to roasting machines, ensuring a continuous and controlled supply. During the grinding process, conveying systems transport ground coffee efficiently to packaging units, minimizing waste and maintaining product consistency. In large-scale coffee production plants, the systems often operate in conjunction with automated sorting and quality control equipment, creating a seamless workflow that enhances overall productivity. The adaptability of these systems to different coffee processing stages makes them essential components in modern coffee manufacturing operations.
Technical Advantages and Operational Efficiency
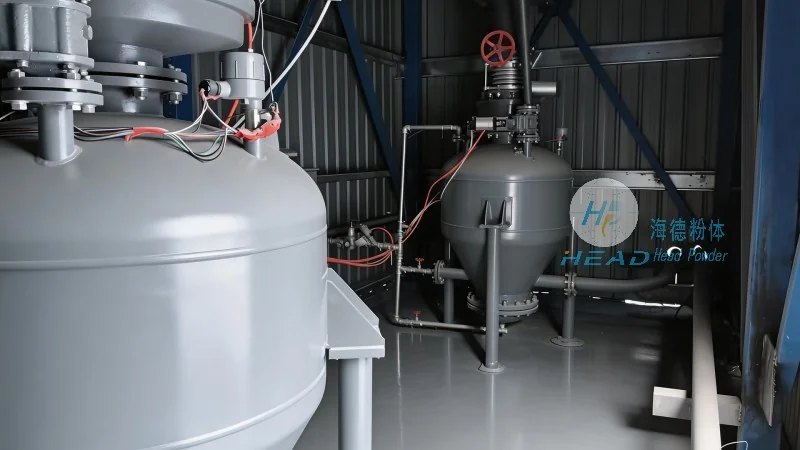
HeadPowder's coffee material conveying systems are equipped with several technical advantages that contribute to superior operational efficiency. The use of durable materials, such as food-grade stainless steel, ensures resistance to corrosion and easy cleaning, which is crucial in maintaining hygiene standards in coffee processing environments. Advanced sensors and monitoring systems provide real-time data on system performance, enabling proactive maintenance and reducing unexpected breakdowns. The modular design of the systems allows for easy integration with existing production lines, minimizing installation time and costs. Additionally, the energy-efficient operation of these systems helps in reducing operational costs while promoting sustainability in coffee production.
Customization and Application Flexibility
HeadPowder recognizes that coffee processing facilities have varying requirements, and thus, their conveying systems are customizable to meet specific needs. Whether it's handling different types of coffee beans, accommodating varying production volumes, or integrating with existing machinery, the systems can be tailored to fit the unique operational demands of each client. The company's engineering team works closely with clients to understand their specific challenges and develop solutions that enhance productivity and efficiency. This flexibility ensures that the coffee material conveying systems not only meet current needs but also adapt to future expansion and technological advancements in the coffee industry.
Conclusion
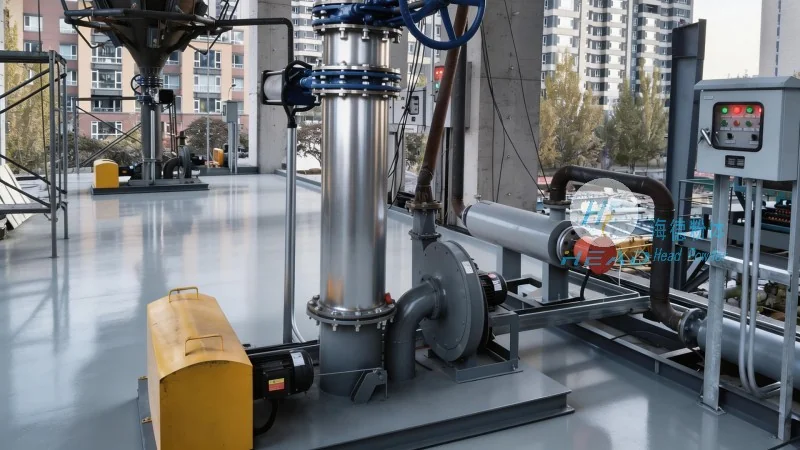
HeadPowder's coffee material conveying systems represent a sophisticated solution for the efficient handling of coffee materials in various working environments. By adhering to the core principles of reliability, efficiency, and adaptability, these systems contribute significantly to the productivity and quality of coffee production. As a trusted manufacturer based in Shandong, China, HeadPowder continues to innovate and provide high-quality conveying solutions that meet the evolving needs of the coffee industry.




