Working Principle and Features of Soap Granule Powder Pneumatic Conveying System
Release time:2026-09-18 02:01:28
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Understanding the operation and characteristics of a soap granule powder pneumatic conveying system is crucial for industries that handle such materials efficiently and safely. This article provides a detailed overview of how these systems function and the key attributes that define their performance.
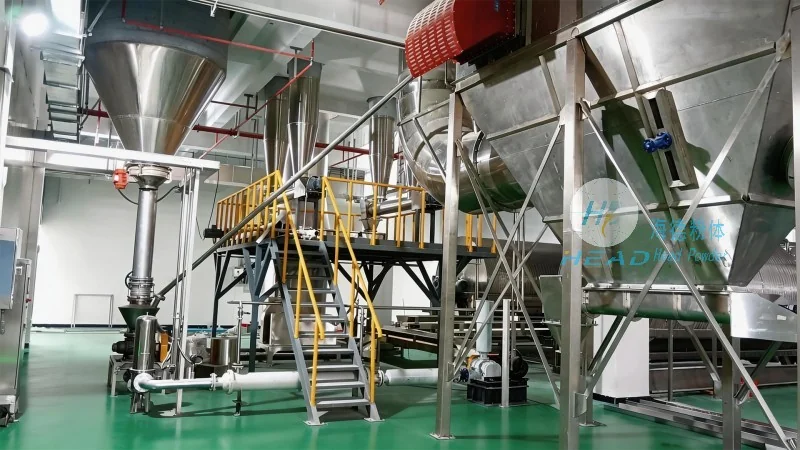
Overview of Pneumatic Conveying Technology for Soap Granules
Pneumatic conveying systems are designed to transport dry powders, such as soap granules, through a pipeline using air or other gases. The technology eliminates the need for mechanical components like belts or buckets, offering a more hygienic and flexible solution for material handling in manufacturing and processing facilities. The core of the system involves creating a pressure differential that moves the material from the source to the destination, ensuring minimal product degradation and contamination.
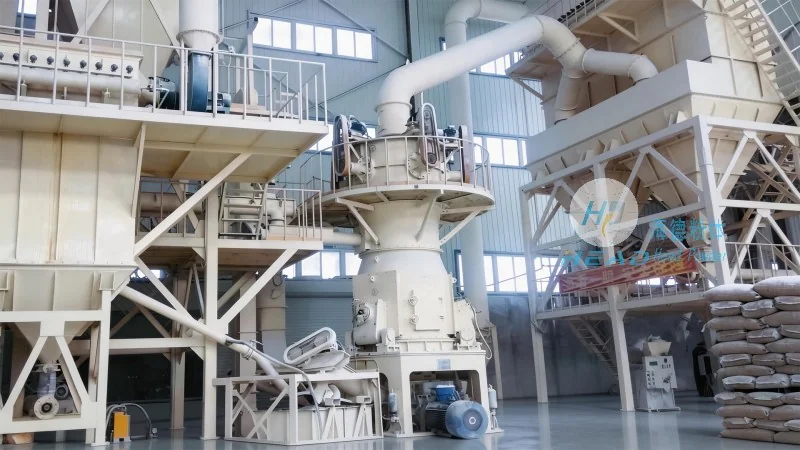
Working Principle of the Soap Granule Powder Pneumatic Conveying System
The working principle of a soap granule powder pneumatic conveying system relies on the generation of airflow within a closed pipeline. The system typically consists of a hopper, a conveyor line, and a receiver. The process begins when the soap granules are fed into the hopper. An air compressor then supplies compressed air, which is introduced into the conveyor line. The air velocity is carefully controlled to achieve a specific flow rate that lifts and transports the granules through the pipeline. The system may use either positive pressure (where air is pushed through the line) or negative pressure (where air is drawn out, creating a vacuum). For soap granules, positive pressure systems are often preferred due to their ability to handle abrasive materials and maintain consistent flow rates.
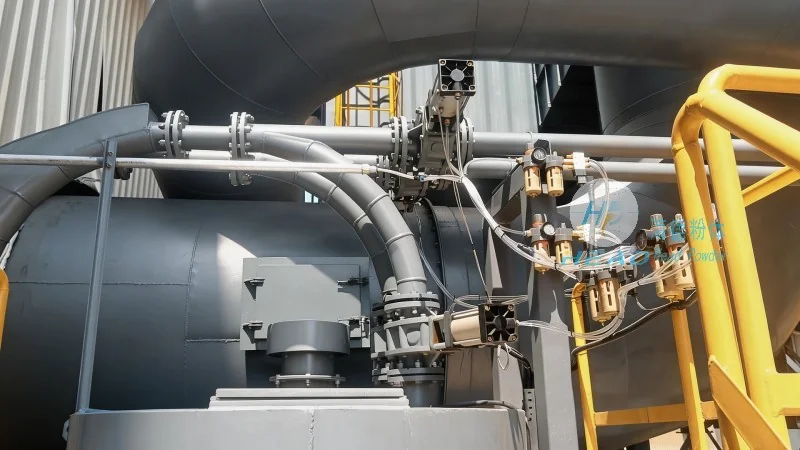
Key Features and Advantages of the System
The soap granule powder pneumatic conveying system offers several advantages that make it an ideal choice for handling delicate or hygienic materials like soap granules. First, it provides a completely enclosed and dust-free environment, which is essential for maintaining product quality and compliance with industry standards. Second, the system minimizes product contamination by eliminating direct human contact and preventing exposure to external elements. Third, it offers high efficiency in material transport, with the ability to handle large volumes of granules over long distances with minimal energy consumption. Additionally, the system is highly flexible, allowing for easy integration with existing production lines and adaptability to varying production demands. The design also ensures low maintenance requirements, as there are fewer moving parts compared to traditional mechanical conveyors, reducing downtime and operational costs.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the manufacturer of this advanced pneumatic conveying system, is a leading company in the field of powder handling solutions. Based in Shandong, China, HeadPowder specializes in developing and supplying high-quality equipment for the chemical, pharmaceutical, and personal care industries. The company’s expertise lies in understanding the unique challenges of handling materials like soap granules, ensuring that their systems are tailored to meet the specific needs of each client. With a commitment to innovation and quality, HeadPowder provides reliable and efficient solutions that enhance productivity and safety in material handling processes.




