HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems. Among their portfolio is the negative pressure dilute phase powder conveying system, a technology that efficiently transports bulk powders over long distances with minimal energy consumption and operational complexity. This article delves into the working principle and key features of this system, highlighting its practical applications and benefits for various industries.
Understanding the Negative Pressure Dilute Phase Pneumatic Conveying System
The negative pressure dilute phase powder pneumatic conveying system operates on the principle of creating a vacuum or negative pressure in the conveying line to draw the powder material from the source to the destination. Unlike positive pressure systems that push air and material through the pipeline, negative pressure systems pull the material, which is often more energy-efficient for certain applications, especially when the material is sensitive to high pressure or when the conveying distance is moderate.
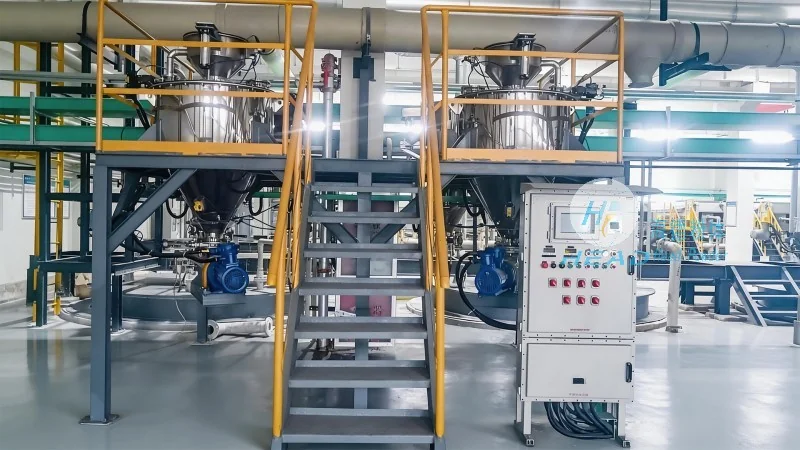
At its core, the system consists of several key components: a dust collector, a conveying line, a material hopper, and a control system. The material is first stored in the hopper, from which it is fed into the conveying line under the influence of the negative pressure created by the dust collector. The dust collector, typically equipped with a filter to capture fine particles, maintains the vacuum by continuously extracting air from the system. As the material is drawn into the line, it is suspended in the air stream and transported to the receiving hopper or silo at the destination.
Working Principle Explained in Detail
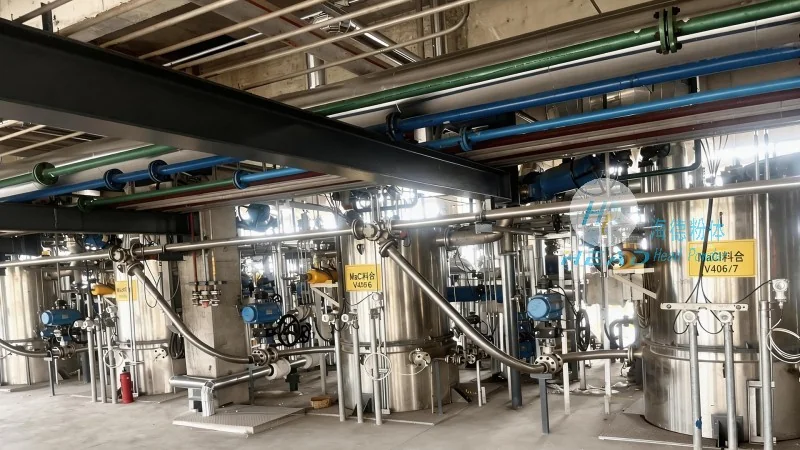
The operation of the negative pressure dilute phase system can be broken down into several sequential steps. First, the material is loaded into the source hopper. A feeder, often a rotary valve or a screw feeder, regulates the flow of material into the conveying line. Simultaneously, the dust collector starts operating, creating a negative pressure within the pipeline. This vacuum pulls the material and the air mixture from the hopper into the line. The material is then suspended in the air stream, which moves it along the pipeline at a consistent velocity. The receiving hopper at the end of the line collects the material as the air continues to flow through the system, eventually being filtered and discharged by the dust collector.
Key Features and Advantages of the System
Several distinct features make the negative pressure dilute phase powder conveying system an attractive solution for bulk material handling. One of the primary advantages is its energy efficiency, as it operates under lower pressure compared to positive pressure systems, reducing operational costs. The system is also suitable for transporting materials that are sensitive to high pressure or temperature, as the negative pressure environment minimizes stress on the material particles.
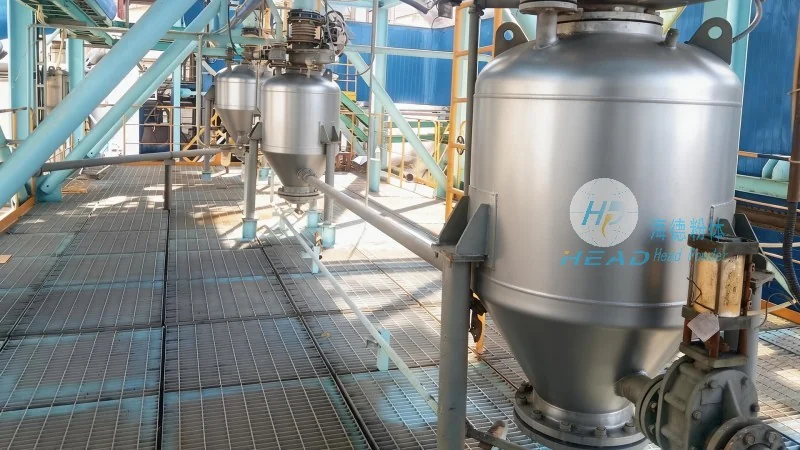
Another notable feature is its ability to handle a wide range of powder types, from fine powders to bulk materials, with minimal segregation or degradation. The dilute phase operation ensures that the material is well-mixed with air, preventing clumping and ensuring consistent flow. Additionally, the system is relatively simple in design, with fewer moving parts compared to other conveying methods, which reduces maintenance requirements and downtime.
Applications and Industries Benefiting from This Technology
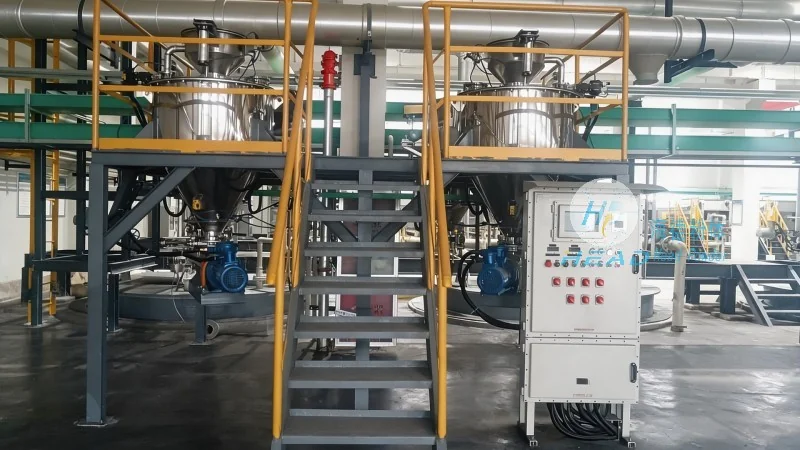
The negative pressure dilute phase powder pneumatic conveying system is widely used across various industries due to its versatility and efficiency. In the chemical industry, it is used to transport raw materials and finished products, such as powders and granules, between processing units. The food and pharmaceutical sectors also rely on this system for handling sensitive materials, ensuring product integrity and safety. The system is particularly effective in applications where dust control is critical, as the integrated dust collector captures and filters particles, preventing environmental contamination and maintaining air quality.
Conclusion: Why Choose HeadPowder's Negative Pressure Dilute Phase System
For businesses seeking a reliable and efficient solution for bulk powder transport, the negative pressure dilute phase pneumatic conveying system from HeadPowder offers a robust and cost-effective option. By leveraging advanced engineering and a deep understanding of material handling principles, HeadPowder ensures that their systems are tailored to meet the specific needs of each client. The combination of energy efficiency, material compatibility, and ease of maintenance makes this system an ideal choice for industries that demand precision and reliability in their material handling processes. With a strong presence in Shandong, China, HeadPowder continues to innovate and provide high-quality solutions that enhance operational efficiency and product quality.




