For industrial applications requiring efficient and reliable transport of powdered dry desulfurizers, the pneumatic conveying system developed by Shandong HeadPowder Engineering Co., Ltd. offers a sophisticated solution. This technology is crucial for optimizing the handling of desulfurizer powders, which are essential in flue gas treatment processes to reduce sulfur dioxide emissions. The following sections detail the working principle and key characteristics of this system, providing insights into its operational efficiency and practical advantages.
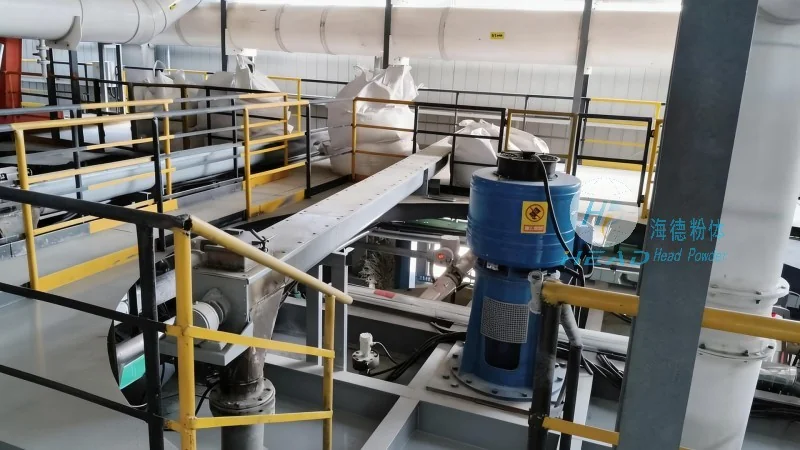
Introduction to Powdered Dry Desulfurizer Pneumatic Conveying by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field of powder handling technologies, specializes in the design and implementation of pneumatic conveying systems for industrial applications. HeadPowder, as the company is commonly known, is headquartered in Shandong, China, and has established itself as a trusted partner for businesses seeking advanced solutions for material transport. The company's expertise lies in tailoring systems to meet specific operational needs, ensuring that clients receive equipment that is both efficient and cost-effective. The pneumatic conveying system for powdered dry desulfurizers is a prime example of their commitment to innovation and quality.
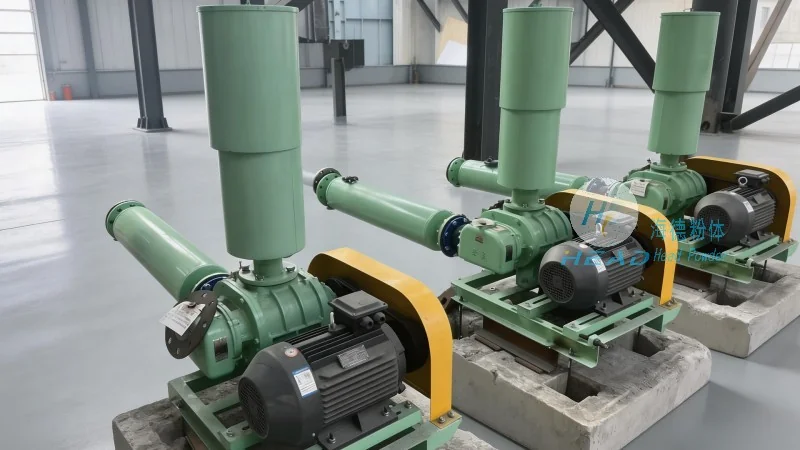
Working Principle of Pneumatic Conveying for Dry Desulfurizer Powders
The core of the pneumatic conveying system for dry desulfurizer powders is the utilization of compressed air or gas to transport the material through a network of pipes. The process begins with the desulfurizer powder stored in a hopper or silo. When the system is activated, a fan or compressor generates a flow of air, which is introduced into the hopper. The air and powder mixture forms a slurry-like flow, known as a "pneumatic stream," that travels through the pipeline to the destination point, such as a reactor or processing unit. The velocity of the air and the design of the pipeline are critical factors in ensuring that the powder is transported without clogging or degradation. The system typically includes components like a feeder, which controls the flow rate of the powder, a filter to remove any excess dust from the air, and a pressure regulator to maintain consistent air pressure. This integrated approach ensures a smooth and continuous transport of the desulfurizer powder, minimizing downtime and maximizing operational efficiency.
Key Characteristics of the Pneumatic Conveying System
The pneumatic conveying system for powdered dry desulfurizers exhibits several distinct characteristics that make it an ideal choice for industrial applications. Firstly, it offers high efficiency in material transport, as the system can handle large volumes of powder quickly and with minimal labor. Unlike traditional mechanical systems that rely on conveyor belts or buckets, pneumatic conveying eliminates the need for physical contact with the material, reducing wear and tear on equipment. Secondly, the system is environmentally friendly, as it operates in a closed loop, preventing dust emissions and protecting the surrounding environment. This is particularly important in industries where air quality regulations are stringent. Thirdly, the flexibility of the system allows for adjustments in the conveying distance and flow rate, making it adaptable to various plant layouts and operational requirements. Additionally, the system is relatively low-maintenance, with fewer moving parts compared to mechanical conveyors, which translates to lower operational costs and reduced maintenance time. Finally, the safety aspect is a significant advantage, as the enclosed system reduces the risk of exposure to the desulfurizer powder for operators, thereby enhancing workplace safety.
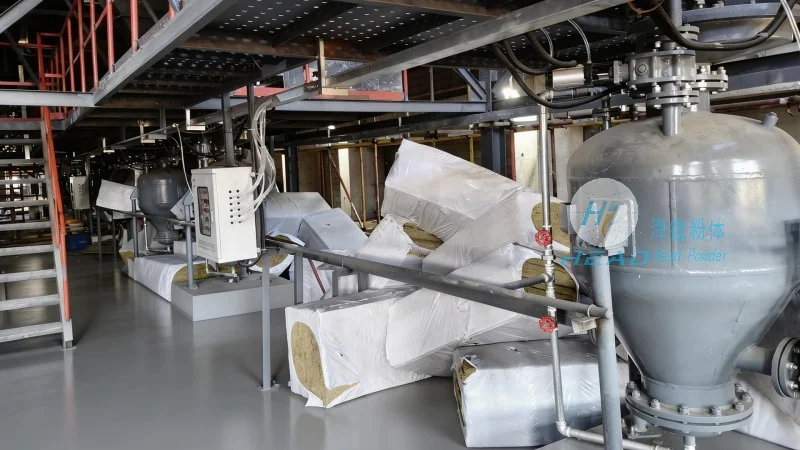
Operational Advantages and Practical Applications
From a practical standpoint, the pneumatic conveying system for dry desulfurizer powders provides several operational advantages. The ability to transport the powder over long distances without the need for intermediate storage points is a major benefit, as it streamlines the overall process flow. This is especially relevant in large-scale power plants or industrial facilities where the desulfurizer needs to be delivered from a central storage area to multiple processing units. The system also ensures consistent material quality, as the enclosed environment prevents contamination from external sources. Furthermore, the system's reliability is enhanced by its simple yet robust design, which minimizes the risk of breakdowns and ensures continuous operation. In summary, the pneumatic conveying system developed by Shandong HeadPowder Engineering Co., Ltd. represents a cutting-edge solution for the efficient handling of powdered dry desulfurizers, combining technological innovation with practical benefits that meet the demands of modern industrial operations.




