Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in the design, manufacturing, and supply of advanced grain material handling systems. With a focus on efficiency and reliability, our equipment is engineered to meet the demanding needs of modern grain processing and storage operations. Based in Shandong, China, we combine decades of industry expertise with cutting-edge technology to deliver solutions that enhance productivity and ensure the safe and efficient movement of grain materials.
Working Principles of Grain Material Handling System Equipment
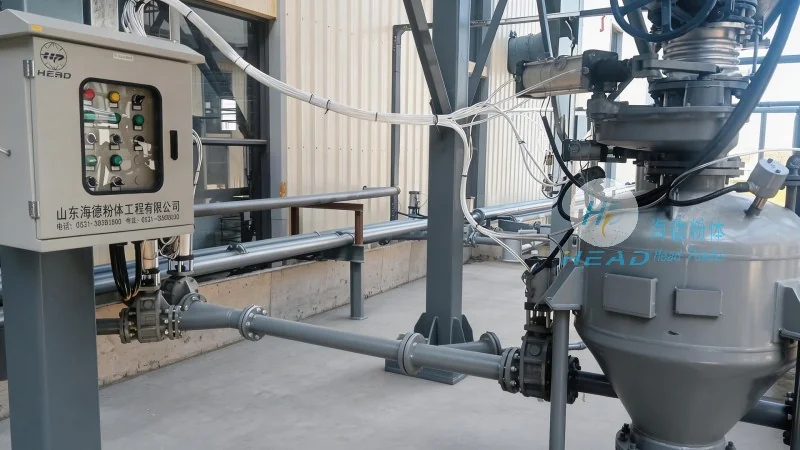
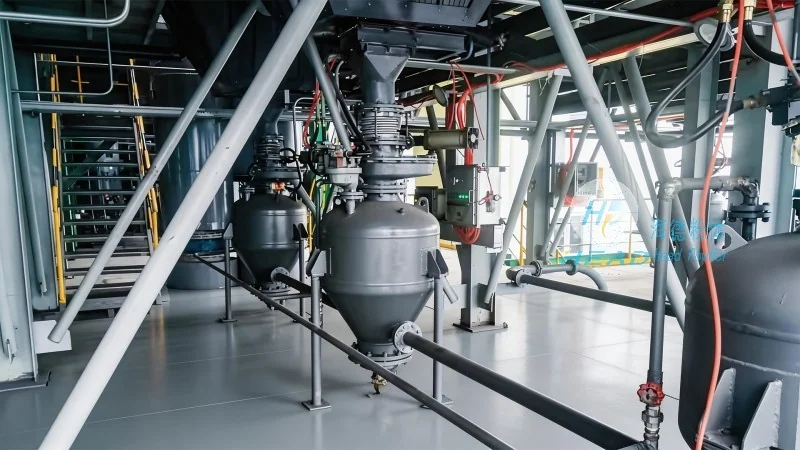
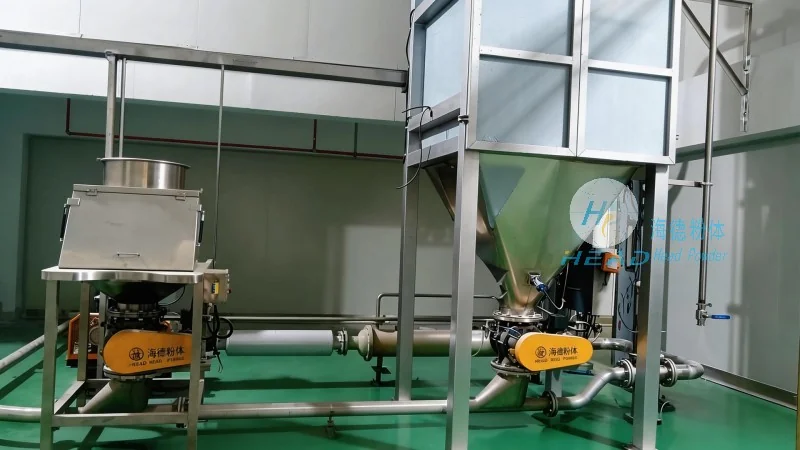
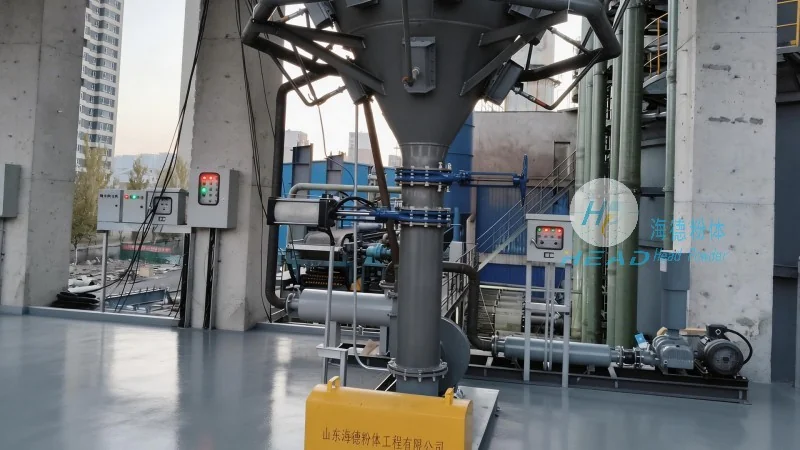
The working principle of grain material handling system equipment revolves around the efficient transfer of bulk materials through a combination of mechanical and electrical components. The process begins with the intake of grain, where a hopper or feeder collects the material and feeds it into a conveyor system. Belt conveyors, for instance, use a continuous belt to move grain horizontally, while screw conveyors utilize a rotating screw to transport material vertically or at an incline. Bucket elevators, another common component, lift grain using buckets attached to a chain or belt, allowing for vertical movement with high capacity. The system integrates sensors, such as load cells and level detectors, to monitor the flow and adjust the speed of the conveyors dynamically. This ensures that the grain is moved at an optimal rate, preventing overloading and reducing energy waste. Additionally, the control panel provides operators with real-time data on system performance, including speed, pressure, and temperature, enabling immediate adjustments to maintain efficiency. The design of the equipment emphasizes safety, with features like emergency stop buttons and overload protection to safeguard both the machinery and personnel during operation.
Key Features of Grain Material Handling System Equipment
Key features of our grain material handling systems include robust construction, enhanced durability, and user-friendly operation. The equipment is manufactured using high-grade materials, such as stainless steel and corrosion-resistant alloys, which resist wear and tear from abrasive grain particles, ensuring a longer service life. The modular design allows for easy integration with existing facilities and facilitates maintenance, as components can be replaced or upgraded without major system overhauls. Energy efficiency is a priority, with variable frequency drives (VFDs) and optimized motor configurations reducing power consumption by up to 30% compared to traditional systems. Advanced monitoring systems provide comprehensive data on performance, enabling predictive maintenance and reducing unexpected downtime. The systems also adhere to international safety standards, including CE certification, and are designed to minimize dust and noise, creating a safer working environment. Furthermore, the equipment is customizable to meet specific customer requirements, such as varying conveyor lengths, capacity adjustments, or integration with other processing equipment, ensuring a tailored solution for each application.




