Coal ash, a byproduct of coal combustion in power plants, is often in granular form and requires efficient handling and transportation for reuse or disposal. The process of coal ash particle material conveying involves specialized equipment and systems designed to move these materials safely and effectively. This article explores the working principle and key characteristics of coal ash granular material conveying systems, highlighting the technology and operational aspects that make them effective for industrial applications, with technical insights provided by Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions based in Shandong, China.
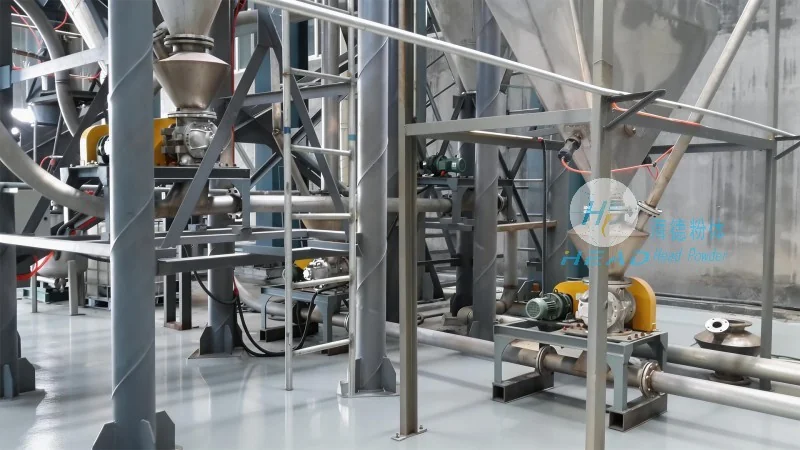
Working Principle of Coal Ash Granular Material Conveying
The working principle of coal ash particle material conveying typically involves a combination of mechanical and pneumatic systems, depending on the specific application and material properties. For bulk handling, screw conveyors, belt conveyors, and bucket elevators are commonly used. These systems operate by transferring the granular coal ash from one location to another through a series of rotating components or continuous belts. The screw conveyor, for instance, uses a rotating helical screw to push the material forward, while the belt conveyor relies on a moving belt that carries the particles along a predetermined path. In pneumatic conveying systems, air is used to create a flow that transports the coal ash particles through pipes, often with the assistance of positive or negative pressure to control the movement and direction of the material. Control systems play a crucial role in the operation of these conveying systems. Sensors and controllers monitor the flow rate, pressure, and temperature of the material, ensuring that the process runs smoothly and efficiently. This automation helps maintain consistent performance and reduces the risk of material blockages or system failures. The integration of these components allows for a seamless transfer of coal ash particles from storage areas, such as silos or hoppers, to processing units or disposal sites.
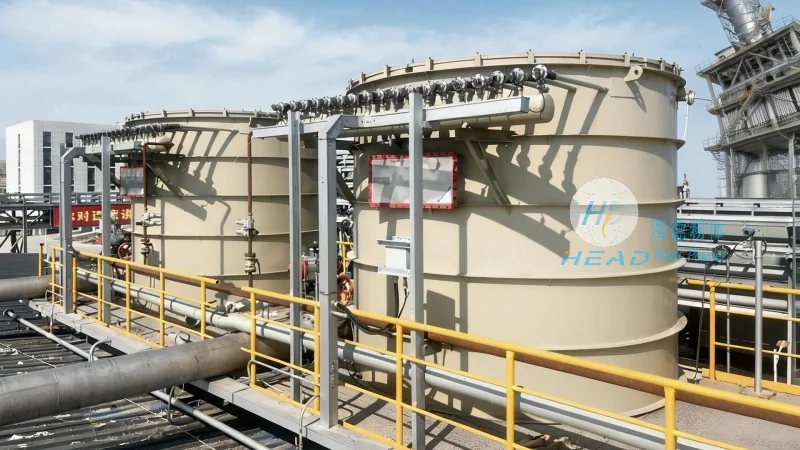
Key Characteristics of Coal Ash Granular Material Conveying
Efficiency is a primary characteristic of coal ash granular material conveying systems. These systems are designed to handle large volumes of material with minimal energy consumption, making them cost-effective for industrial operations. The ability to maintain a consistent flow rate and avoid material degradation is another important feature. Coal ash particles are often abrasive and can cause wear on equipment, so systems are engineered with durable materials and components to extend their lifespan and reduce maintenance costs. Another key characteristic is the adaptability of these conveying systems to different particle sizes and shapes. Whether the coal ash is fine or coarse, the equipment can be adjusted to handle the specific characteristics of the material. This flexibility is essential for applications where the composition of the coal ash may vary, such as in different power plants or during different stages of combustion. The systems also offer environmental benefits by reducing the need for manual handling and minimizing dust emissions, which is critical for maintaining workplace safety and compliance with environmental regulations.
Operational Considerations and Applications
When implementing coal ash granular material conveying systems, several operational considerations must be taken into account. The choice of equipment depends on factors such as the volume of material to be conveyed, the distance between the source and destination, and the required speed of transfer. For short distances and moderate volumes, screw conveyors may be sufficient, while for longer distances or larger volumes, belt conveyors or pneumatic systems are more appropriate. The system design also needs to consider the potential for material buildup and blockages, which can be mitigated through proper maintenance and the use of anti-wear coatings. Coal ash granular material conveying systems are widely used in various industrial applications. In power plants, they are used to transport ash from the boiler to storage facilities or to other processing units for reuse, such as in cement production or as a soil amendment. In construction and mining industries, the ash can be used as a filler material, and the conveying systems ensure that it is delivered to the job site efficiently. The versatility of these systems makes them suitable for a range of applications where bulk material handling is required.
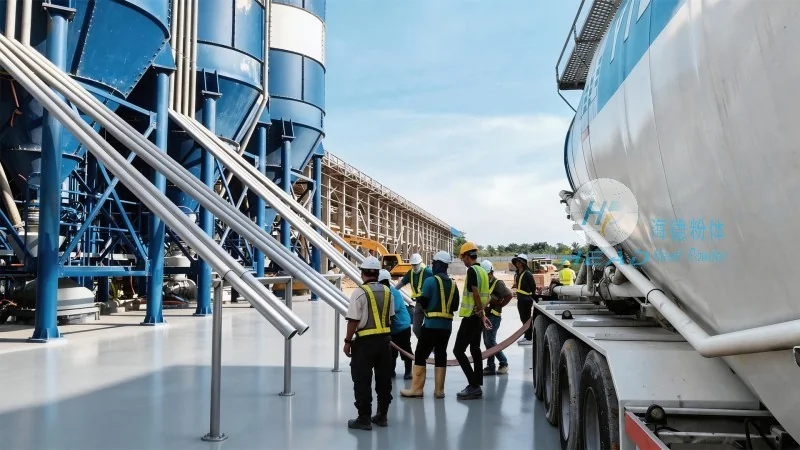
Conclusion
Coal ash granular material conveying systems are essential for the efficient and safe handling of coal ash particles. By understanding the working principle and key characteristics of these systems, industrial operators can select the appropriate equipment for their specific needs and optimize their operations. The technology continues to evolve, with advancements in materials and control systems improving the performance and reliability of coal ash conveying. As the demand for sustainable and efficient waste management increases, the importance of these systems in the coal ash industry will only grow. The expertise of companies like Shandong HeadPowder Engineering Co., Ltd. in designing and implementing such systems ensures that industrial facilities can meet their material handling requirements while adhering to safety and environmental standards.




