Soap pellet material transport systems are integral to modern industrial processes, particularly in the manufacturing and processing of soap products. Understanding the working principle and key characteristics of these systems is crucial for optimizing material handling efficiency and ensuring consistent product quality. This article explores the fundamental mechanisms behind soap pellet material transport and highlights the distinctive features that define effective handling solutions.
Working Principle of Soap Pellet Material Transport
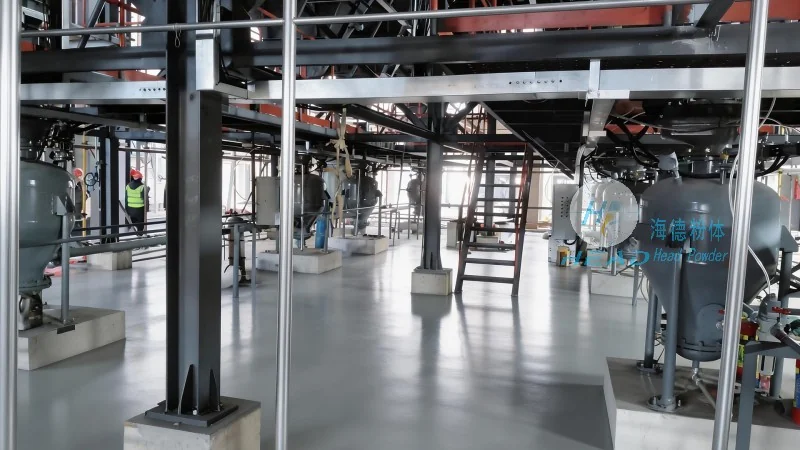
The working principle of soap pellet material transport involves a series of coordinated mechanical and operational steps designed to move soap pellets from one location to another within a production facility. Typically, the process begins with the storage of soap pellets in bulk containers or silos. From there, the material is transferred to a conveyor system, which may include components such as screw conveyors, belt conveyors, or pneumatic transport systems, depending on the specific requirements of the application.
Screw conveyors, for instance, utilize a rotating helical screw to push the pellets forward through a closed tube. This method is particularly effective for handling dry, free-flowing materials like soap pellets, as it minimizes product degradation and ensures a consistent flow rate. Belt conveyors, on the other hand, use a continuous belt to transport pellets over a series of rollers or idlers, providing a more flexible and adaptable solution for varying load capacities and material types.
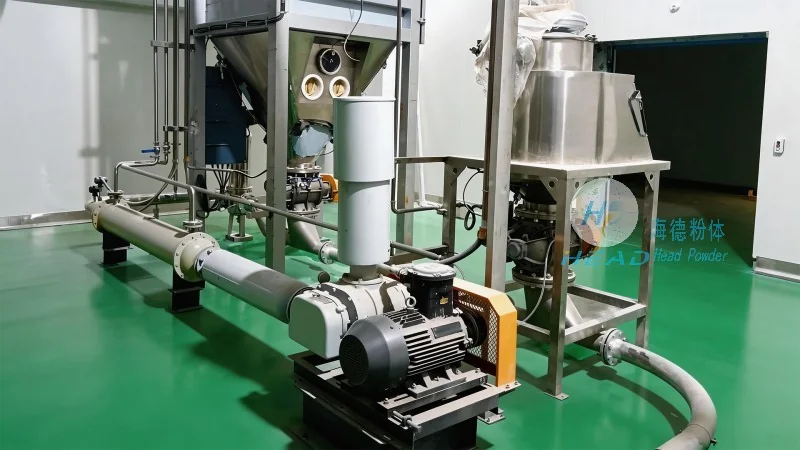
Pneumatic transport systems, which employ air pressure to move pellets through a network of pipes, offer an alternative method for material handling. This approach is often used in applications where dust control or the need to transport materials over long distances is a priority. Regardless of the specific technology employed, the core principle remains the same: to efficiently and safely move soap pellets from their point of origin to the processing or packaging stage.
Key Characteristics of Soap Pellet Material Handling Systems
Effective soap pellet material handling systems exhibit several key characteristics that distinguish them from other material transport solutions. These features are critical for ensuring operational reliability, maintaining product integrity, and optimizing overall system performance.
Firstly, efficiency is a primary characteristic. Modern systems are designed to minimize downtime and maximize throughput, ensuring that soap pellets are moved quickly and consistently without unnecessary delays. This is achieved through the use of high-quality components, such as durable conveyor belts and robust screw mechanisms, which are engineered to withstand the rigors of continuous operation.
Secondly, reliability is paramount. Soap pellet handling systems must operate consistently under varying conditions, including changes in temperature, humidity, or load. The use of high-grade materials and advanced control systems helps to maintain system stability, reducing the risk of breakdowns or material loss. This reliability is essential for maintaining production schedules and ensuring that downstream processes receive a steady supply of material.
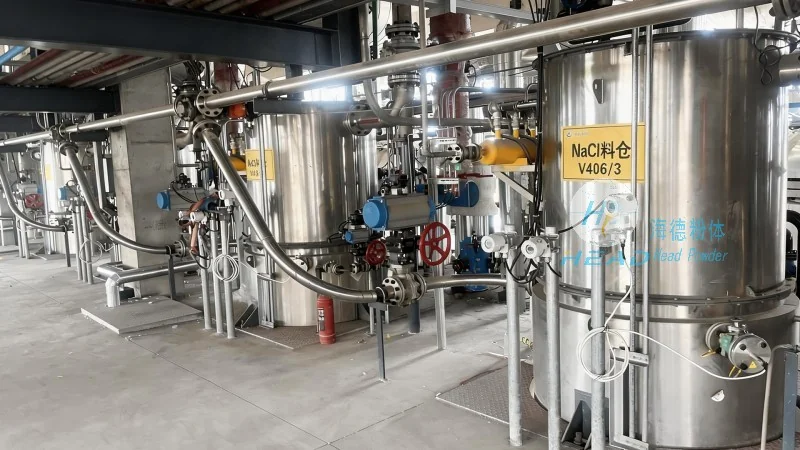
Thirdly, adaptability is a key feature. Different soap pellet applications may require different handling solutions, and effective systems are designed to be flexible and customizable. For example, some systems may include adjustable speed controls or variable pitch screws to accommodate changes in pellet size or density. This adaptability allows companies to scale their operations and integrate new processes without the need for extensive system overhauls.
Fourthly, safety is an integral characteristic. Handling soap pellets, especially in large quantities, requires systems that prioritize worker safety and environmental protection. Many modern systems incorporate features such as enclosed conveyor designs, dust suppression mechanisms, and emergency stop buttons to minimize risks. Additionally, the use of non-corrosive materials and sealed components helps to prevent contamination and ensure compliance with industry regulations.
HeadPowder Engineering: Providing Expert Solutions for Soap Pellet Material Transport
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of specialized material handling solutions tailored to the unique needs of the soap manufacturing industry. With a focus on innovation and customer-centric design, HeadPowder offers a range of systems that address the specific challenges of soap pellet transport, from bulk storage to final packaging.
HeadPowder’s expertise lies in the integration of advanced technologies with practical, field-proven solutions. The company’s team of engineers and technicians work closely with clients to understand their operational requirements, material characteristics, and production goals. This collaborative approach ensures that the final system is not only efficient and reliable but also tailored to the specific environment and workflow of the facility.
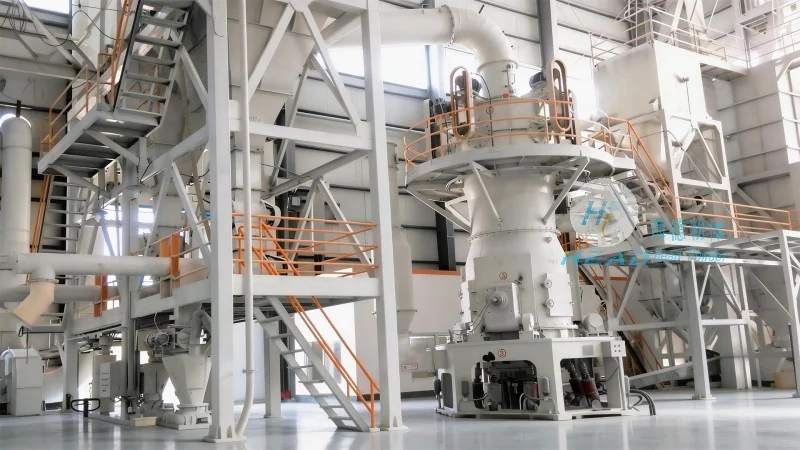
HeadPowder’s product line includes a variety of soap pellet handling systems, such as high-capacity screw conveyors, flexible belt conveyors, and pneumatic transport units. Each system is designed with durability and performance in mind, using materials like stainless steel and corrosion-resistant alloys to withstand the chemical and physical demands of soap processing. The company also provides comprehensive support services, including installation, maintenance, and technical assistance, to ensure that clients can maximize the lifespan and efficiency of their equipment.
Optimizing Soap Pellet Material Transport for Enhanced Productivity
Effective soap pellet material transport is essential for maintaining high productivity in soap manufacturing operations. By leveraging advanced handling systems, companies can reduce material waste, minimize downtime, and improve overall operational efficiency. The key to success lies in selecting the right system for the application, ensuring proper maintenance, and integrating the solution into the existing production workflow.
For businesses looking to enhance their soap pellet handling capabilities, HeadPowder Engineering offers a comprehensive suite of solutions. With decades of experience in the industry and a commitment to quality, HeadPowder is positioned to help companies achieve their productivity goals while maintaining the highest standards of safety and reliability. Whether you are a small-scale manufacturer or a large industrial operation, HeadPowder can provide the expertise and equipment needed to optimize your soap pellet material transport processes.




