

[WOKING PRINCIPLE AND FEATURES OF RARE EARTH POWDER PNEUMATIC CONVEYING EQUIPMENT]
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling rare earth powders. This article provides an in-depth look at the working principles and key features of such equipment, highlighting how it addresses the unique challenges associated with transporting these valuable materials.
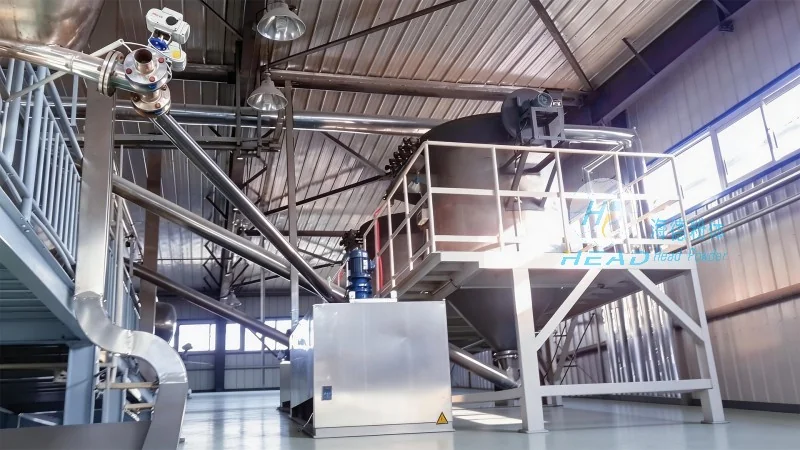
Introduction to Rare Earth Powder Pneumatic Conveying Systems
Rare earth powders, due to their fine particle size and high value, require specialized equipment to ensure efficient and safe transportation. Pneumatic conveying systems offer a reliable solution by utilizing air to move the material through pipelines. The technology has evolved significantly, with modern systems incorporating advanced control mechanisms and materials handling capabilities to meet industrial demands.
Working Principle of Rare Earth Powder Pneumatic Conveying Equipment
The core working principle of a pneumatic conveying system involves the use of compressed air to create a flow that transports the powder. There are primarily two types of pneumatic conveying: dilute phase and dense phase. Dilute phase systems use higher air velocities to keep the powder suspended in the air stream, suitable for short to medium distances. Dense phase systems, on the other hand, operate at lower velocities, creating a slurry-like flow that minimizes particle degradation and pressure drops. For rare earth powders, the choice often depends on the material's properties, such as particle size distribution and moisture content, as well as the required conveying distance and throughput.
In a typical setup, the system includes a feeding hopper, a conveyor line, and a discharge unit. The powder is first fed into the hopper, where it is then introduced into the pipeline via a venturi or rotary valve. Compressed air is supplied from a blower or compressor, creating a pressure differential that propels the powder forward. The air and powder mixture travels through the pipeline, and at the discharge end, the air is separated from the powder, often using a cyclone or filter system. The separated powder is then collected in a receiving container, while the air is either vented to the atmosphere or recirculated, depending on the system design.
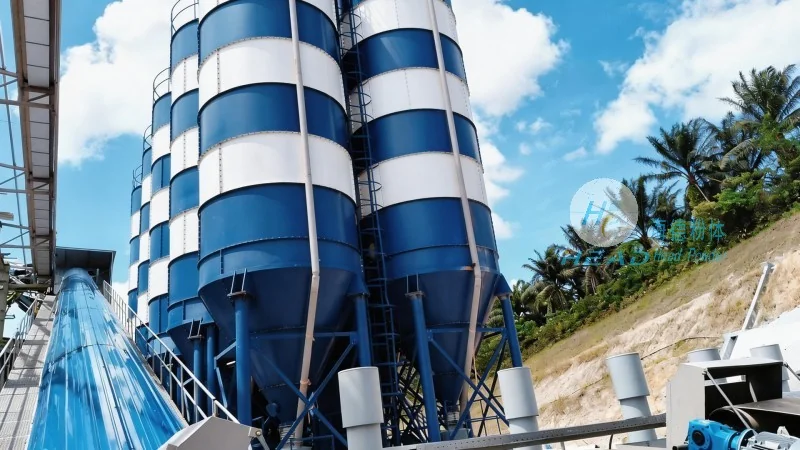
Key Features of Rare Earth Powder Pneumatic Conveying Equipment
When selecting a pneumatic conveying system for rare earth powders, several key features are critical to ensure optimal performance and reliability. These features include:
1. Material Compatibility: The equipment must be constructed from materials that are resistant to corrosion and wear caused by rare earth powders. Common materials include stainless steel, special alloys, and high-quality plastics. This ensures that the system can withstand the chemical and mechanical stresses associated with handling these materials without degradation.
2. Low Particle Degradation: Rare earth powders are often sensitive to mechanical stress, which can affect their properties. Advanced systems employ gentle feeding mechanisms and smooth pipeline designs to minimize particle attrition. This is crucial for maintaining the quality of the powder, especially when it is used in high-value applications such as electronics and aerospace.
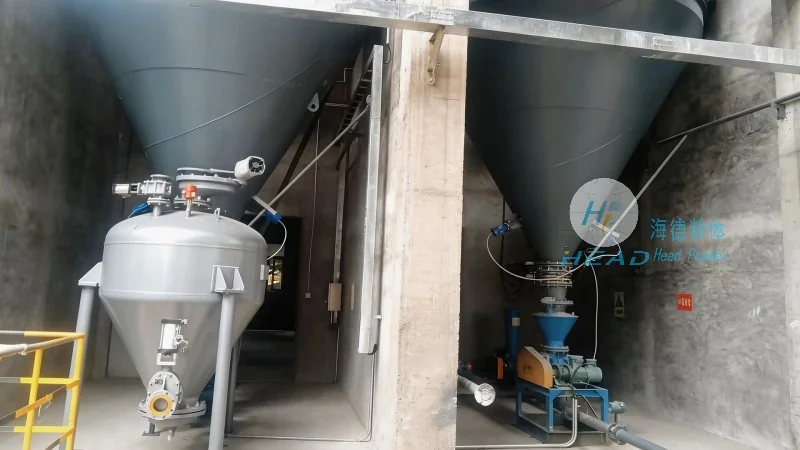
3. Precise Flow Control: The ability to control the flow rate accurately is essential for maintaining consistent product quality and preventing overloading or underloading of the system. Modern pneumatic conveying systems use variable frequency drives (VFDs) and advanced control algorithms to regulate the air pressure and flow, ensuring stable operation and efficient material transport.
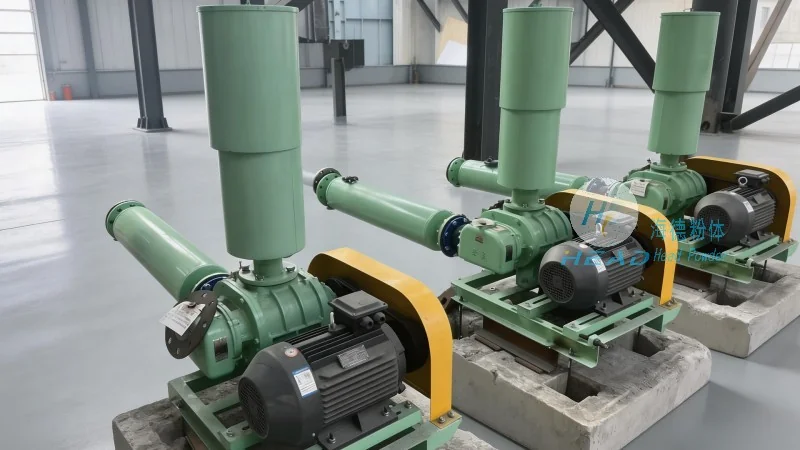
4. Energy Efficiency: Energy consumption is a significant factor in the operation of pneumatic conveying systems. High-efficiency blowers and optimized pipeline designs help reduce energy costs while maintaining the required conveying capacity. This is particularly important for large-scale industrial applications where long-term operational costs are a major consideration.
5. Safety and Environmental Considerations: Handling rare earth powders involves safety and environmental concerns, such as dust control and air quality. The equipment is designed with features like dust collection systems, explosion-proof components, and sealed pipelines to minimize the risk of dust explosions and ensure compliance with environmental regulations.
Applications and Benefits of Rare Earth Powder Pneumatic Conveying Systems
Rare earth powder pneumatic conveying systems are widely used in various industries, including electronics, metallurgy, and chemical manufacturing. The primary benefits of using such systems include improved process efficiency, reduced labor costs, and enhanced product quality. By eliminating the need for manual handling and traditional bulk transport methods, these systems provide a more streamlined and automated solution for material transport. Additionally, the ability to handle fine powders without clogging or degradation makes them ideal for applications where precision and consistency are paramount.
Conclusion
HeadPowder's pneumatic conveying equipment for rare earth powders combines advanced technology with robust design to address the unique challenges of handling these valuable materials. By understanding the working principles and key features of such systems, industries can make informed decisions to improve their material handling processes, enhance product quality, and reduce operational costs. With a strong presence in Shandong, China, HeadPowder continues to lead in the development of innovative solutions for the efficient and safe transport of rare earth powders.