

What is a Multi-Hopper Pneumatic Powder Conveying System? And What Are Its Design Principles?
Multi-hopper pneumatic powder conveying equipment is a specialized system designed for the efficient and reliable transportation of bulk powders over long distances or within complex industrial setups. This technology has become an essential component in various industries, including pharmaceuticals, food processing, and chemical manufacturing, where the safe and hygienic handling of powders is paramount. The system operates by using compressed air to transport powders through a network of pipes, ensuring minimal product degradation and contamination.
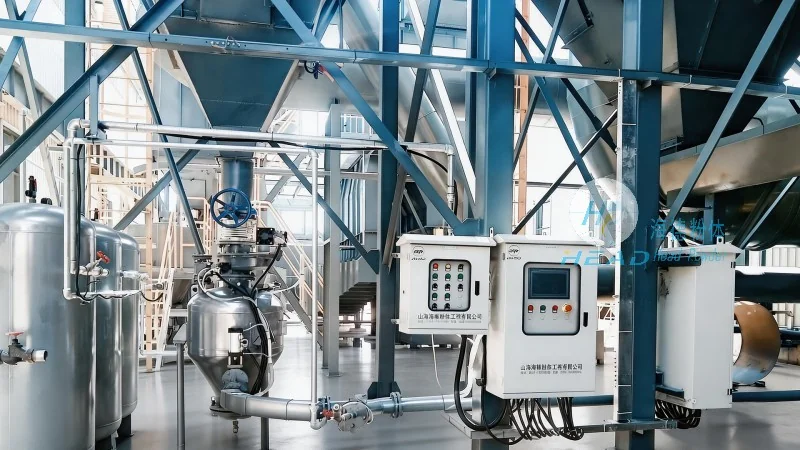
Understanding the Core Components of Multi-Hopper Systems
At the heart of a multi-hopper pneumatic conveying system lies a series of hoppers, each designed to store and meter different types of powders. These hoppers are typically equipped with feeding mechanisms, such as rotary valves or screw feeders, which control the flow rate of the material into the conveying line. The system also includes a central control unit that manages the operation of each hopper and the overall conveying process, ensuring precise and synchronized material transfer. Additionally, the system features a filter and cyclone separator to capture and return any fines or dust back to the hoppers, maintaining product purity and system efficiency.
Design Principles Behind Multi-Hopper Pneumatic Conveying
The design of a multi-hopper system is guided by several key principles aimed at optimizing performance, energy efficiency, and operational safety. One of the primary principles is the use of positive pressure or negative pressure (or a combination of both) to move powders through the system. Positive pressure systems, where air is blown into the conveying line, are commonly used for short to medium distances and for materials that are prone to caking or agglomeration. Negative pressure systems, where air is drawn out of the line, are preferred for longer distances and for materials that are more free-flowing. The design also considers the particle size distribution of the powder, as larger particles may require higher air velocities to maintain suspension, while smaller particles need more careful control to avoid excessive pressure drop and energy consumption.
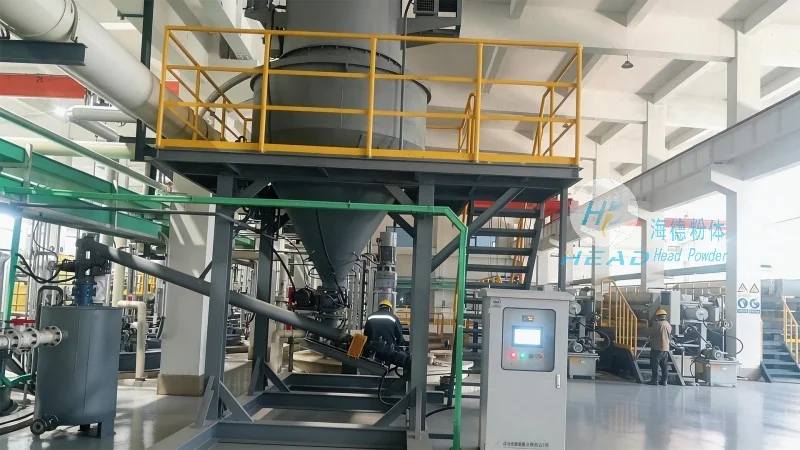
Key Advantages of Multi-Hopper Pneumatic Conveying Equipment
Multi-hopper systems offer several advantages over traditional conveying methods, such as belt conveyors or bucket elevators. These include the ability to handle a wide range of powder types, from fine powders to bulk materials, without the need for additional equipment like hoppers or silos. The system also provides a closed-loop operation, which minimizes dust emissions and improves workplace safety. Furthermore, the modular design of multi-hopper systems allows for easy expansion or modification as production needs change, making it a flexible solution for growing businesses. The energy efficiency of these systems is another significant benefit, as they can operate with lower air pressures compared to other pneumatic conveying methods, reducing operational costs over time.
Applications in Industrial Settings
Multi-hopper pneumatic conveying equipment is widely used in various industrial applications where the handling of powders is critical. In the pharmaceutical industry, for example, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision and minimal contamination, ensuring compliance with stringent regulatory standards. In the food processing sector, the system is employed to convey ingredients like flour, sugar, and spices, maintaining hygiene and preventing cross-contamination. The chemical industry also benefits from these systems when handling reactive or hazardous powders, as the closed-loop design provides a safe and controlled environment. Additionally, in the agricultural sector, multi-hopper systems are used to transport fertilizers and other bulk materials, improving efficiency in storage and distribution.
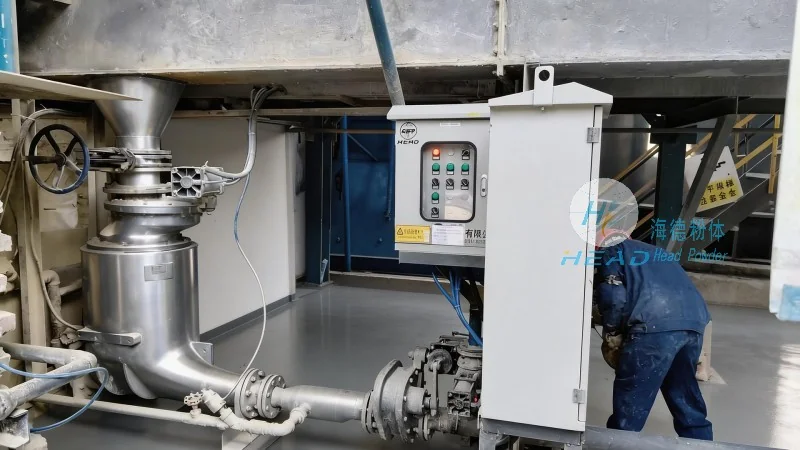
Customization and Integration with Existing Facilities
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of multi-hopper pneumatic conveying systems, specializes in customizing equipment to meet the specific needs of each client. The company’s engineers work closely with customers to understand their production requirements, material characteristics, and operational constraints, then design a system that optimizes performance and cost-effectiveness. The multi-hopper systems can be integrated seamlessly with existing facilities, including silos, storage tanks, and processing lines, without disrupting current operations. This integration ensures a smooth transition to the new conveying system and minimizes downtime during installation.
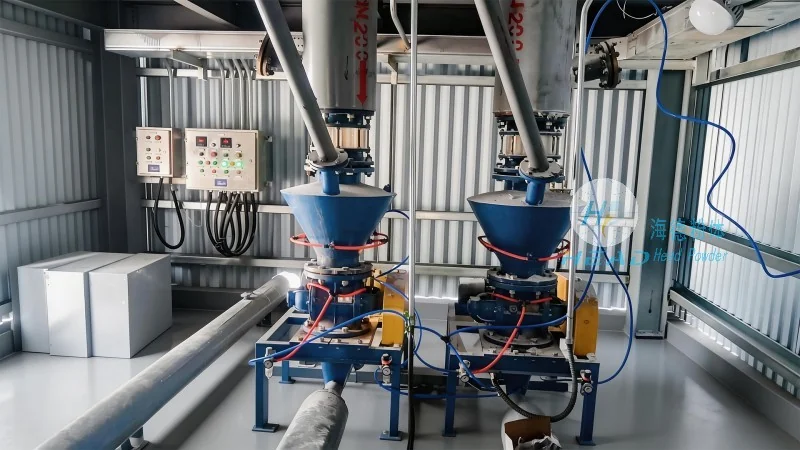
Maintenance and Operational Considerations
Proper maintenance is essential to ensure the long-term reliability and efficiency of a multi-hopper pneumatic conveying system. Regular cleaning of the hoppers, filters, and cyclone separators is necessary to prevent clogging and maintain air flow. The system’s control unit should be checked periodically to ensure it is functioning correctly and that the feeding mechanisms are operating at the desired speed. Additionally, monitoring the air pressure and flow rates can help identify any issues early on, allowing for timely maintenance and preventing system failures. The use of high-quality materials, such as stainless steel for the hoppers and pipes, also contributes to the durability and longevity of the equipment.
Conclusion: The Role of Multi-Hopper Systems in Modern Manufacturing
Multi-hopper pneumatic powder conveying equipment plays a vital role in modern manufacturing by providing an efficient, safe, and flexible solution for the transportation of bulk powders. The design principles behind these systems, combined with advanced control technologies, ensure that powders are handled with precision and minimal risk of contamination. As industries continue to demand higher standards of product quality and operational efficiency, the importance of multi-hopper systems will only grow. Shandong HeadPowder Engineering Co., Ltd. remains committed to delivering innovative and reliable solutions that meet the evolving needs of its clients, helping them achieve their production goals while maintaining the highest standards of safety and performance.