HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. This article focuses on the design of a specialized pneumatic conveying system tailored for the efficient transport of red sugar, a critical component in the food processing industry.
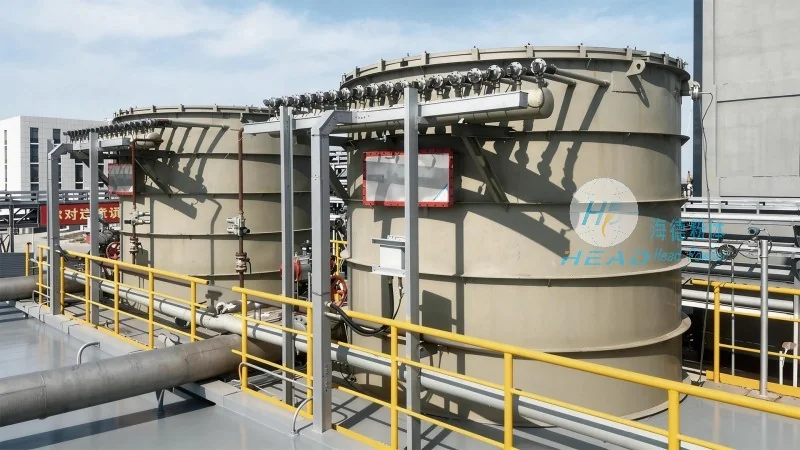
Overview of the Red Sugar Pneumatic Conveying System
The pneumatic conveying system for red sugar is engineered to meet the unique demands of handling granular, hygroscopic materials while ensuring minimal product degradation and optimal operational efficiency. HeadPowder's design incorporates state-of-the-art technology to address the challenges associated with red sugar's physical properties, such as its tendency to clump and its sensitivity to moisture.
Key Components and Design Features
The system comprises several core components, each meticulously selected to enhance performance and reliability. These include a high-capacity air compressor, a hopper for material storage, a rotary airlock valve for controlled discharge, and a flexible hose or pipeline system for material transport. The design emphasizes the use of corrosion-resistant materials, such as stainless steel, to withstand the acidic and moisture-rich environment typical of red sugar processing.
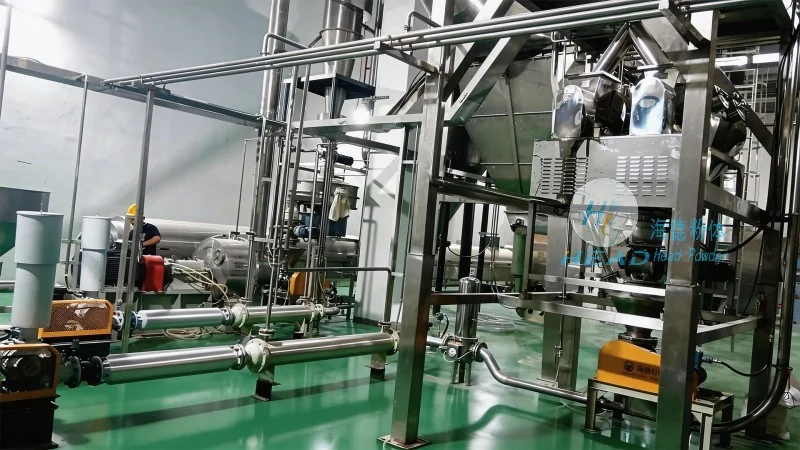
One of the standout features is the integration of a dust collection and filtration system, which ensures compliance with environmental regulations and maintains a clean working environment. The system also incorporates advanced control mechanisms, allowing for precise regulation of air pressure and flow rates to optimize conveying efficiency and minimize energy consumption.
Operational Advantages and Benefits
Implementing this pneumatic conveying system offers several significant advantages for red sugar manufacturers. Firstly, it enables a dust-free and hygienic material handling process, which is essential for maintaining product quality and meeting stringent food safety standards. Secondly, the system reduces material handling time and labor costs by automating the transport process, thereby increasing overall production throughput.
Furthermore, the design minimizes product breakage and contamination risks, which are critical concerns in the food industry. By using a closed system with minimal contact points, the risk of cross-contamination is significantly reduced. The system's flexibility also allows for easy integration with existing production lines, making it a cost-effective solution for both new and retrofit applications.
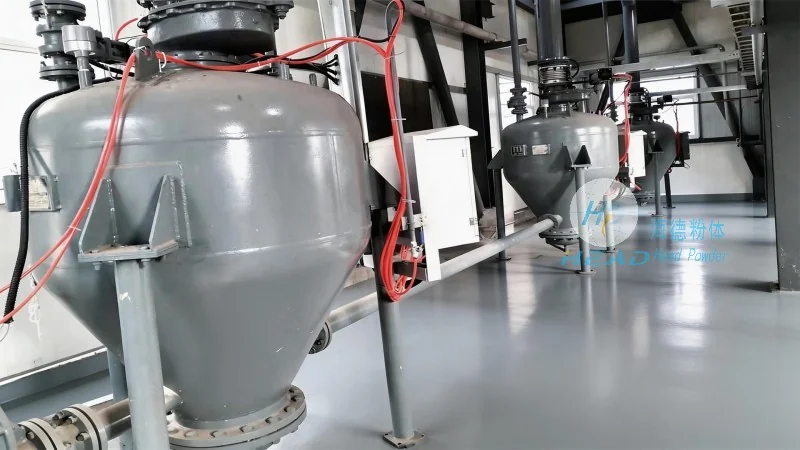
Customization and Scalability
HeadPowder recognizes that each red sugar processing facility has unique operational requirements. Therefore, the pneumatic conveying system is designed with scalability in mind, allowing for adjustments in capacity and configuration to suit varying production volumes. The company offers tailored solutions, ensuring that the system aligns with the specific needs of the client, whether it's a small-scale operation or a large industrial facility.
Conclusion
HeadPowder's design of the red sugar pneumatic conveying system exemplifies the company's commitment to delivering innovative, efficient, and reliable material handling solutions. By leveraging advanced engineering principles and adhering to industry best practices, the system provides a superior alternative to traditional conveying methods, offering enhanced product quality, operational efficiency, and cost savings. For businesses in the red sugar industry seeking to optimize their material handling processes, this system represents a valuable investment in productivity and compliance.




