

What is a Purified Powder Body Conveyor? Understanding Its Design Principles
HeadPowder, a leading manufacturer based in Shandong, China, specializes in industrial equipment designed for efficient and safe powder handling. Among their product line is the purified powder body conveyor, a critical component in industries where handling fine powders requires stringent cleanliness and contamination control. This equipment is engineered to transport dry powders and granular materials with minimal risk of particle loss or cross-contamination, making it essential in sectors such as pharmaceuticals, food processing, and high-purity chemical manufacturing.
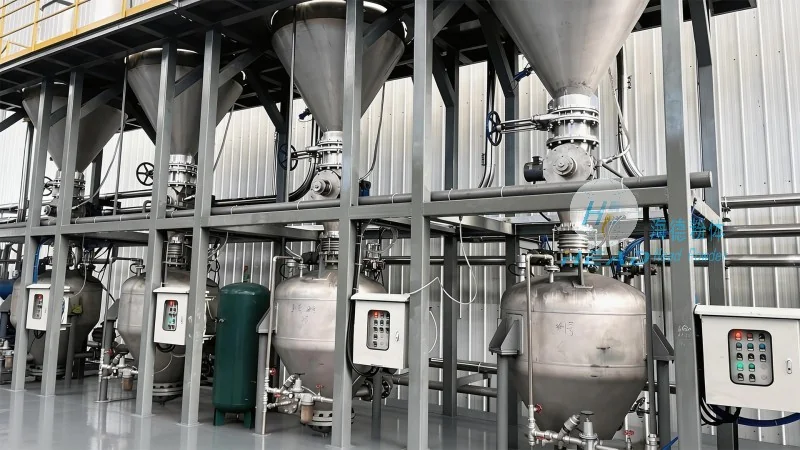
Key Features and Design Objectives
The design of a purified powder body conveyor prioritizes several key factors to ensure optimal performance in cleanroom environments. First, the conveyor system is constructed using materials that are non-porous and easy to clean, such as stainless steel or specialized plastics, to prevent the accumulation of dust or residues. This is crucial for maintaining the purity of the conveyed materials, as even minor contaminants can compromise product quality in sensitive applications. Second, the conveyor features enclosed or semi-enclosed structures that minimize exposure to external air and prevent the escape of fine particles, thereby reducing the risk of cross-contamination in adjacent areas. Additionally, the design incorporates smooth, rounded surfaces and minimal dead zones to facilitate thorough cleaning and prevent material buildup, which is vital for maintaining hygiene standards in regulated industries.
Working Principle and Operational Mechanics
The core of a purified powder body conveyor is its ability to move materials through a controlled environment. The system typically consists of a hopper or feed inlet where the powder is loaded, followed by a conveyor belt or screw mechanism that transports the material along a defined path. The conveyor is often equipped with a drive system, such as a motor and gearbox, that provides consistent and adjustable speed control. This allows operators to regulate the flow rate of the powder, ensuring precise and uniform delivery to downstream processes. The design may also include features like variable speed drives or adjustable feed hoppers to accommodate different material types and processing requirements. For example, in pharmaceutical applications, the conveyor might be equipped with a positive displacement pump or a pneumatic system to handle sensitive powders without generating dust or air currents that could introduce contaminants.
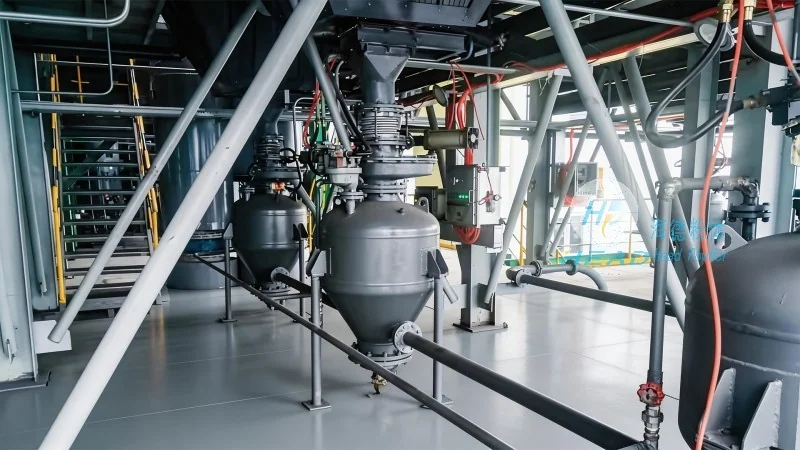
Applications and Industry Relevance
Purified powder body conveyors are widely used in industries where the purity of powders is non-negotiable. In the pharmaceutical sector, these conveyors are essential for transporting raw materials or finished products in cleanroom environments, ensuring that the final drug products meet stringent regulatory standards. Similarly, in the food industry, they are used to handle ingredients like flour, sugar, or spices, maintaining hygiene and preventing cross-contamination with other food products. In high-purity chemical manufacturing, the conveyor helps transport reagents or catalysts while minimizing the risk of contamination from ambient air or other materials. The versatility of the purified powder body conveyor makes it suitable for a range of applications, from small-scale laboratory operations to large-scale industrial production lines.
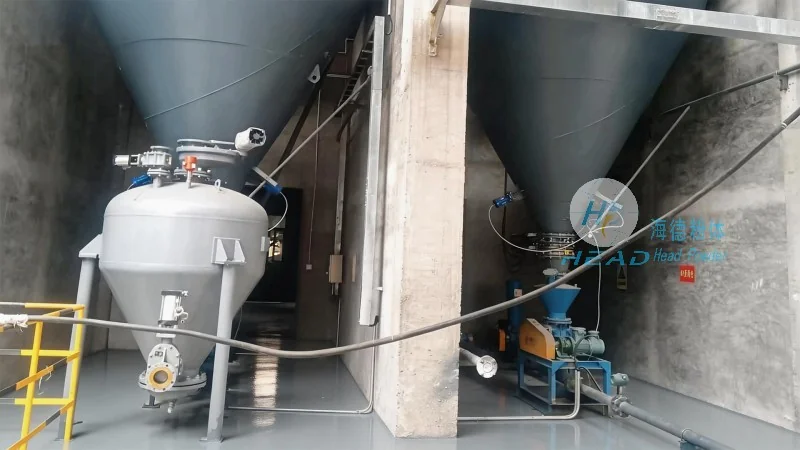
Advantages Over Traditional Conveying Systems
Compared to traditional conveyor systems, purified powder body conveyors offer several distinct advantages that make them the preferred choice for cleanroom applications. First, their enclosed design significantly reduces the risk of dust generation and particle loss, which is a major concern in traditional belt or screw conveyors. This not only improves product quality but also enhances workplace safety by minimizing exposure to airborne particles. Second, the materials used in the construction of these conveyors are highly resistant to corrosion and chemical attack, ensuring long-term durability and reliability in harsh industrial environments. Third, the conveyor’s design allows for easy integration with other equipment, such as hoppers, mixers, or packaging machines, creating a seamless material handling process. Additionally, the ability to adjust the speed and flow rate provides flexibility in accommodating different production rates and material characteristics, which is critical for optimizing operational efficiency.
Conclusion and Company Expertise
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of purified powder body conveyors and other industrial equipment. With a focus on innovation and adherence to industry standards, the company designs and manufactures conveyors that meet the stringent requirements of cleanroom environments. By prioritizing material purity, structural integrity, and operational efficiency, HeadPowder’s conveyors help industries maintain high-quality standards while ensuring safe and reliable material handling. Whether for pharmaceutical, food, or chemical applications, the purified powder body conveyor from HeadPowder is a reliable solution for transporting powders with the utmost care and precision.