HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for the handling of potassium carbonate. This article provides an in-depth overview of the equipment, its structural components, and the underlying principles that enable efficient material transport in industrial applications.
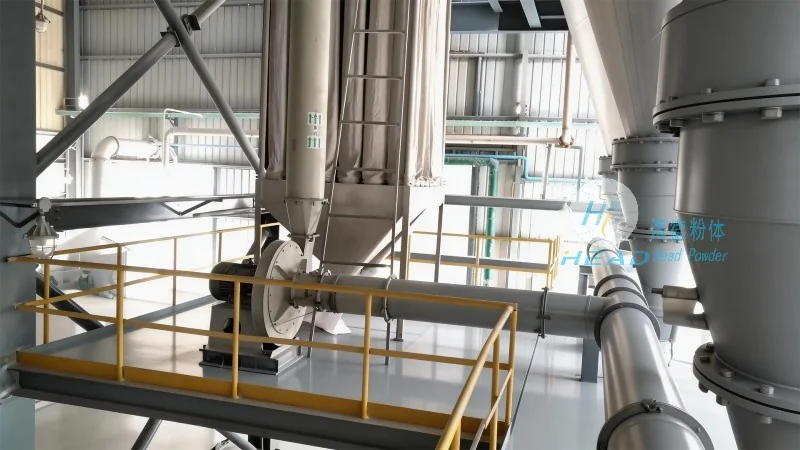
Overview of Potassium Carbonate Pneumatic Conveying Systems
Potassium carbonate, a critical chemical widely used in industries such as glass manufacturing, food processing, and chemical synthesis, often requires specialized handling solutions due to its bulk nature and processing requirements. Pneumatic conveying systems offer a highly effective method for transporting this material from storage to processing units, minimizing the need for manual handling and reducing operational risks. The systems are engineered to ensure reliable, dust-free, and energy-efficient material transfer, aligning with modern industrial standards for safety and productivity.
Key Structural Components of the Pneumatic Conveying System
The potassium carbonate pneumatic conveying system consists of several integrated components that work in concert to achieve seamless material transport. The primary elements include the material feed hopper, which serves as the initial storage and feeding unit, ensuring a consistent flow of potassium carbonate into the system. The feed hopper is equipped with a rotary valve or feeder mechanism that regulates the material discharge rate, preventing blockages and maintaining system stability.
Following the feed hopper is the conveying pipeline, typically made of corrosion-resistant materials like stainless steel or high-density polyethylene, to accommodate the chemical properties of potassium carbonate and prevent degradation or contamination. The pipeline is designed with appropriate bends and fittings to maintain the material's flow characteristics, minimizing pressure losses and ensuring efficient transport over varying distances.
A critical component in the system is the air compressor or blower unit, which generates the necessary airflow to move the material particles through the pipeline. The compressor is selected based on the system's capacity requirements, ensuring sufficient air pressure and volume to overcome resistance and maintain a consistent conveying velocity. The air system is equipped with filters and moisture separators to maintain air quality, preventing dust accumulation and ensuring the longevity of downstream equipment.
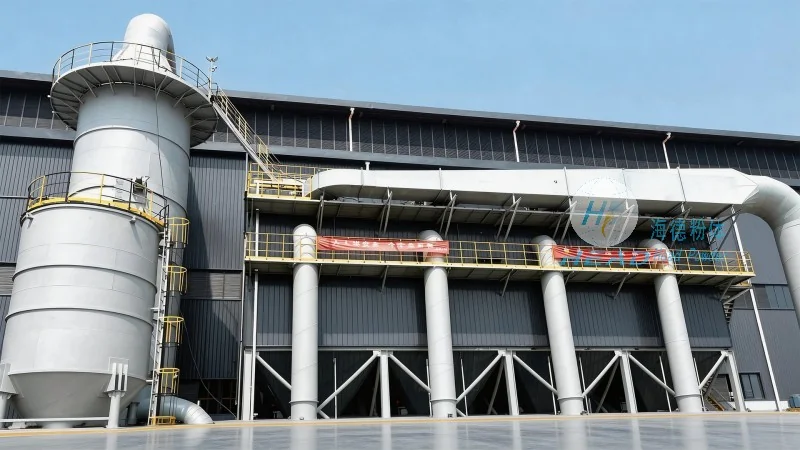
The system also includes a separation and collection unit, typically a cyclone or bag filter, which separates the potassium carbonate particles from the air stream at the receiving end. This unit ensures that the material is deposited into the target container or processing vessel without loss or contamination, while the clean air is discharged back into the environment or recirculated if necessary. The separation efficiency is optimized to meet industry standards, minimizing material loss and maintaining product purity.
Structural Principles and Operational Mechanics
The operational principle of the pneumatic conveying system is based on the fundamental concept of using air as a medium to transport solid particles. The system operates under either positive or negative pressure, depending on the specific application and material characteristics. In positive pressure systems, the air compressor forces air into the pipeline, carrying the potassium carbonate particles forward. In negative pressure systems, the air is drawn out of the system, creating a vacuum that pulls the material through the pipeline.
The conveying velocity is a key parameter that determines the system's performance. It must be maintained at an optimal level to prevent particle segregation, blockages, or excessive wear on the pipeline and components. The velocity is calculated based on factors such as particle size, density, and the pipeline diameter, ensuring that the material is transported efficiently without causing operational issues.
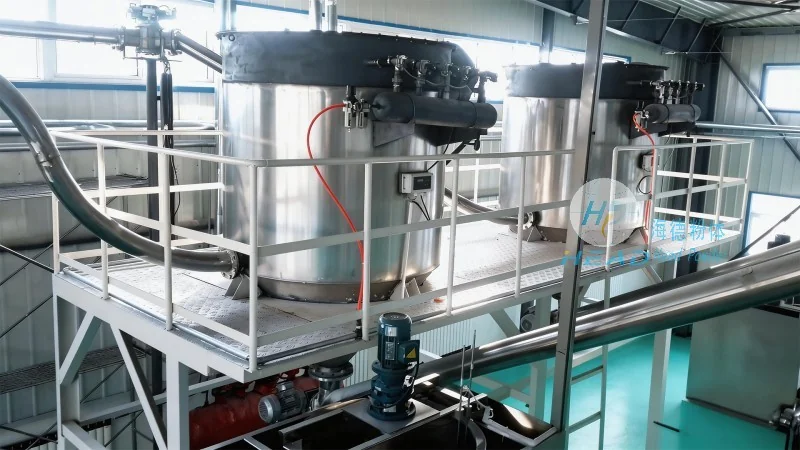
The system's design incorporates features to handle variations in material flow, such as changes in feed rate or pipeline length. This includes adjustable feed mechanisms, pressure sensors, and control valves that allow for real-time monitoring and adjustment of the conveying parameters. The structural integrity of the components is ensured through rigorous material selection and engineering, with considerations for corrosion resistance, durability, and maintenance accessibility.
Application and Industry Relevance
The potassium carbonate pneumatic conveying system is widely adopted in industrial settings where efficient and safe material handling is essential. In the glass industry, for example, potassium carbonate is used as a flux to lower the melting point of silica, and the system ensures that the material is delivered to the furnace without dust or contamination, improving the quality of the final product. In food processing, the system maintains product purity and hygiene standards by preventing cross-contamination and minimizing manual handling.
In chemical synthesis, the system facilitates the transport of potassium carbonate between processing stages, ensuring consistent feed rates and reducing downtime. The flexibility of the system allows for adaptation to different production scales, from small-scale laboratory applications to large-scale industrial operations. The reliability and efficiency of the equipment contribute to overall operational cost reduction and productivity enhancement in various industrial sectors.
Conclusion
HeadPowder's potassium carbonate pneumatic conveying system equipment exemplifies advanced engineering and industrial design, providing a reliable solution for the efficient handling of potassium carbonate. The integration of robust structural components and sound operational principles ensures consistent performance, safety, and product quality. As a company based in Shandong, China, HeadPowder continues to innovate and provide tailored solutions to meet the evolving needs of the chemical and industrial sectors, reinforcing its position as a trusted manufacturer in the field.




