HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems tailored for handling rare earth crystal powders. This article provides an overview of the rare earth crystal powder pneumatic conveying system, detailing its structural components and operational principles to help users understand its functionality and benefits.
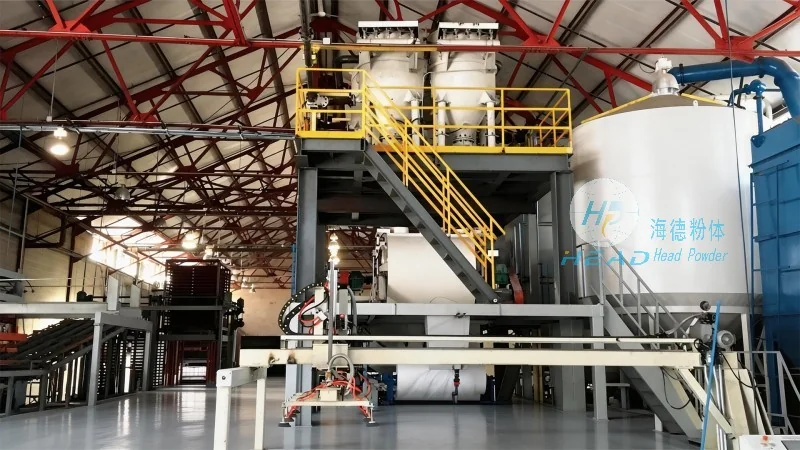
Company Profile and Background
HeadPowder, operating under the full name Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. With a strong focus on engineering excellence and customer-centric solutions, the company has established itself as a trusted partner in the material handling industry, particularly in systems that require precise and efficient transport of fine powders like rare earth crystals. The company's expertise lies in integrating innovative technologies to meet the unique challenges of handling such materials, ensuring high performance and reliability in industrial applications.
Overview of the Pneumatic Conveying System
The rare earth crystal powder pneumatic conveying system is a sophisticated piece of equipment designed to transport fine powders, such as rare earth crystals, through a pipeline using air or other gas as the conveying medium. This system is particularly advantageous for applications where traditional mechanical conveying methods may be less effective or efficient, especially when dealing with materials that are prone to caking, agglomeration, or require gentle handling to maintain particle integrity. The system operates by creating a pressure differential or using suction to move the powder through the pipeline, ensuring a continuous and controlled flow.
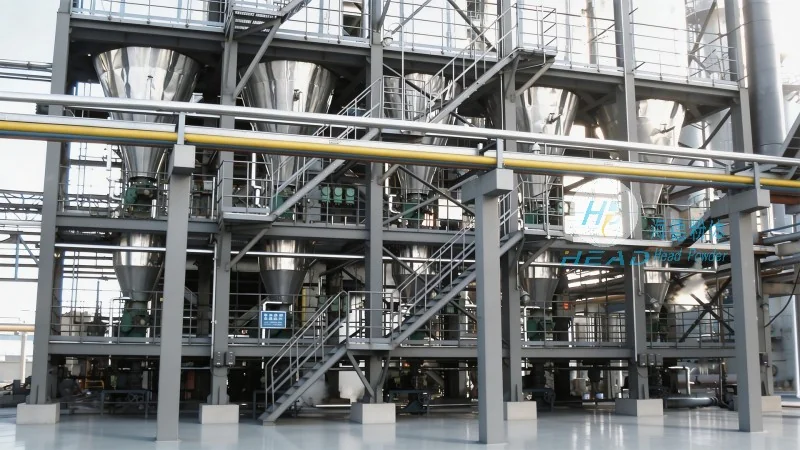
Key Structural Components
The pneumatic conveying system consists of several critical components that work in tandem to achieve efficient material transport. These components include the material feed hopper, which is responsible for storing and feeding the rare earth crystal powder into the system; the air supply unit, which generates the necessary air pressure or vacuum to move the material; the conveying pipeline, which forms the main path for the powder and air mixture; and the control system, which regulates the flow rate, pressure, and other operational parameters to ensure optimal performance. Additionally, the system may include accessories such as filters, cyclones, and dust collectors to manage air quality and prevent material loss or contamination.
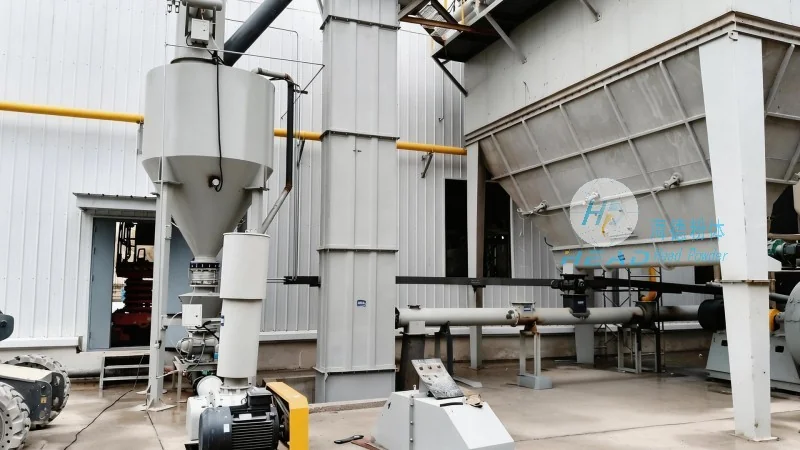
Operational Principles
The core operational principle of the rare earth crystal powder pneumatic conveying system is based on the physics of fluid dynamics and particle movement. When air is introduced into the conveying pipeline, it creates a flow that lifts and transports the powder particles. The system can operate in either pressure or vacuum mode. In pressure mode, compressed air is used to push the material forward, while in vacuum mode, a vacuum pump creates a negative pressure that pulls the material through the pipeline. The choice between these modes depends on factors such as the distance to be covered, the material characteristics, and the desired flow rate. The system's design ensures that the powder particles are suspended in the air stream, preventing them from settling or clogging the pipeline. This suspension is achieved by maintaining a sufficient air velocity, which is calculated based on the particle size, density, and other physical properties of the rare earth crystals.
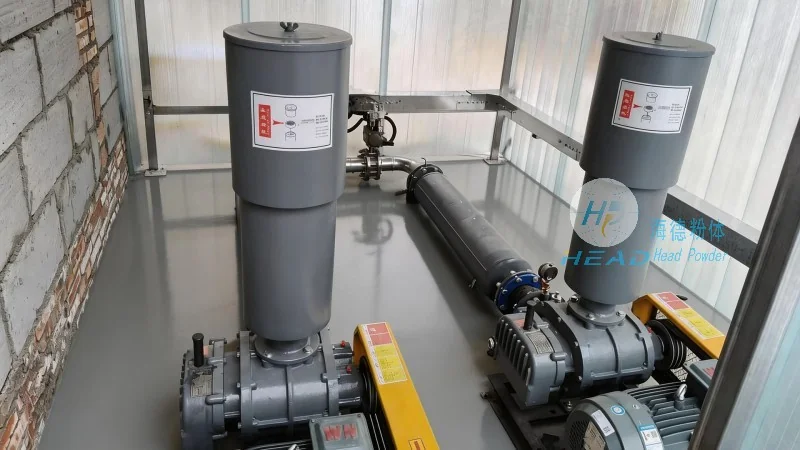
Advantages and Applications
The rare earth crystal powder pneumatic conveying system offers several advantages over traditional conveying methods. These include the ability to handle fine and abrasive materials without causing wear and tear on the equipment, the flexibility to transport materials over long distances, and the reduced risk of material contamination due to enclosed systems. The system is particularly suitable for applications in the rare earth industry, where the precise handling of crystal powders is crucial for maintaining product quality and purity. Additionally, the system's compact design and ease of integration make it a viable solution for various industrial settings, including manufacturing plants, processing facilities, and research laboratories.
Conclusion
HeadPowder's rare earth crystal powder pneumatic conveying system represents a cutting-edge solution for the efficient and reliable transport of fine materials. By understanding its structural components and operational principles, users can appreciate the system's capabilities and benefits, ensuring optimal performance in their industrial applications. With its robust design and advanced technology, this system is a valuable asset for any facility handling rare earth crystals, providing a reliable and efficient means of material transport.




