The diatomite powder pneumatic conveying system is a specialized industrial solution designed for the efficient and reliable transport of diatomite powder. As a key component in many processing and manufacturing applications, this system ensures that diatomite, a natural sedimentary rock with high porosity and excellent filtering properties, is moved from storage to processing units with minimal loss and optimal performance. The system is engineered to handle the unique characteristics of diatomite, such as its fine particle size and low bulk density, which can pose challenges in traditional bulk material handling. By leveraging pneumatic conveying technology, the system provides a closed-loop, dust-free operation that enhances safety and environmental compliance in industrial settings.
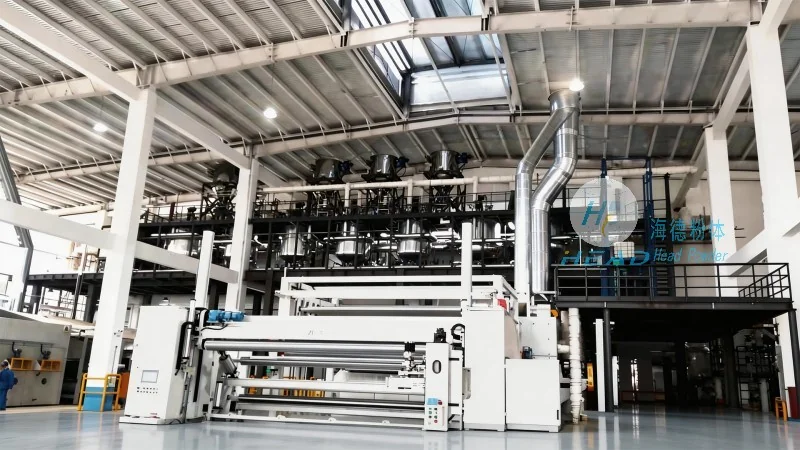
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the manufacturer behind this advanced pneumatic conveying system, is a leading provider of engineering solutions for powder handling and material transport. With a strong focus on innovation and customer-centric design, HeadPowder has established itself as a trusted partner in the industrial sector. The company is headquartered in Shandong, China, and specializes in developing customized solutions that meet the specific needs of clients across various industries, including pharmaceuticals, food processing, and chemical manufacturing. HeadPowder's commitment to quality and reliability is reflected in the robust construction and efficient operation of their pneumatic conveying systems, which are built to withstand the demands of high-volume and continuous material handling operations.
Key Components and Their Roles in the System
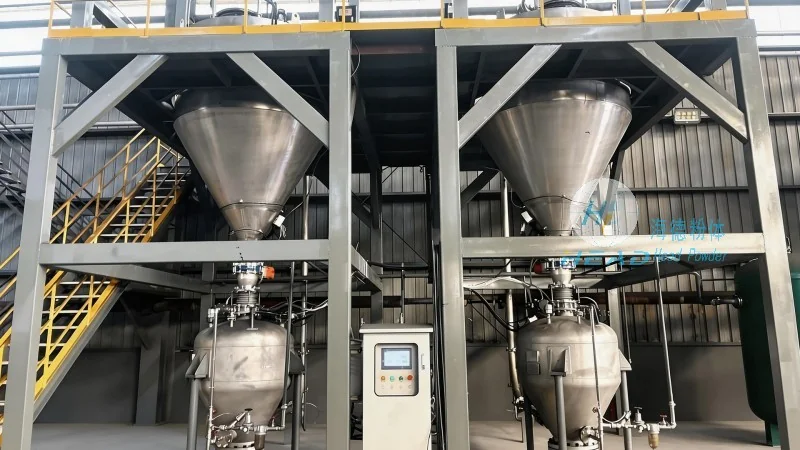
The diatomite powder pneumatic conveying system consists of several critical components that work in tandem to achieve effective material transport. The primary components include the hopper, which serves as the storage and feeding unit for the diatomite powder; the air compressor, which generates the necessary air pressure to move the powder through the system; the pipeline network, which connects the various components and transports the material; and the control system, which monitors and regulates the flow of powder and air. Each component plays a vital role in ensuring the smooth operation of the system. The hopper is designed with a sloped bottom and a discharge valve to facilitate the controlled release of powder into the pipeline. The air compressor provides the required pressure to create a flow of air that entrains the diatomite particles, while the pipeline network ensures that the material is transported to the destination without clogging or loss. The control system allows operators to adjust the air pressure, flow rate, and other parameters to optimize the conveying process and prevent issues such as blockages or excessive pressure drops.
Operation Process of the Pneumatic Conveying System
The operation of the diatomite powder pneumatic conveying system follows a systematic process that ensures efficient and consistent material transport. The process begins with the loading of diatomite powder into the hopper. The powder is then released from the hopper into the pipeline through the discharge valve, which is controlled by the system's control unit. Simultaneously, the air compressor starts to generate compressed air, which is introduced into the pipeline at a specific pressure. The compressed air creates a flow that entrains the diatomite particles, forming a slurry-like mixture known as a "pneumatic stream." This stream travels through the pipeline network to the destination point, such as a processing unit or storage silo. At the receiving end, the air is separated from the powder, typically through a cyclone separator or a filter, and the diatomite powder is collected in the receiving container. The air is then either recycled back into the system or vented to the atmosphere, depending on the system design. The entire process is automated and monitored by the control system, which adjusts the parameters in real-time to maintain optimal performance. This operation process is designed to minimize downtime, reduce material loss, and ensure that the diatomite powder is delivered to its destination in a clean and efficient manner.
Working Principle of the Pneumatic Conveying System
The working principle of the diatomite powder pneumatic conveying system is based on the fundamental concept of pneumatic transport, which involves the use of air to move solid particles. The system operates on the principle of creating a pressure differential between the source and destination points of the material. The air compressor generates a high-pressure air stream that is introduced into the pipeline, creating a pressure higher than the ambient pressure at the receiving end. As the diatomite powder is released into the pipeline, the air stream entrains the particles, reducing the effective density of the mixture and allowing it to flow through the pipeline with minimal resistance. The key to the system's efficiency lies in the balance between the air pressure and the particle size and density of the diatomite powder. The system is designed to maintain a consistent flow rate and pressure, which ensures that the material is transported without clogging or excessive energy consumption. The control system plays a crucial role in maintaining this balance by adjusting the air flow and pressure based on real-time feedback from sensors and other monitoring devices. This working principle allows the system to handle the unique characteristics of diatomite powder, such as its fine particle size and low bulk density, while providing a reliable and efficient transport solution.
Advantages of Using a Diatomite Powder Pneumatic Conveying System
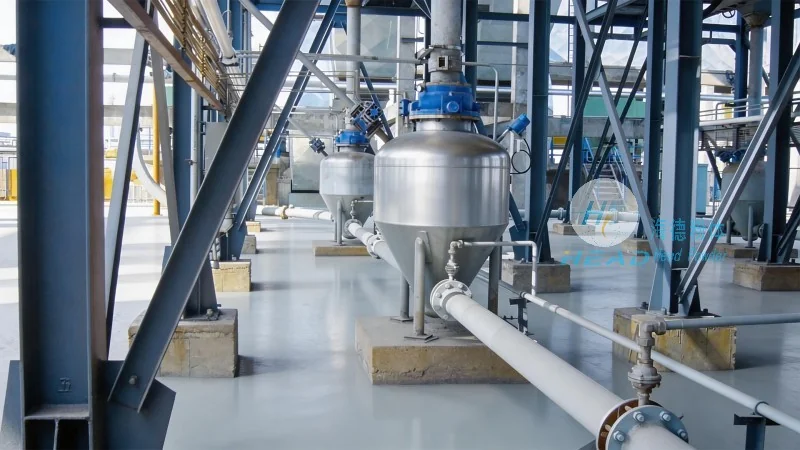
Implementing a diatomite powder pneumatic conveying system offers several significant advantages over traditional material handling methods. One of the primary benefits is the ability to achieve dust-free and closed-loop operation, which enhances safety in the workplace and reduces the risk of environmental contamination. The system also minimizes material loss during transport, as the powder is contained within the pipeline and handled in a controlled manner. This results in cost savings for the end-user, as less material is wasted and more is delivered to the processing unit. Additionally, the system is highly efficient in terms of energy consumption, as the air compressor and pipeline network are designed to operate with minimal energy loss. The automated control system further reduces the need for manual intervention, lowering labor costs and improving overall operational efficiency. The system's flexibility also allows it to be customized to meet the specific requirements of different applications, such as varying flow rates or material types. Overall, the diatomite powder pneumatic conveying system provides a reliable, efficient, and cost-effective solution for handling diatomite powder in industrial settings.
Conclusion and Contact Information
For businesses seeking an efficient and reliable solution for diatomite powder handling, the pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. offers a superior choice. With its robust design, advanced control system, and commitment to quality, this system ensures that diatomite powder is transported safely and effectively. HeadPowder, based in Shandong, China, provides customized solutions tailored to the unique needs of each client, ensuring optimal performance and minimal downtime. By leveraging the expertise and innovation of HeadPowder, industrial operations can enhance their material handling processes and improve overall productivity. For more information about the diatomite powder pneumatic conveying system or to learn how HeadPowder can assist with your specific material transport needs, please contact the company at their headquarters in Shandong, China.




