Principle and Working Scene Characteristics of Pneumatic Conveying Equipment for Phenolic Resin Powd
Release time:2026-09-20 03:01:37
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying equipment tailored for handling phenolic resin powders. This equipment is engineered to efficiently transport fine powders like phenolic resin through an air-driven system, offering a reliable solution for industrial applications where traditional bulk material handling methods may fall short. The core principle of pneumatic conveying involves using compressed air to move the powder particles through a pipeline, ensuring a seamless and dust-free transfer process.
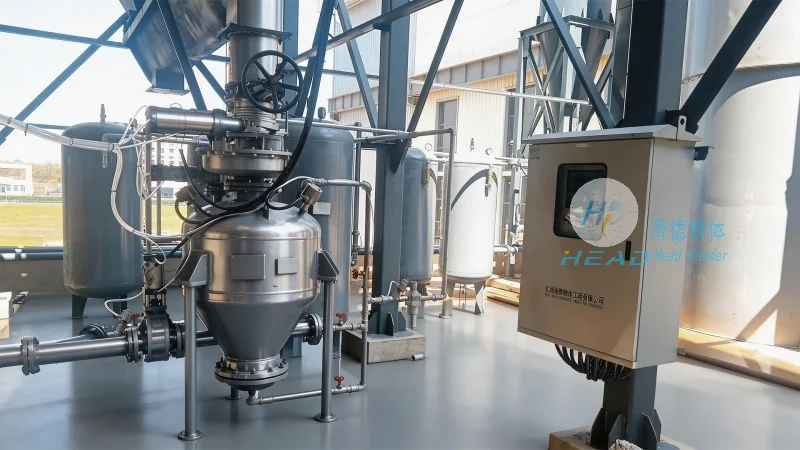
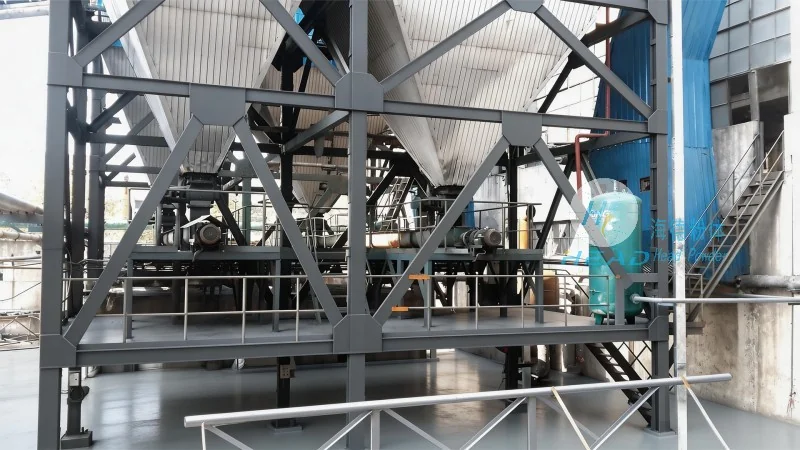
Principle of Operation for Phenolic Resin Powder Pneumatic Conveying
The pneumatic conveying system for phenolic resin powders operates on the fundamental principle of air flow and particle suspension. In this system, a blower or compressor generates high-pressure air that is introduced into the conveying line. The phenolic resin powder is then fed into the pipeline, where the air flow creates a low-pressure zone that lifts and transports the powder particles. The equipment typically includes components such as a hopper for material storage, a feeder to control the flow rate, a pipeline network for transport, and a receiver for material discharge. The design ensures that the powder remains suspended in the air stream, preventing clogging and maintaining consistent flow rates. This method is particularly effective for phenolic resin powders due to their fine particle size and cohesive properties, which can otherwise lead to blockages in traditional conveying systems.
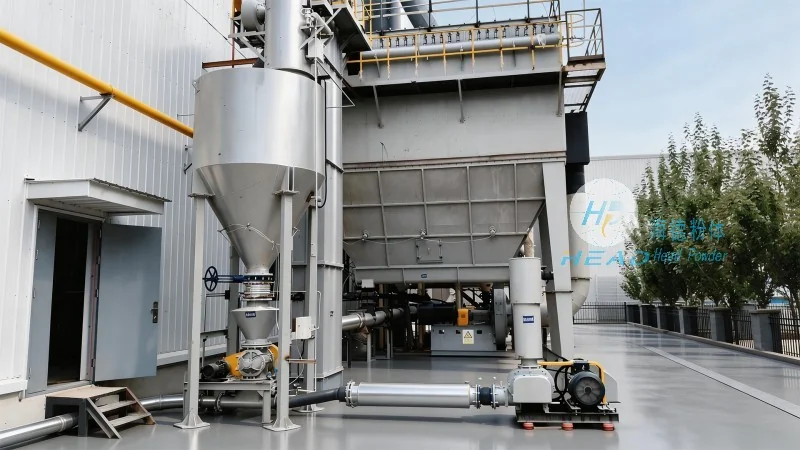
Key Working Scene Characteristics of the Equipment
The working scene characteristics of the pneumatic conveying equipment for phenolic resin powders are tailored to meet the demands of various industrial environments. One of the primary advantages is its ability to handle materials in a closed system, minimizing dust emissions and ensuring a clean working environment. This is crucial in applications where air quality and safety are paramount, such as in pharmaceutical or food processing industries where phenolic resin may be used as a binding agent or additive. Additionally, the system is designed for flexibility, allowing it to transport materials over varying distances and through complex layouts, including vertical and horizontal sections. The equipment is also capable of handling different powder loads, from low to high flow rates, making it suitable for both small-scale and large-scale production lines. The working scene typically involves integration with existing production processes, where the conveying system connects the resin storage area to the processing units, ensuring a continuous and uninterrupted supply of material. This integration enhances operational efficiency and reduces downtime associated with manual handling or traditional bulk transport methods.
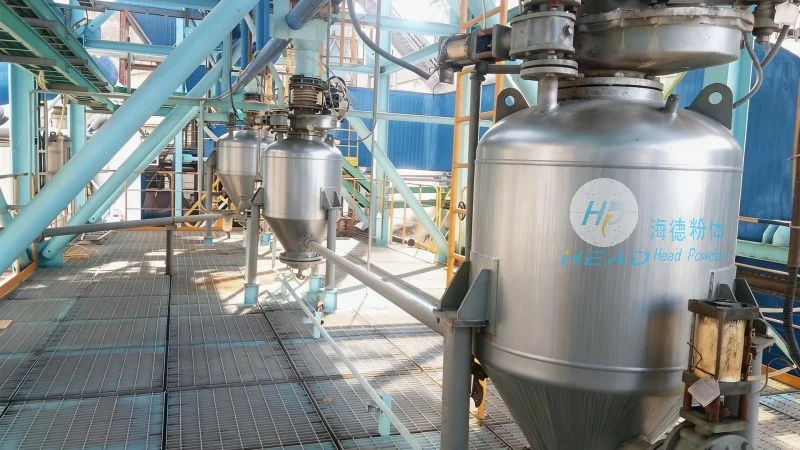
Advantages and Practical Applications
The pneumatic conveying equipment for phenolic resin powders offers several advantages that make it a preferred choice in industrial settings. One significant benefit is the reduction in labor costs and manual handling, as the system automates the material transport process. This not only improves safety by minimizing human exposure to dust and heavy lifting but also increases productivity by eliminating the need for frequent material transfers. The system also provides better material control, ensuring consistent quality and preventing contamination, which is critical for phenolic resin applications where purity is essential. Practical applications include the manufacturing of composites, adhesives, and coatings, where phenolic resin is used as a key component. The equipment is also suitable for use in research and development laboratories, where precise and controlled material handling is required for testing and formulation processes. In all these scenarios, the equipment's ability to handle fine powders efficiently and reliably contributes to improved overall process performance.




