HeadPowder, a leading provider in the field, specializes in the design and implementation of pneumatic conveying systems tailored for mining operations. These systems are engineered to efficiently transport bulk materials such as ores, powders, and granules over varying distances, ensuring optimal performance in challenging industrial environments.
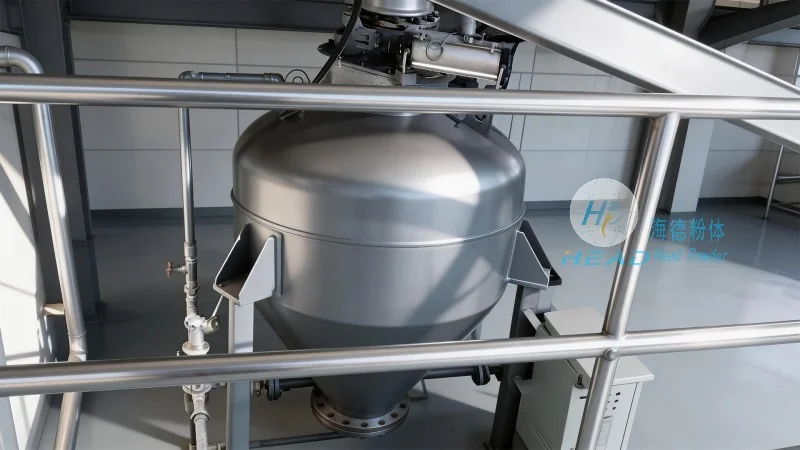
The Fundamental Principle of Pneumatic Conveying
The core principle of pneumatic conveying involves the use of air or gas to move materials through a pipeline. This method relies on the creation of a pressure differential, where air is introduced into the system to generate a flow that carries the material particles. The system typically consists of a hopper, a conveying line, and a discharge unit, with the air flow controlling the speed and direction of material transport. The technology offers advantages like dust reduction, minimal maintenance, and the ability to handle materials that are difficult to transport via traditional methods.
Key Components and Their Functions
Several critical components make up a pneumatic conveying system. The hopper serves as the material storage and feeding unit, ensuring a consistent supply of material to the system. The conveying line, often made of durable materials like stainless steel or plastic, is designed to withstand the pressures and abrasion from the transported materials. The air compressor or blower provides the necessary air pressure, while the control valves regulate the flow and pressure within the system. The discharge unit, such as a rotary valve or a venturi, manages the release of material at the destination point. Each component works in tandem to ensure smooth and efficient material transport.
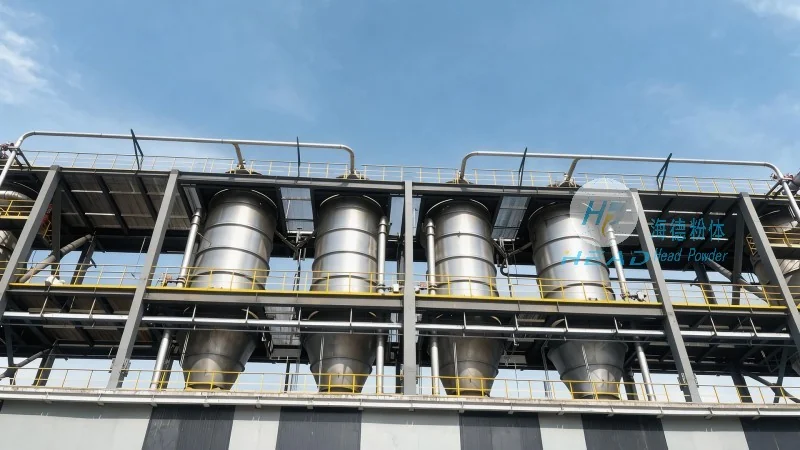
Working Scene Characteristics in Mining Operations
The application of pneumatic conveying in mining operations is characterized by specific operational demands. Mines often require the transport of large volumes of materials over long distances, which traditional methods may struggle to handle effectively. Pneumatic systems excel in these scenarios by providing a continuous, low-maintenance solution. The systems are also adaptable to different material types, including fine powders and coarse granules, making them versatile for various mining processes. Additionally, the enclosed nature of the conveying line helps in controlling dust and environmental impact, which is crucial in modern mining practices.
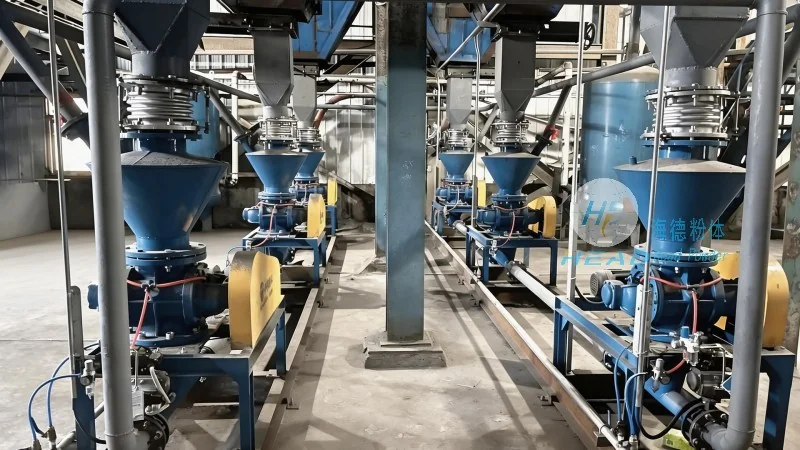
Advantages and Practical Applications
HeadPowder's pneumatic conveying systems offer several key advantages that make them ideal for mining applications. These include reduced labor costs due to automated material handling, lower maintenance requirements compared to mechanical systems, and improved safety by minimizing manual handling of bulk materials. The systems are particularly useful in underground mining operations where space is limited and dust control is essential. They are also employed in surface mining for transporting ore from processing plants to storage facilities or for transporting raw materials to processing units.
Customization and Engineering Solutions
At Shandong HeadPowder Engineering Co., Ltd., we understand that each mining operation has unique requirements. Our team of engineers works closely with clients to design customized pneumatic conveying systems that meet specific operational needs. This includes selecting the appropriate air pressure, pipeline diameter, and material handling capacity based on the type of ore or powder being transported. We also consider factors such as distance, elevation changes, and environmental regulations to ensure the system operates efficiently and complies with industry standards. Our commitment to quality and innovation ensures that our clients receive reliable and long-lasting solutions that enhance their mining operations.




