Principle and Working Scene Characteristics of Maltose Powder Pneumatic Conveying Line
Release time:2026-09-19 19:01:33
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
HeadPowder, a leading provider of industrial powder handling solutions, specializes in the design and implementation of pneumatic conveying systems tailored for maltose powder applications. This article explores the fundamental principles behind maltose powder pneumatic conveying lines and highlights the key characteristics of their operational environments.
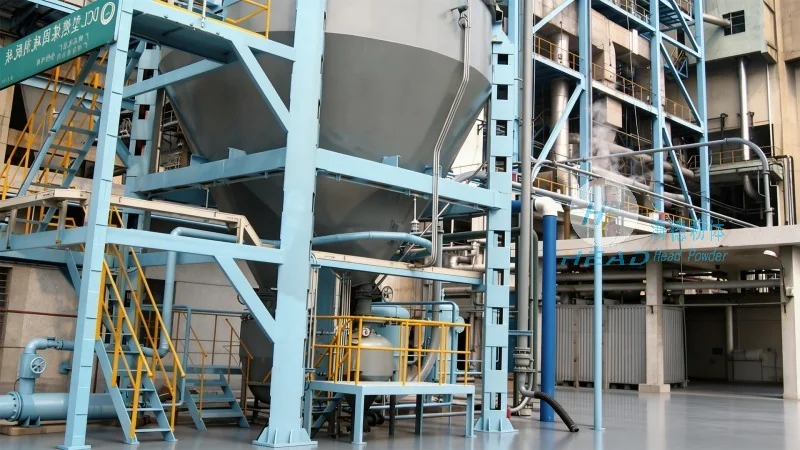
Understanding Pneumatic Conveying Systems for Maltose Powder
Pneumatic conveying lines are a critical component in the processing and transportation of fine powders like maltose. The core principle involves using compressed air to transport the powder material through a pipeline system. This method offers several advantages over traditional mechanical conveying, including reduced contamination risk, lower maintenance requirements, and the ability to handle sensitive or hygienic powders without direct contact with metal or other materials.
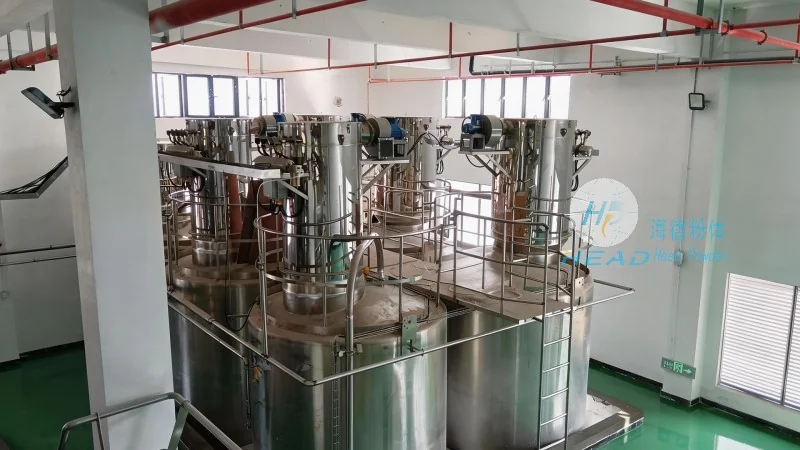
The Working Principle of Maltose Powder Pneumatic Conveying Lines
The operation of a maltose powder pneumatic conveying line typically involves the following steps: first, the maltose powder is fed into a hopper or feeder where it is metered at a controlled rate. Next, compressed air is introduced into the system, creating a flow that propels the powder particles through the pipeline. The system may use either a positive pressure or negative pressure (vacuum) method, depending on the specific application and distance requirements. Positive pressure systems are commonly used for long-distance or high-volume transport, while vacuum systems are ideal for short distances or when the powder needs to be collected from multiple sources.
Key Working Scene Characteristics of Maltose Powder Pneumatic Conveying Lines
The operational environment of maltose powder pneumatic conveying lines is characterized by several factors that influence system design and performance. Firstly, the hygienic requirements of maltose processing often necessitate stainless steel construction and easy-to-clean components to prevent contamination and ensure compliance with food safety regulations. Secondly, the dust control measures are paramount, as maltose is a fine powder that can generate significant airborne dust if not properly managed. The system typically incorporates dust collection and filtration systems to maintain air quality and protect the environment. Thirdly, the system's efficiency and reliability are crucial in continuous production lines, where downtime can impact overall productivity. Therefore, robust control systems and regular maintenance schedules are essential to ensure consistent performance. Additionally, the system's scalability allows it to be adapted for various production scales, from small-scale laboratory applications to large industrial manufacturing facilities.
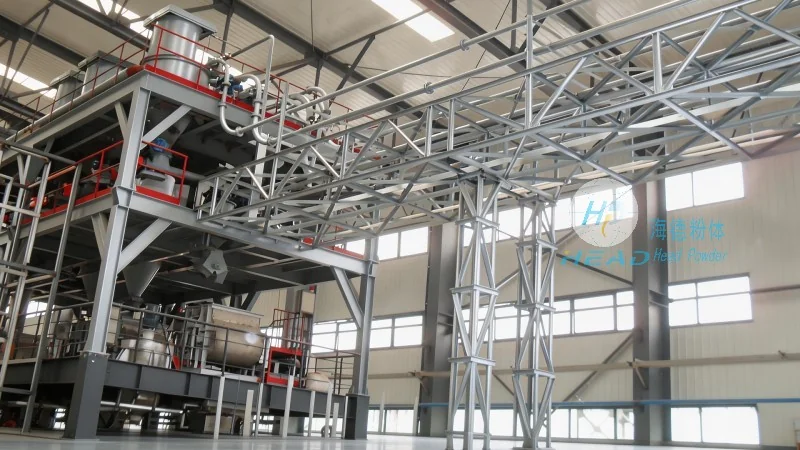
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, with its headquarters in Shandong, China, is dedicated to providing customized pneumatic conveying solutions for the food and pharmaceutical industries. The company's expertise lies in understanding the unique challenges of handling maltose powder and designing systems that meet both operational and regulatory standards. By leveraging advanced engineering and materials, HeadPowder ensures that its pneumatic conveying lines are durable, efficient, and compliant with industry best practices. The company's commitment to quality and customer satisfaction has established it as a trusted partner in the powder handling sector.




