Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer and supplier of powder handling equipment. The company is headquartered in Shandong, China, and specializes in the design, development, and implementation of advanced powder conveying systems, including powder silos and related components. With years of industry experience, headpowder has established itself as a reliable partner for businesses seeking efficient and reliable solutions for powder storage and transportation.
Principle of Powder Silo Powder Conveying
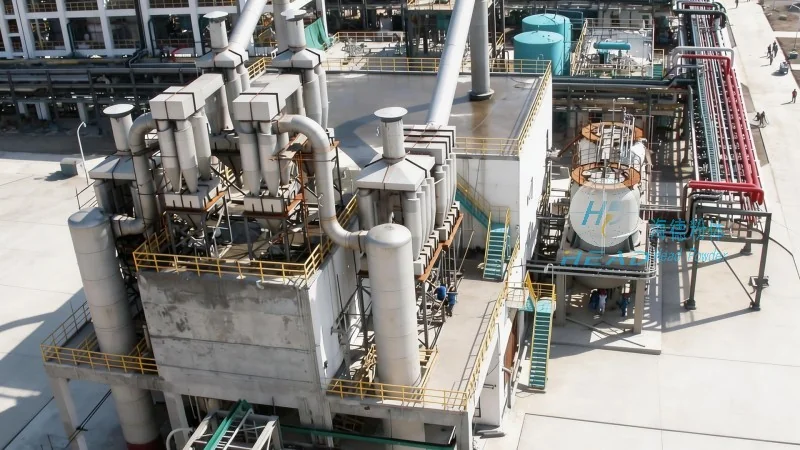
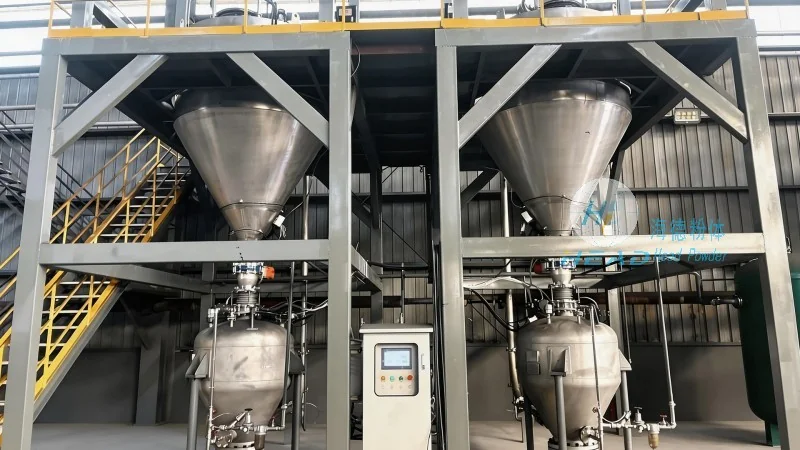
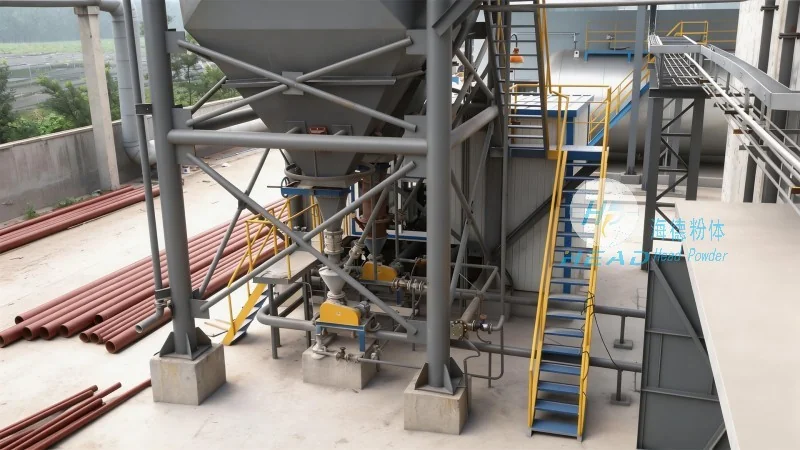
Powder silo powder conveying systems typically operate based on the principle of pneumatic or mechanical transport, depending on the specific application and material characteristics. The core components of such a system include a powder silo, a conveying pipeline, a dust collector, and a control system. The powder silo serves as the primary storage vessel, where bulk powders are stored under controlled conditions to prevent caking or segregation. The conveying process begins when the material is released from the silo, either through a discharge valve or a rotary feeder, and is then transported through the pipeline using air pressure or mechanical force. Pneumatic conveying systems utilize compressed air to create a flow that carries the powder particles, while mechanical systems employ screw conveyors or belt conveyors to move the material. The choice of conveying method depends on factors such as the powder's density, flowability, and moisture content, as well as the required conveying distance and throughput.
Working Scene Characteristics of Powder Silo Powder Conveying
The working scene characteristics of powder silo powder conveying systems vary significantly based on the industry and specific application. In the chemical industry, for example, these systems are commonly used to transport raw materials like powders of pigments, additives, or catalysts to production lines. The systems must be designed to handle materials with varying particle sizes and moisture levels, ensuring consistent quality and preventing contamination. In the food and pharmaceutical industries, the emphasis is on hygiene and safety, with systems often incorporating stainless steel components and advanced filtration to meet regulatory standards. The pharmaceutical sector, in particular, requires strict control over particle size distribution and contamination, making the selection of appropriate conveying equipment critical. In the cement and construction materials industry, large-scale powder silos and high-capacity conveying systems are used to transport bulk materials like cement, fly ash, or limestone to mixing plants or storage facilities. The systems must be robust and capable of handling abrasive materials to ensure long-term durability. Additionally, in the agricultural sector, powder silos are used to store and convey fertilizers or animal feed, where the systems need to be efficient and low-maintenance to support large-scale farming operations. Each application scenario demands tailored solutions to address unique challenges, such as material flowability, environmental regulations, and operational efficiency.




