HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced powder handling solutions. This article explores the fundamental principles of vacuum suction powder conveying systems and highlights key application characteristics that make them ideal for various industrial settings.
Understanding the Principle of Vacuum Suction Powder Conveying
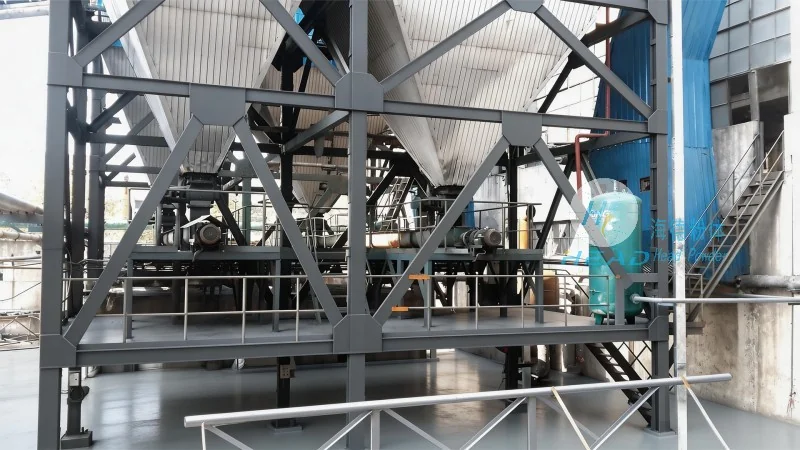
Vacuum suction powder conveying operates on the principle of creating a negative pressure environment within the conveying line. By drawing air and material particles into the system, this method effectively transports powders from the source to the destination. The process typically involves a vacuum pump that generates the necessary suction force, while a hopper or feed device supplies the material. As the material is drawn into the pipeline, it mixes with the air stream, forming a slurry that is then transported through the system. This approach is particularly effective for handling fine or abrasive powders, as it minimizes material degradation and reduces the risk of blockages compared to positive pressure systems.
Key Working Scene Characteristics of Vacuum Suction Systems
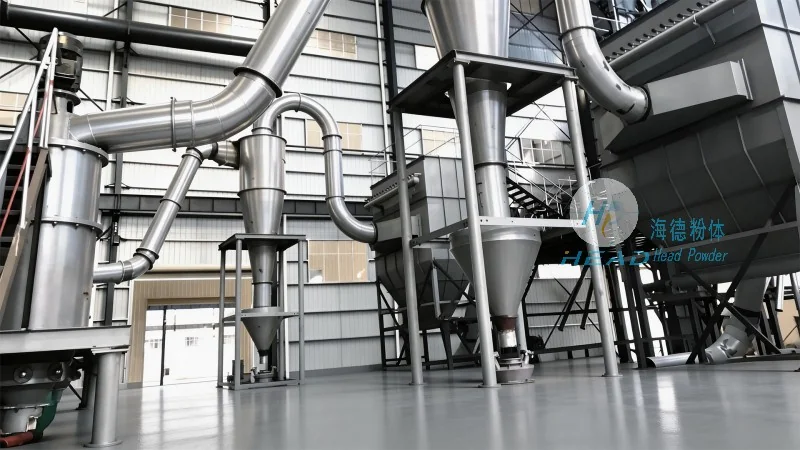
The application characteristics of vacuum suction powder conveying systems are tailored to meet the demands of diverse industrial environments. One of the primary advantages is the ability to handle powders in a closed system, which enhances safety by preventing dust emissions and cross-contamination. This feature is crucial in industries such as pharmaceuticals, food processing, and chemical manufacturing, where product purity and environmental compliance are paramount. Additionally, vacuum suction systems are highly flexible in terms of layout and integration, as they can transport materials over long distances and through complex routes without the need for extensive infrastructure modifications. The system's design allows for easy integration with existing production lines, making it a cost-effective solution for upgrading or expanding powder handling capabilities.
Benefits and Practical Applications
HeadPowder's vacuum suction powder conveying systems offer several benefits that enhance operational efficiency and product quality. The closed-loop design ensures that powders are handled in a controlled environment, reducing the risk of contamination and improving overall product consistency. The system's low maintenance requirements and energy efficiency contribute to long-term cost savings, making it a sustainable choice for industrial operations. In practical applications, these systems are widely used in the pharmaceutical industry for transporting active pharmaceutical ingredients (APIs) and excipients, in the food industry for handling flour, sugar, and other dry ingredients, and in the chemical industry for conveying raw materials and finished products. The ability to handle a wide range of powder types, from fine powders to bulk materials, further expands the system's versatility across different sectors.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, is committed to providing innovative and reliable powder conveying solutions. By leveraging the principles of vacuum suction technology, the company's systems address the unique challenges of modern industrial powder handling, ensuring safety, efficiency, and product integrity. Whether for new installations or system upgrades, HeadPowder's vacuum suction powder conveying systems offer a robust and adaptable solution for businesses seeking to optimize their material handling processes. With a focus on quality and customer satisfaction, HeadPowder continues to be a trusted partner in the development of advanced powder handling technologies.




