HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced pneumatic conveying solutions tailored for handling manganese sulfate materials. This article delves into the working principle and key features of their equipment, offering insights into how such systems efficiently transport this critical industrial chemical.
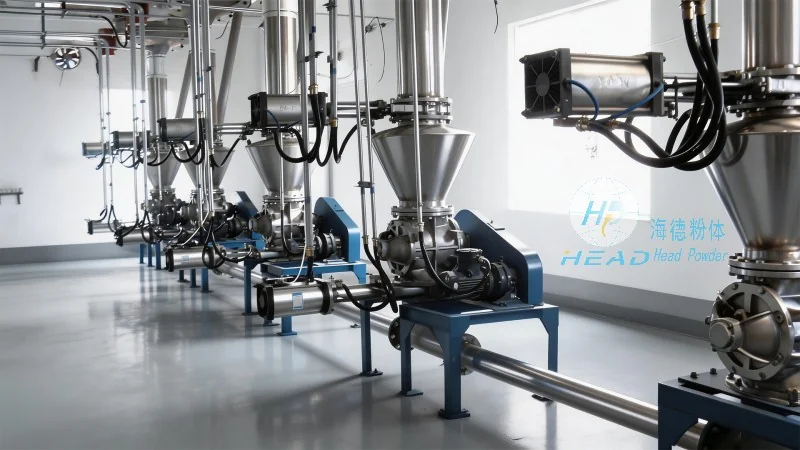
Working Principle of Pneumatic Conveying Equipment for Manganese Sulfate
The pneumatic conveying system for manganese sulfate operates on the fundamental principle of using air as the conveying medium to transport bulk materials. In this setup, the equipment typically employs either positive pressure or negative pressure (or a combination of both) to move the material from the source to the destination. For manganese sulfate, which is often in powder or granular form, the system is designed to handle its specific physical and chemical properties, such as its fine particle size and potential moisture content. The process begins with the material being fed into a hopper or feeder, where it is then introduced into a pipeline. Simultaneously, a fan or blower generates airflow within the pipeline, creating a pressure differential that propels the material forward. The air velocity is carefully controlled to ensure the material remains suspended and moves smoothly without clogging or degradation. The system may include components like cyclones, filters, and receivers to separate the material from the air stream, ensuring efficient collection and minimal loss. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and operational costs while maintaining a high level of efficiency.
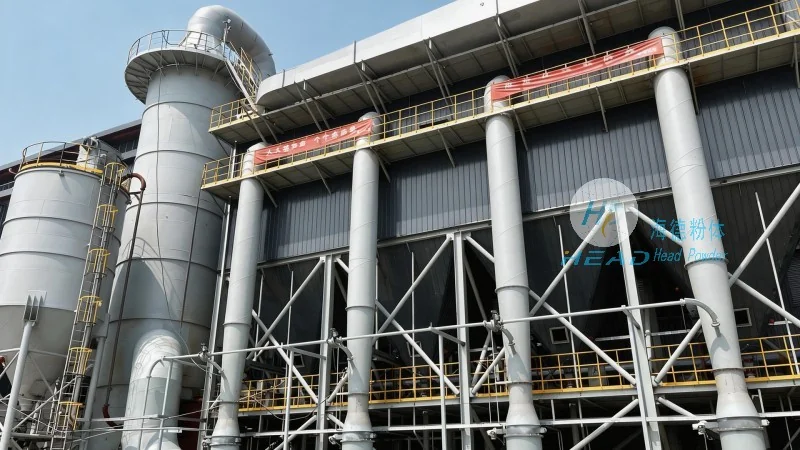
Key Features of the Pneumatic Conveying Equipment
HeadPowder's pneumatic conveying equipment for manganese sulfate is characterized by several distinct features that enhance its performance and suitability for industrial applications. Firstly, the system offers high efficiency in material transport, with the ability to handle large volumes of material over long distances with minimal energy consumption. The design incorporates advanced control systems that allow for precise regulation of air pressure and flow, ensuring consistent and reliable operation. This is particularly important for manganese sulfate, as variations in particle size or moisture can affect flow characteristics, and the equipment's adaptability helps maintain stable performance. Secondly, the equipment is built with durability and longevity in mind, using high-quality materials resistant to corrosion and wear, which is crucial when handling chemical materials like manganese sulfate. The components are designed to withstand the abrasive nature of the material, reducing the frequency of maintenance and extending the service life of the system. Thirdly, the system prioritizes safety and environmental compliance. It incorporates features such as dust suppression and filtration to minimize airborne particulates, adhering to industrial safety standards and reducing the environmental impact. The enclosed design also prevents material spillage and contamination, maintaining a clean and safe working environment. Additionally, the equipment is designed for easy integration into existing production lines, with modular components that can be customized to fit specific plant layouts and operational requirements. This flexibility allows users to adapt the system as their production needs evolve, ensuring long-term value and efficiency.
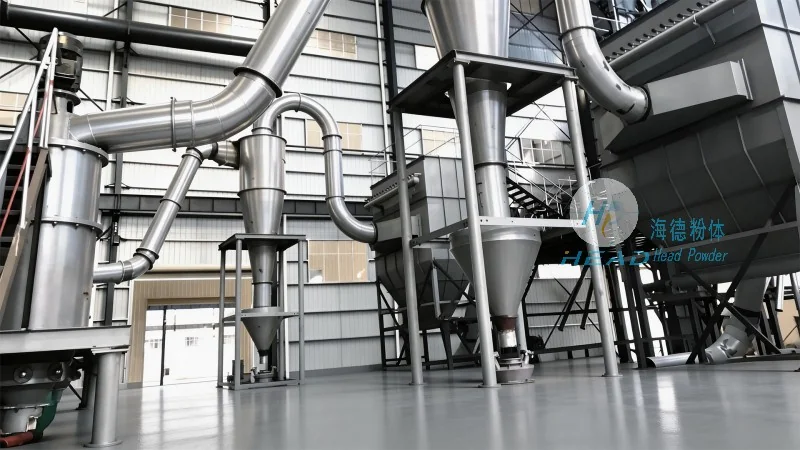
Applications and Benefits in Industrial Settings
The pneumatic conveying equipment for manganese sulfate is widely used in various industrial sectors, including chemical manufacturing, mining, and food processing. In chemical plants, it facilitates the transport of manganese sulfate from storage silos to processing units, ensuring a continuous supply without interruptions. The efficiency of the system reduces downtime and improves overall production throughput. In mining operations, the equipment is used to transport manganese ore or processed manganese compounds, enabling safe and effective handling of bulk materials in challenging environments. The benefits extend to the food industry, where the system can be adapted to handle manganese sulfate used as a food additive, maintaining hygiene and safety standards. The primary advantages of using this equipment include improved operational efficiency, reduced labor costs, and enhanced safety. By eliminating manual handling of bulk materials, the system minimizes the risk of accidents and exposure to dust, while also reducing the physical strain on workers. Furthermore, the enclosed and controlled environment of the pneumatic system prevents cross-contamination and maintains product quality, which is critical in industries where purity and consistency are paramount. Overall, the equipment provides a reliable and cost-effective solution for transporting manganese sulfate, aligning with modern industrial demands for efficiency, safety, and sustainability.




