For industries dealing with copper sulfate, efficient and reliable powder handling is crucial. This article explores the working principles and key features of specialized equipment designed for this purpose, ensuring optimal performance and safety in material processing. The equipment is tailored to meet the unique demands of copper sulfate applications, which often involve handling fine powders that require precise control to prevent issues like caking or segregation.
Working Principle of Copper Sulfate Powder Handling Equipment
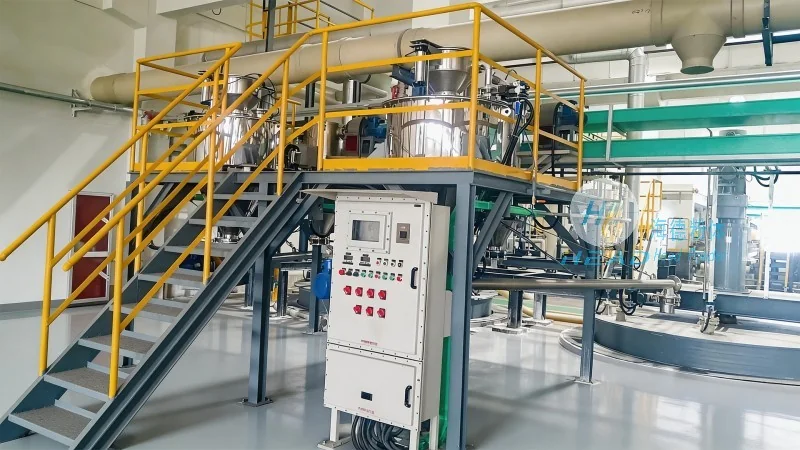
The core of copper sulfate powder handling equipment lies in its ability to transport and manage the material from storage to processing or packaging stages. Typically, these systems incorporate components such as hoppers, feeders, conveyors, and control mechanisms. The working principle involves several key steps: first, the powder is stored in a hopper, where it is held under controlled conditions to prevent moisture absorption or degradation. Next, a feeder regulates the flow of the powder into the conveyor system, ensuring a consistent and controlled discharge rate. The conveyor then transports the powder to the next stage, such as a mixer, reactor, or packaging unit. Advanced systems may include sensors and automation to monitor flow rates, pressure, and other parameters, providing real-time feedback to maintain optimal operation. This integrated approach ensures that the copper sulfate powder is handled with minimal loss, contamination, or degradation, maintaining its quality throughout the process.
Key Features of Copper Sulfate Powder Handling Equipment
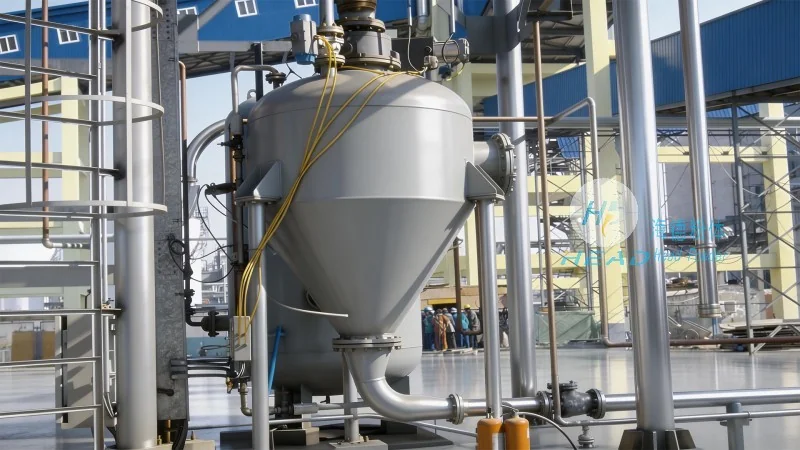
Specialized copper sulfate powder handling equipment is designed with several features that enhance performance and safety. One of the primary features is the use of dust-proof and explosion-proof designs, which are essential for handling powders that may be prone to dust accumulation and potential ignition risks. The equipment often incorporates sealed systems and proper ventilation to minimize dust exposure and ensure compliance with safety regulations. Another critical feature is the ability to handle fine powders without caking or segregation. This is achieved through the use of agitators or vibrators in hoppers and feeders, which keep the powder in a free-flowing state. Additionally, the equipment may include temperature control mechanisms to prevent moisture absorption, as copper sulfate can absorb moisture from the air, leading to clumping and reduced effectiveness. The design also prioritizes ease of maintenance, with accessible components and quick-release mechanisms for cleaning and replacement of parts. These features collectively ensure that the equipment operates efficiently, safely, and reliably, meeting the demands of industrial applications.
Application Scenarios and Benefits
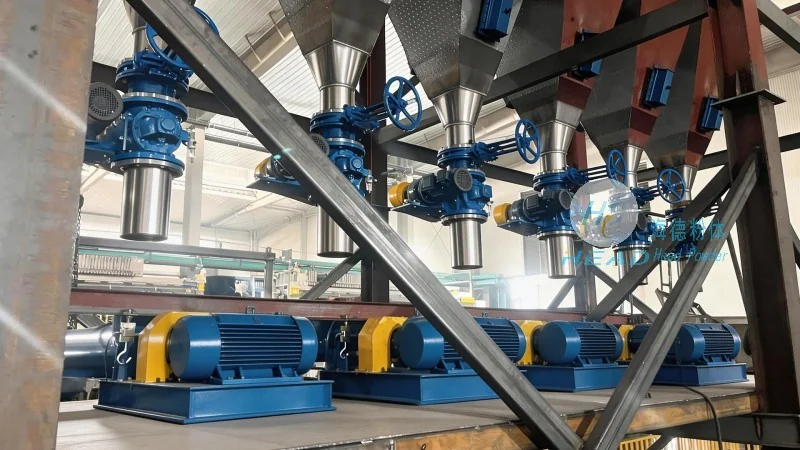
Copper sulfate powder handling equipment is widely used in various industries, including agriculture, water treatment, and chemical manufacturing. In agriculture, it is used as a fungicide and algaecide, and the equipment ensures that the powder is applied uniformly and safely. In water treatment, copper sulfate is used to control algae growth, and the equipment helps in precise dosing and distribution. The benefits of using specialized handling equipment include improved product quality, reduced waste, and enhanced safety for operators. By maintaining the powder in a dry and free-flowing state, the equipment prevents caking, which can lead to blockages and reduced efficiency. The consistent flow rates also ensure that the copper sulfate is applied at the correct concentration, optimizing the effectiveness of the product. Furthermore, the automation and control features reduce the risk of human error, leading to more reliable and repeatable results. The equipment also contributes to environmental safety by minimizing dust emissions and preventing accidental spills, which can be harmful to both personnel and the environment.
Customization and Integration with Existing Systems
Shandong HeadPowder Engineering Co., Ltd. offers customized solutions for copper sulfate powder handling equipment, tailored to the specific needs of each client. The company, known as headpowder, provides a range of options from standard models to fully customized systems that integrate seamlessly with existing production lines. Customization may include adjustments to hopper size, conveyor capacity, and control systems to match the client's production volume and process requirements. The equipment can also be integrated with other machinery, such as mixers, reactors, or packaging units, to create a comprehensive material handling system. This integration ensures that the copper sulfate powder is processed efficiently from storage to final use, minimizing downtime and maximizing productivity. The company's expertise in powder handling technology allows them to address unique challenges, such as handling powders with high moisture content or those that are prone to agglomeration. By working closely with clients, headpowder develops solutions that meet both current and future needs, ensuring long-term reliability and performance.
Maintenance and Longevity of the Equipment
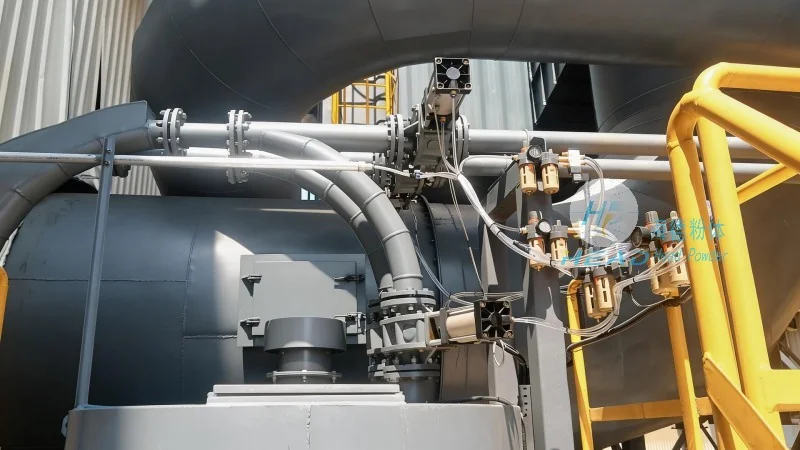
Proper maintenance is essential to ensure the longevity and optimal performance of copper sulfate powder handling equipment. Regular maintenance tasks include cleaning the hopper and feeder to prevent powder buildup, checking the condition of seals and bearings, and inspecting the conveyor system for wear and tear. The equipment is designed with durable materials, such as stainless steel, to withstand the corrosive nature of copper sulfate and prevent rust or degradation over time. Headpowder provides maintenance services and spare parts to support their clients, ensuring that the equipment remains in good working condition. By following the manufacturer's guidelines for maintenance, users can extend the lifespan of the equipment and avoid costly repairs or replacements. The company also offers training to operators on how to properly operate and maintain the equipment, enhancing safety and efficiency. This proactive approach to maintenance helps in reducing downtime and maintaining consistent performance, which is critical for industries that rely on reliable powder handling systems.




