

Working Principle and Features of Borax Pneumatic Conveying Systems
Understanding the operational mechanics and key attributes of borax pneumatic conveying systems is crucial for industries relying on efficient material handling. This article delves into the core principles behind these systems and highlights their distinct advantages, providing insights into how they enhance process efficiency and safety.
Working Principle of Borax Pneumatic Conveying Systems
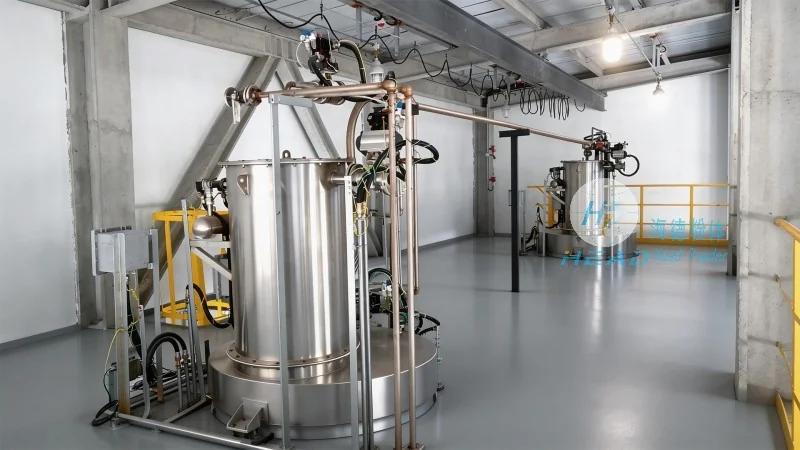
Borax pneumatic conveying systems utilize air as the primary medium to transport borax particles from one location to another. The fundamental mechanism involves creating a pressure differential between the conveying line and the surrounding environment. In a typical setup, a blower or compressor generates high-pressure air that is introduced into the system. As the air flows through the pipeline, it draws borax particles into the stream, forming a dense mixture known as a "slurry" or "conveying stream." The system can operate under either positive pressure (where the air pressure is higher than ambient) or negative pressure (where the air pressure is lower than ambient). Positive pressure systems are often preferred for long-distance or multi-point delivery, as they can maintain consistent flow rates and prevent dust ingress. Negative pressure systems, on the other hand, are suitable for applications requiring dust containment and are commonly used in environments where air quality must be preserved.
Key Features and Advantages of Borax Pneumatic Conveying Systems
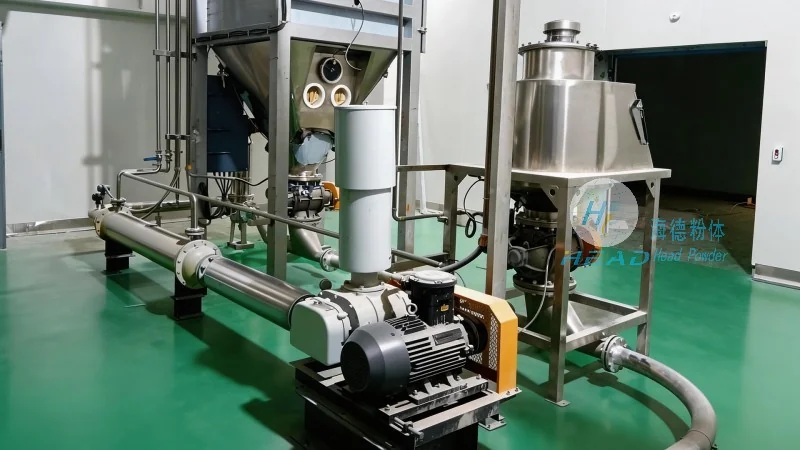
The borax pneumatic conveying systems offered by Shandong HeadPowder Engineering Co., Ltd. (commonly known as headpowder) are designed to deliver superior performance and reliability. These systems are engineered to handle the unique properties of borax, such as its fine particle size and hygroscopic nature, ensuring minimal degradation during transport. One of the standout features is the high efficiency in material transfer, with the ability to move large volumes of borax over considerable distances with minimal energy consumption. The systems are also equipped with advanced control mechanisms that allow for precise regulation of air flow and pressure, enabling operators to optimize the conveying process based on specific requirements. Additionally, the design incorporates robust filtration and separation components to prevent particle buildup and maintain system cleanliness, reducing maintenance downtime and operational costs. Safety is a paramount consideration in these systems, with features like explosion-proof blowers and dust collection units that mitigate risks associated with handling powders. The systems are compliant with industry standards for material handling, ensuring adherence to safety and environmental regulations.
Customization and Application Flexibility
headpowder recognizes that borax processing facilities have diverse operational needs. Therefore, their pneumatic conveying systems are highly customizable to meet specific application requirements. Whether the application involves short-distance transport within a plant or long-distance delivery to a storage facility, the systems can be tailored to accommodate varying particle sizes, flow rates, and system configurations. The company's engineering team works closely with clients to assess their unique processes and design solutions that maximize efficiency while minimizing operational challenges. This approach ensures that the borax pneumatic conveying systems are not only effective but also scalable, allowing businesses to adapt to changing production demands over time. The flexibility in system design also extends to integration with existing infrastructure, reducing the need for extensive modifications and lowering the overall project cost.
Operational Benefits and Cost Efficiency
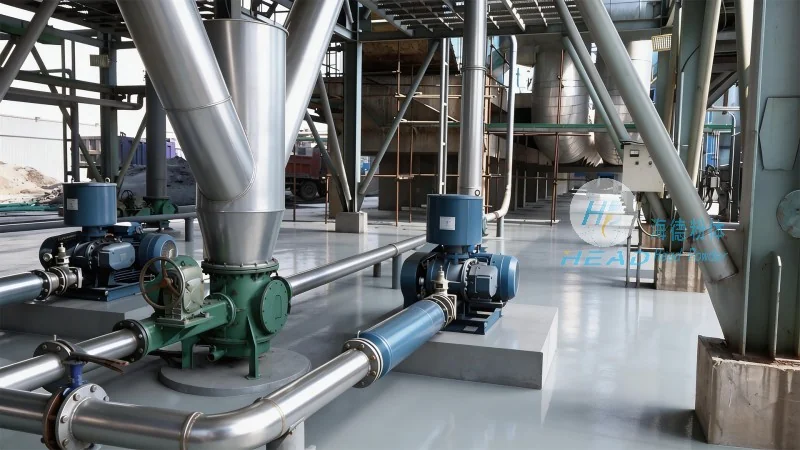
Implementing borax pneumatic conveying systems brings numerous operational benefits that contribute to overall cost savings and process optimization. By eliminating the need for traditional bulk handling methods, such as bucket elevators or belt conveyors, the systems reduce labor costs and minimize the risk of material spillage or contamination. The automated nature of the process ensures consistent and reliable material transfer, which is critical for maintaining production schedules and product quality. Furthermore, the reduced reliance on manual handling improves workplace safety by minimizing exposure to dust and other hazards associated with handling fine powders. The energy efficiency of these systems, particularly in positive pressure configurations, results in lower operational expenses over the long term. The initial investment in a borax pneumatic conveying system is often offset by the savings in labor, maintenance, and energy costs, making it a financially viable solution for borax processing operations.