Coffee bean material handling systems are essential components in the coffee processing industry, designed to efficiently transport coffee beans from one stage of production to another. These systems play a crucial role in ensuring the smooth operation of coffee processing facilities, from raw bean reception to final packaging. Understanding the design principles behind these systems is vital for optimizing workflow, maintaining product quality, and enhancing overall operational efficiency.
Understanding Coffee Bean Material Handling Systems
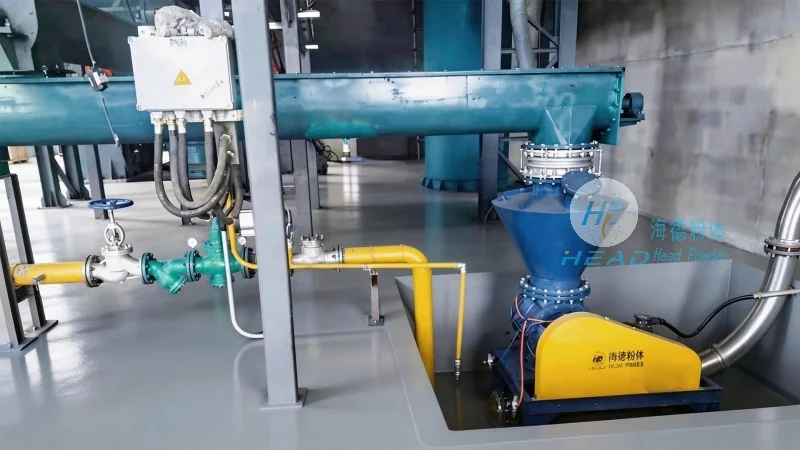
A coffee bean material handling system encompasses a range of equipment and mechanisms used to move coffee beans through various processing stages. This includes receiving, cleaning, sorting, roasting, and packaging. The system's design must consider factors such as bean size, moisture content, and the specific requirements of each processing step to ensure optimal performance. For instance, during the reception phase, the system may involve bulk handling equipment like conveyors or elevators to move large quantities of raw coffee beans from storage silos or trucks into processing areas. Cleaning equipment, such as air classifiers or magnetic separators, may be integrated to remove impurities like stones, dust, or metal fragments, which could compromise the quality of the final product.
Key Design Principles for Efficient Material Handling
The design of a coffee bean material handling system is guided by several fundamental principles aimed at maximizing efficiency and minimizing downtime. One of the primary principles is the concept of continuous flow, where beans move through the system in a seamless, unbroken process. This reduces the need for manual intervention and minimizes the risk of product contamination or loss. Another critical principle is the use of standardized equipment that can handle various bean types and sizes, providing flexibility in processing different coffee varieties. Additionally, the system should be designed for easy maintenance and cleaning, as coffee beans can adhere to equipment surfaces and require regular sanitation to prevent mold or bacterial growth.
Components of a Typical Coffee Bean Material Handling System
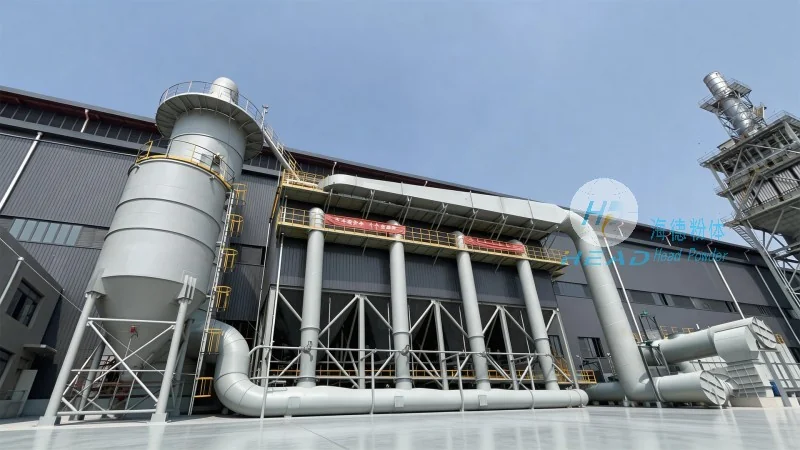
A comprehensive coffee bean material handling system typically includes several key components, each serving a specific function in the overall workflow. The first component is often a receiving and storage system, which may include silos or bulk storage tanks to hold large quantities of raw coffee beans. From there, the beans are transferred to a cleaning and sorting unit, where air classifiers separate lighter impurities from heavier beans, and magnetic separators remove metal contaminants. The cleaned beans then move to a roasting section, where they are roasted to the desired level of doneness. After roasting, the beans are cooled and may undergo a final sorting or grading process to ensure uniform quality. Finally, the processed beans are packaged and prepared for distribution.
HeadPowder Engineering: Experts in Coffee Bean Processing Solutions
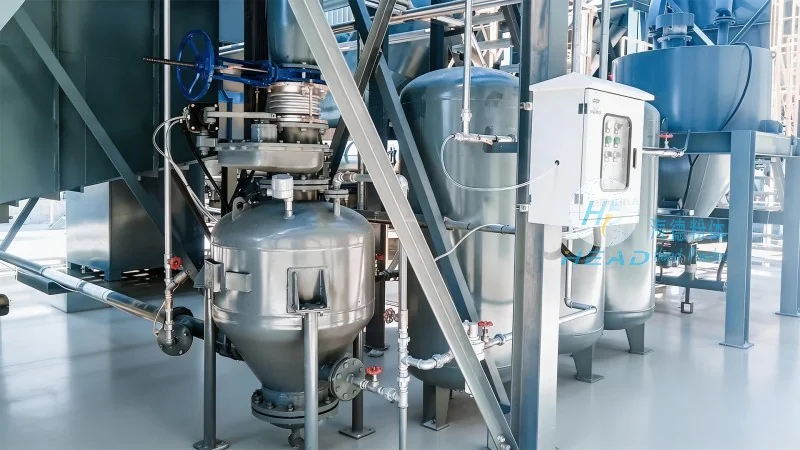
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the coffee processing equipment industry, specializes in designing and manufacturing high-quality coffee bean material handling systems. With years of experience and a deep understanding of the coffee industry's unique requirements, HeadPowder provides customized solutions tailored to the specific needs of coffee producers. The company's products are engineered to meet the highest standards of efficiency, durability, and reliability, ensuring that coffee beans are handled with care from reception to packaging. HeadPowder's commitment to quality and innovation has made it a trusted partner for coffee processing facilities worldwide.
Conclusion: The Importance of Well-Designed Material Handling Systems
In conclusion, coffee bean material handling systems are indispensable in modern coffee processing operations. Their design principles, which prioritize continuous flow, flexibility, and ease of maintenance, are crucial for maintaining product quality and operational efficiency. By investing in a well-designed material handling system, coffee producers can streamline their production processes, reduce costs, and enhance the overall quality of their final products. As the coffee industry continues to grow, the importance of efficient material handling systems will only increase, making them a critical component of any successful coffee processing facility.




