When it comes to handling bulk powder materials, the tonne bag automatic feeding powder conveyor is a critical piece of equipment in industrial processes. This system is specifically designed to efficiently and safely transfer powder from large bulk bags (tonne bags) into subsequent processing stages, streamlining operations and enhancing productivity. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, specializes in developing advanced powder handling solutions tailored to meet the demands of various industries.
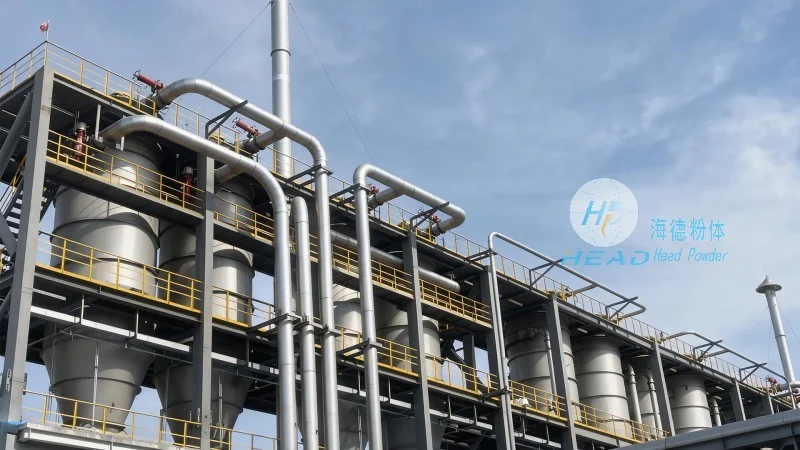
What is a Tonne Bag Automatic Feeding Powder Conveyor?
A tonne bag automatic feeding powder conveyor, also known as a bulk bag unloader or bulk bag feeder, is an automated system engineered to handle the unloading and feeding of powder materials from tonne bags. These large, flexible containers are commonly used for transporting bulk powders, and the conveyor system simplifies the process by eliminating the need for manual labor to open, empty, and transfer the contents. The system typically integrates several key components, including a bag support frame, an opening mechanism (such as a bag opener or tarpaulin removal system), a discharge valve or spout, and a material handling unit (like a screw conveyor or pneumatic conveyor) that transports the powder to the next stage of production.
Design Principles of the Tonne Bag Automatic Feeding Powder Conveyor
The design of a tonne bag automatic feeding powder conveyor is centered on efficiency, safety, and automation. Several key principles guide the engineering and operation of this equipment:
1. **Automated Bag Handling**: The system is designed to handle the entire process of bag opening, emptying, and closure without manual intervention. This includes mechanisms such as bag lifting, tarpaulin removal, and discharge valve operation, which are controlled by a programmable logic controller (PLC) or other automation systems. This automation reduces labor costs and minimizes the risk of human error.
2. **Material Transfer Efficiency**: The conveyor system is engineered to maximize the transfer rate of powder from the tonne bag to the downstream process. This is achieved through the selection of appropriate material handling components, such as screw conveyors or pneumatic conveying systems, which are optimized for the specific properties of the powder (e.g., flowability, moisture content, and particle size). The design ensures minimal material loss and consistent flow rates.
3. **Safety and Environmental Considerations**: The design incorporates safety features to protect operators and the environment. For example, dust collection systems are integrated to capture airborne particles, preventing contamination and ensuring compliance with environmental regulations. Additionally, the system may include safety interlocks to prevent operation when the bag is not properly positioned or when the discharge valve is open.
4. **Modular and Scalable Design**: The conveyor is often designed as a modular system, allowing for easy integration with existing production lines and scalability to accommodate varying production volumes. This flexibility enables manufacturers to adapt the system to changing production needs without significant modifications.
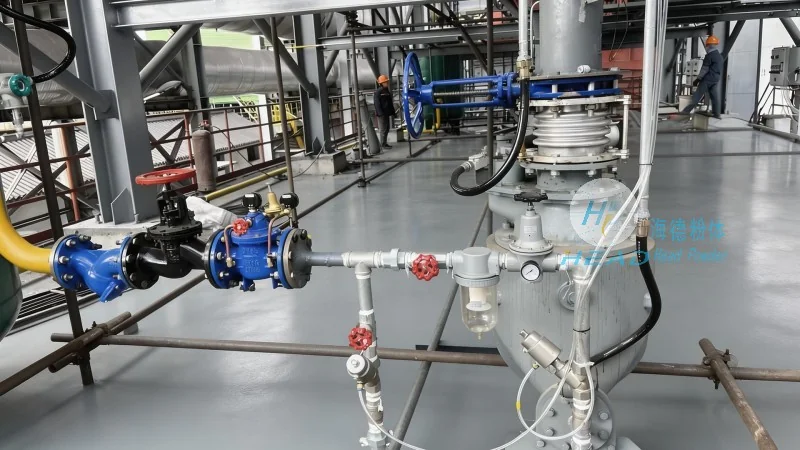
Key Components and Their Functions
The tonne bag automatic feeding powder conveyor consists of several interconnected components, each playing a vital role in the overall operation:
1. **Bag Support and Lifting Frame**: This component holds the tonne bag in place and elevates it to the correct height for unloading. It typically includes a frame with adjustable supports to accommodate different bag sizes and weights.
2. **Bag Opener or Tarpaulin Removal System**: This mechanism is responsible for opening the top of the tonne bag. Common methods include mechanical cutting of the bag top, or the use of a tarpaulin removal system that pulls the cover off the bag, exposing the powder inside.
3. **Discharge Valve or Spout**: Once the bag is opened, the discharge valve or spout allows the powder to flow out into the conveyor system. This component is often designed to be adjustable to control the flow rate and prevent overloading the downstream equipment.
4. **Material Handling Unit (e.g., Screw Conveyor or Pneumatic Conveyor)**: This is the core of the material transfer process. A screw conveyor uses rotating screws to push the powder forward, while a pneumatic conveyor uses air pressure to transport the powder through a pipeline. The choice of unit depends on the powder's characteristics and the distance to the next processing stage.
5. **Control System**: The entire operation is managed by a control system, usually a PLC, which coordinates the actions of all components. The system can be programmed to follow a specific sequence, such as lifting the bag, opening it, starting the conveyor, and then closing the bag once empty.
Applications and Benefits
The tonne bag automatic feeding powder conveyor is widely used in industries that handle bulk powders, including food processing, pharmaceuticals, chemicals, and mining. Its benefits include:
1. **Increased Productivity**: By automating the unloading process, the system reduces downtime and increases the throughput of powder materials, allowing for higher production rates.
2. **Improved Safety**: Manual handling of tonne bags is hazardous, and the automated system eliminates the need for workers to be in close proximity to the bags during unloading, reducing the risk of injuries.
3. **Consistent Quality**: The system ensures a consistent flow rate and particle size distribution, which is crucial for maintaining product quality in sensitive applications like pharmaceuticals or food production.
4. **Reduced Labor Costs**: Automation minimizes the need for manual labor, lowering operational costs and freeing up human resources for other tasks.
5. **Environmental Compliance**: The integrated dust collection systems help maintain a clean working environment and comply with environmental regulations regarding dust emissions.




