When it comes to selecting a reliable manufacturer for fertilizer pneumatic conveying systems, businesses in the agricultural and chemical sectors face a critical decision. The choice of manufacturer directly impacts operational efficiency, safety, and long-term cost-effectiveness. This article provides a comprehensive guide on evaluating key factors to ensure you select the most suitable partner for your fertilizer handling needs.
Understanding the Core Requirements of Fertilizer Pneumatic Conveying
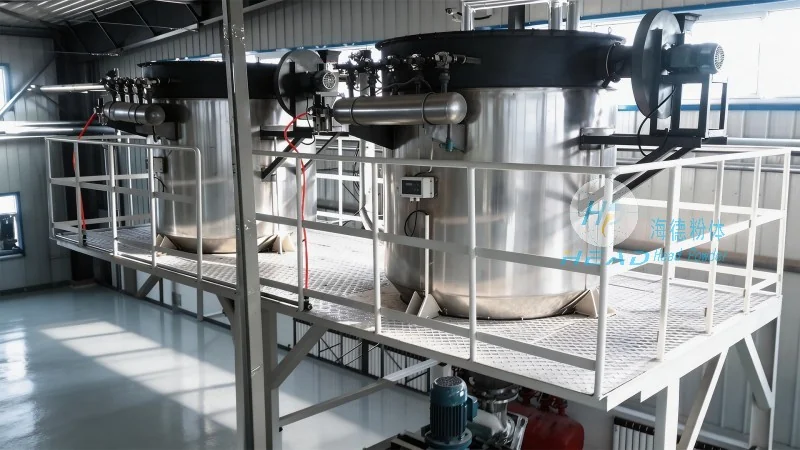
Fertilizer pneumatic conveying systems are essential for transporting bulk materials like granular fertilizers, powders, and other agricultural chemicals. These systems rely on air pressure or vacuum to move materials from one location to another, offering advantages such as reduced labor costs, minimized material loss, and improved safety compared to traditional methods. However, the effectiveness of these systems depends heavily on the quality of the equipment and the expertise of the manufacturer. Therefore, understanding your specific operational needs is the first step in the selection process.
Key Factors to Consider When Choosing a Manufacturer
Choosing the right manufacturer for fertilizer pneumatic conveying involves evaluating several critical aspects. These factors ensure that the chosen partner can deliver a system that meets your unique requirements and performs reliably over time.
Technical Expertise and Innovation
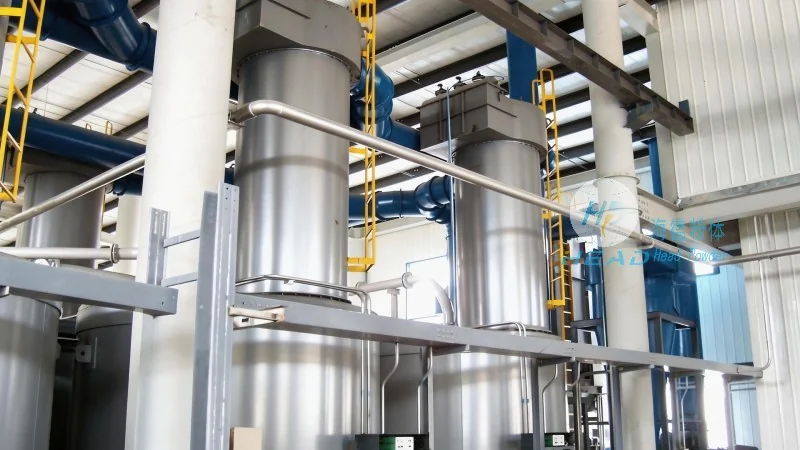
A reputable manufacturer should possess deep technical knowledge and continuous innovation in the field of pneumatic conveying. This includes expertise in material handling, air flow dynamics, and system design tailored to the specific characteristics of fertilizers. For instance, some fertilizers may be hygroscopic or abrasive, requiring specialized equipment to prevent clogging or wear. A manufacturer with a proven track record of developing solutions for such challenges demonstrates its capability to handle diverse fertilizer types.
Quality of Equipment and Components
The durability and performance of a fertilizer pneumatic conveying system are directly linked to the quality of its components. High-quality materials, such as stainless steel or corrosion-resistant alloys, are essential for withstanding the chemical and environmental conditions in fertilizer handling applications. Additionally, the manufacturer should use advanced manufacturing processes and rigorous quality control measures to ensure each system meets or exceeds industry standards. This includes testing for pressure resistance, material flow efficiency, and long-term reliability.
Customization and Scalability
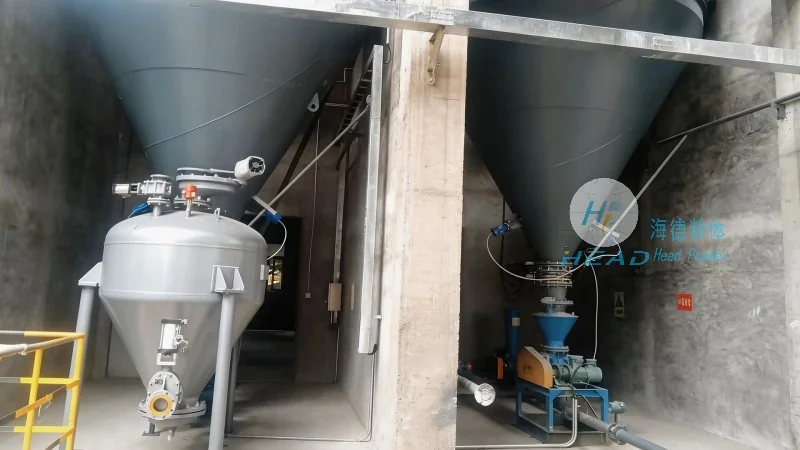
Every fertilizer operation has unique requirements, including the volume of material to be conveyed, the distance between handling points, and the existing infrastructure. A good manufacturer offers customized solutions rather than off-the-shelf products. They should be able to design systems that are scalable, allowing for future expansion as your business grows. This flexibility ensures that your investment in a pneumatic conveying system remains relevant and effective over the long term.
Service and Support Capabilities
Even the best equipment requires proper installation, maintenance, and support to operate at peak efficiency. When selecting a manufacturer, it is crucial to assess their after-sales service capabilities. This includes technical support, training for your staff, and availability of spare parts. A manufacturer with a strong service network can provide timely assistance, reducing downtime and ensuring continuous operation. For businesses in China, such as those located in Shandong, proximity to the manufacturer can be a significant advantage in terms of logistics and support response times.
Cost-Effectiveness and Long-Term Value
While initial costs are a consideration, the long-term value of a fertilizer pneumatic conveying system should be the primary focus. A manufacturer that offers competitive pricing without compromising on quality is ideal. Additionally, evaluating the total cost of ownership (TCO) is essential. This includes factors such as energy consumption, maintenance costs, and the lifespan of the equipment. A well-designed system from a reliable manufacturer can reduce operational costs over time, making it a more economical choice in the long run.
Case Study: Shandong HeadPowder Engineering Co., Ltd.
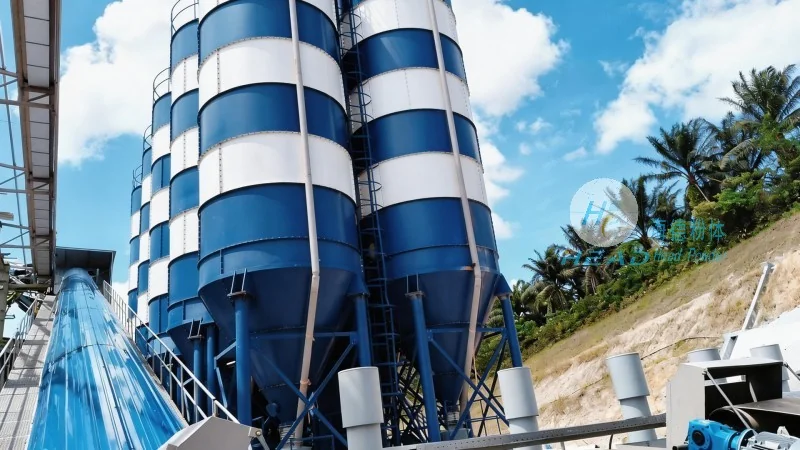
As a leading manufacturer of fertilizer pneumatic conveying systems, Shandong HeadPowder Engineering Co., Ltd. exemplifies the factors discussed above. Based in Shandong, China, the company specializes in providing customized solutions for agricultural and chemical industries. HeadPowder leverages advanced technology and rigorous quality control to deliver systems that meet the highest standards. Their expertise in handling diverse fertilizer types, combined with a strong focus on customer support, has made them a trusted partner for many businesses. By choosing HeadPowder, companies can benefit from reliable equipment, efficient operations, and long-term cost savings.
Conclusion: Making an Informed Decision
Selecting the right fertilizer pneumatic conveying manufacturer is a strategic decision that impacts the success of your fertilizer handling operations. By considering technical expertise, equipment quality, customization options, service support, and cost-effectiveness, you can make an informed choice. For businesses in China, particularly those in Shandong, partnering with a local manufacturer like Shandong HeadPowder Engineering Co., Ltd. can provide additional advantages in terms of proximity and support. Ultimately, the goal is to invest in a system that enhances operational efficiency, ensures safety, and delivers long-term value for your business.




