

What is a PFA Pneumatic Conveying Equipment? Introduction to the Structure and Principle of Powder H
For industrial applications requiring the efficient and reliable transport of powder materials, specialized equipment is essential. Among the advanced solutions available, the PFA (Polytetrafluoroethylene-co-hexafluoropropylene) pneumatic conveying system stands out due to its exceptional chemical resistance, thermal stability, and durability. This article provides a comprehensive overview of what a PFA pneumatic conveying equipment is, detailing its structural components and the underlying principles that enable effective powder handling.
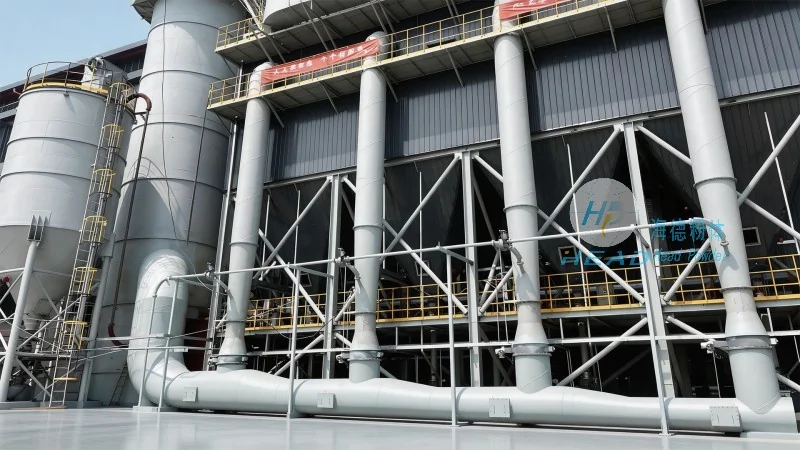
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of powder handling technology, specializes in designing and manufacturing high-quality pneumatic conveying systems. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner for industries such as pharmaceuticals, food processing, and chemical manufacturing. HeadPowder's expertise lies in developing customized solutions that meet the unique requirements of each client, ensuring optimal performance and longevity of the equipment.
Key Structural Components of PFA Pneumatic Conveying Equipment
The PFA pneumatic conveying system is composed of several critical components that work in tandem to achieve efficient powder transport. The primary elements include: (1) a high-pressure air source, typically an air compressor, which generates the necessary airflow to move the powder particles; (2) a feed hopper or inlet, where the powder is introduced into the system; (3) a conveying line, often made from PFA or other corrosion-resistant materials, to transport the powder from the inlet to the discharge point; (4) a separation or collection unit, such as a cyclone or filter, which separates the powder from the air stream; and (5) a control system, which regulates the airflow and pressure to maintain optimal operation.
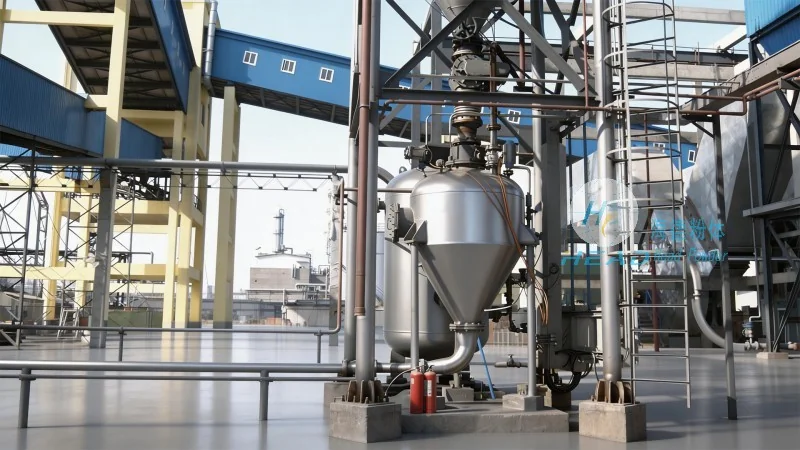
Operational Principle: How PFA Pneumatic Conveying Works
The core principle of pneumatic conveying is the use of compressed air to create a flow that transports the powder particles. In the PFA system, the air is introduced into the conveying line at a high velocity, creating a "slug" or "stream" of air that pulls the powder particles along. The PFA material of the conveying line is chosen for its resistance to chemical corrosion and high temperatures, ensuring that the system can handle a wide range of powder types without degradation. The separation unit then captures the powder, allowing the clean air to be recirculated or vented, depending on the application.
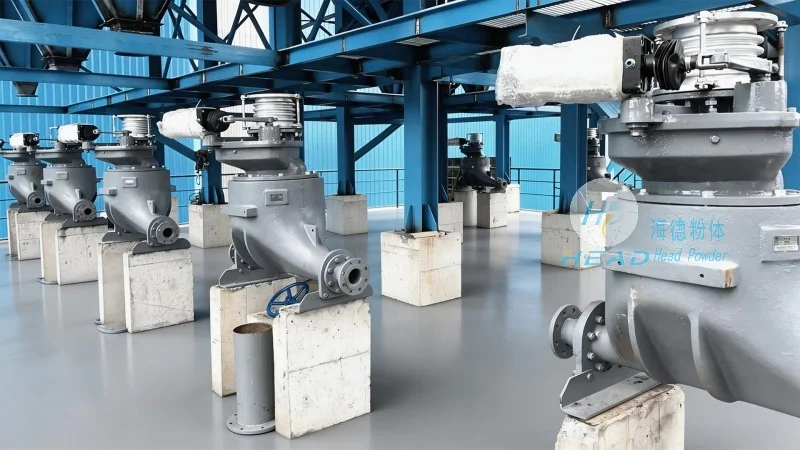
Advantages of PFA Pneumatic Conveying Equipment
Compared to traditional mechanical conveying methods, PFA pneumatic conveying offers several advantages. Firstly, it eliminates the need for moving parts, reducing maintenance requirements and increasing reliability. Secondly, the system can handle a wide variety of powder characteristics, including fine powders, bulk powders, and those with high moisture content. Thirdly, the PFA material provides excellent chemical resistance, making it suitable for transporting corrosive or abrasive powders. Additionally, the system is compact and can be easily integrated into existing production lines, minimizing space requirements.
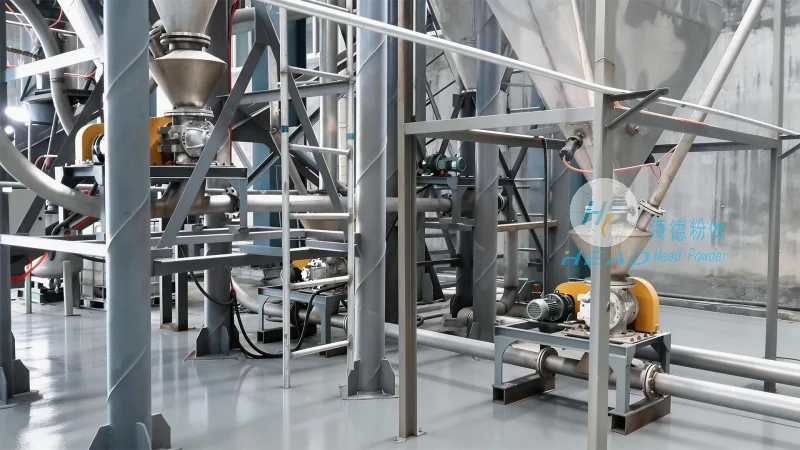
Applications and Industries Served
PFA pneumatic conveying equipment is widely used across various industries due to its versatility and efficiency. In the pharmaceutical industry, it is used for the transport of active pharmaceutical ingredients (APIs) and excipients, ensuring that the powders remain sterile and free from contamination. In the food processing sector, it handles powders such as sugar, flour, and spices, maintaining product quality and hygiene. The chemical industry utilizes the system for transporting corrosive chemicals and catalysts, while the manufacturing sector employs it for bulk material handling in production lines.
Conclusion: The Role of PFA Pneumatic Conveying in Modern Powder Handling
As industries continue to demand higher efficiency and reliability in powder handling, PFA pneumatic conveying equipment remains a critical solution. By leveraging advanced materials and operational principles, this technology ensures that powder materials are transported safely, efficiently, and with minimal loss or contamination. With its robust design and adaptability, the PFA pneumatic conveying system continues to be a preferred choice for businesses seeking to optimize their material handling processes.